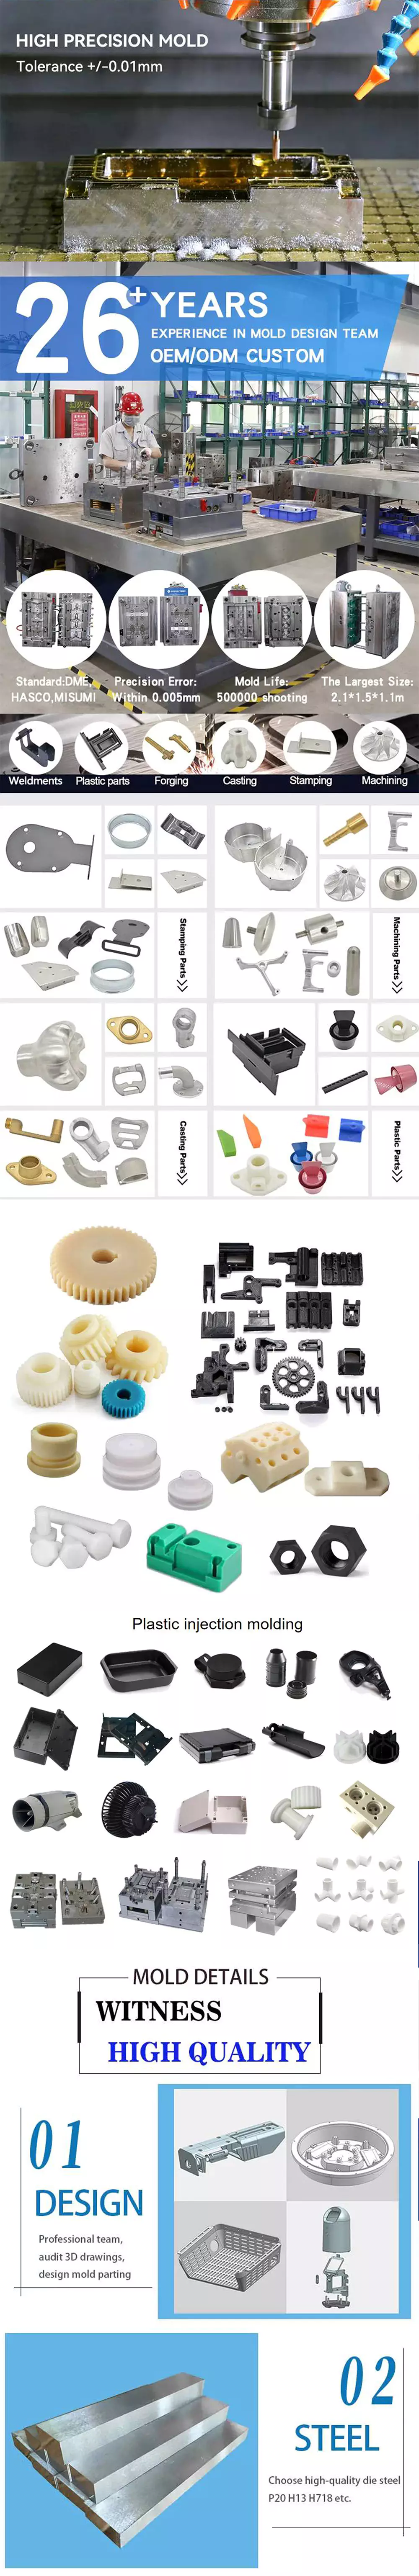
China Custom Wholesale High Precision ABS Plastic Injection Molded Parts Plastic Cryogenic Box injection moulding of parts
Solution Description
Customized Wholesale Large Precision Ab muscles Plastic Injection Molded Areas Plastic Cryogenic Box
Benefits:
one. Free of charge style and free of charge sample.
two. Indicator NDA.
3. ISO Certificated with the rigorous top quality management program.
4. thirteen Years OEM&ODM Mould-making,metal and plastic processing knowledge.
5. Excellent at spoken english and phone get in touch with interaction.
6.1 cease resolution and fall shipment for on the web sellers.
Product Description
| Solution Description |
ODM plastic injection molding |
| Plastic Supplies: |
PS, Abs, PP, PVC, PMMA, PBT, Pc, POM, PA66, PA6, PBT+GF, Pc/Stomach muscles, PEEK, HDPE, TPU, PET, PPO,…and so forth. |
| Standard: |
ISO9001:2008 |
| High quality: |
RoSH and SGS regular |
| Feature: |
Non marking and Non flash |
| Dimensions: |
In accordance to your Second, 3D Drawing |
| Colour,Quantity,Device cost,Tooling price,Tooling measurement: |
To be discussed |
| Package: |
Standard exported Wood box packed, Fumigation method(on essential) |
| Mold Constructing Direct Time: |
T1, 15-25 Operating times, Portion measurement report (on necessary). |
| Export Region: |
All nations are reachable. |
| Knowledge: |
13 many years knowledge in plastic injection mildew generating and plastic prouducts create. |
| Mould Base: |
Hasco Normal, European Normal, Planet Common |
| Mould Foundation Content: |
LKM, FUTA, HASCO, DME,…and so forth. Or as for every Customer’s Requirment. |
| Area End: |
Texture(MT standard), Substantial gloss polishing |
| Cavity/Core Steel: |
P20, 2311, H13, 2344, Starvax 420, 236, AdC3, S136, 2312, 2379, 2316, 2083, Nak80, 2767 …and so forth. |
| Sizzling/ Chilly Runner |
HUSKY, INCOE, YDDO, HASCO, DME, MoldMaster, Masterflow, Mastip, ZheJiang created brand…etc. |
| Mould Daily life: |
five,000 to 1,000,000 Photographs. (According to your operating atmosphere.) |
| Design & Program Softwares: |
CAD, CAM, CAE, Pro-E, UG, Soild performs, Moldflow, CATIA….and so on. |
| Equipments: |
Substantial pace CNC, Normal CNC, EDM, Wire Chopping, WEDM, Grinder, Plastic Injection Molding Machine for trial out mildew from fifty-3000T accessible. |
Products display
Solutions
Papler Sector gives provider of prototype making, mildew design and style, mold creation, mass generation and assembly provider in house. Our experience variety from basic design to tough specialized parts.
Firm Profile
Workshops and Equipments
Cooperating Clients
Packaging & Delivery
FAQ
one. Q: The place is your business or manufacturing facility?
A: We are located in HangZhou, We have our very own manufacturing facility.
two. Q: Can you make layout?
A: We will be happy to make CZPT types for you, and for totally free. Full CZPT Second & 3D will supply to clients right after get.
three. Q: What variety of CZPT you can make?
A: We can make all types of plastic injection mould, specially prosperous Expertise
on family moulds.
4. Q: What sort of information can you acknowledge?
A: We can accept diverse types of data files this sort of as DXF, DWG, IGS, IGES, STP, PRT, X_T, PDF.
five. Q: What type of metal do you use?
A: P20, P20 (H), 718, 718 (H), 2738, 2738 (H), H13, NAK80,2344, S136, 4Cr13, S55C,C45#
6. Q: What sort of material you use for examination CZPT and production?
A:PP, Laptop, PS, PE, HDPE, POM, PA6, PA66, PA6+GF, Stomach muscles, TPU, TPE, PVC, SMC, BMC,
We have prosperous knowledge for producing merchandise with these materials and know
how to change Parameter to get the ideal item.
seven. Q: How to send sample?
A: The quotation we supply you like The price of sample delivery 2 times samples by
DHL, UPS, EMS,FEDEX or TNT.
US $0.01-3
/ Piece
|
|
1 Piece
(Min. Order)
|
###
| Plastic Type: |
Thermosetting Plastic |
| Plastic Form: |
Powder |
| Molding Method: |
Injection Molding |
| Customization: |
Available |
| Material: |
ABS, PP, Nylon, PC, POM, PU, TPU, TPV, PBT, PC+Ab |
| Drawing: |
Provide by Customer(Dxf/Dwg/Prt/Sat/Iges/Step etc) |
###
###
###
| Product Description |
ODM plastic injection molding |
| Plastic Materials: |
PS, ABS, PP, PVC, PMMA, PBT, PC, POM, PA66, PA6, PBT+GF, PC/ABS, PEEK, HDPE, TPU, PET, PPO,…etc. |
| Standard: |
ISO9001:2008 |
| Quality: |
RoSH and SGS standard |
| Feature: |
Non marking and Non flash |
| Size: |
According to your 2D, 3D Drawing |
| Color,Quantity,Unit price,Tooling cost,Tooling size: |
To be discussed |
| Package: |
Standard exported Wooden box packed, Fumigation process(upon required) |
| Mold Building Lead Time: |
T1, 15-25 Working days, Part measurement report (upon required). |
| Export Country: |
All countries are reachable. |
| Experience: |
13 years experience in plastic injection mold making and plastic prouducts produce. |
| Mould Base: |
Hasco Standard, European Standard, World Standard |
| Mould Base Material: |
LKM, FUTA, HASCO, DME,…etc. Or as per Customer’s Requirment. |
| Surface Finish: |
Texture(MT standard), High gloss polishing |
| Cavity/Core Steel: |
P20, 2311, H13, 2344, Starvax 420, 236, AdC3, S136, 2312, 2379, 2316, 2083, Nak80, 2767 …etc. |
| Hot/ Cold Runner |
HUSKY, INCOE, YDDO, HASCO, DME, MoldMaster, Masterflow, Mastip, Taiwan made brand…etc. |
| Mould Life: |
5,000 to 1,000,000 Shots. (According to your working environment.) |
| Design & Program Softwares: |
CAD, CAM, CAE, Pro-E, UG, Soild works, Moldflow, CATIA….etc. |
| Equipments: |
High speed CNC, Standard CNC, EDM, Wire Cutting, WEDM, Grinder, Plastic Injection Molding Machine for trial out mold from 50-3000T available. |
US $0.01-3
/ Piece
|
|
1 Piece
(Min. Order)
|
###
| Plastic Type: |
Thermosetting Plastic |
| Plastic Form: |
Powder |
| Molding Method: |
Injection Molding |
| Customization: |
Available |
| Material: |
ABS, PP, Nylon, PC, POM, PU, TPU, TPV, PBT, PC+Ab |
| Drawing: |
Provide by Customer(Dxf/Dwg/Prt/Sat/Iges/Step etc) |
###
###
###
| Product Description |
ODM plastic injection molding |
| Plastic Materials: |
PS, ABS, PP, PVC, PMMA, PBT, PC, POM, PA66, PA6, PBT+GF, PC/ABS, PEEK, HDPE, TPU, PET, PPO,…etc. |
| Standard: |
ISO9001:2008 |
| Quality: |
RoSH and SGS standard |
| Feature: |
Non marking and Non flash |
| Size: |
According to your 2D, 3D Drawing |
| Color,Quantity,Unit price,Tooling cost,Tooling size: |
To be discussed |
| Package: |
Standard exported Wooden box packed, Fumigation process(upon required) |
| Mold Building Lead Time: |
T1, 15-25 Working days, Part measurement report (upon required). |
| Export Country: |
All countries are reachable. |
| Experience: |
13 years experience in plastic injection mold making and plastic prouducts produce. |
| Mould Base: |
Hasco Standard, European Standard, World Standard |
| Mould Base Material: |
LKM, FUTA, HASCO, DME,…etc. Or as per Customer’s Requirment. |
| Surface Finish: |
Texture(MT standard), High gloss polishing |
| Cavity/Core Steel: |
P20, 2311, H13, 2344, Starvax 420, 236, AdC3, S136, 2312, 2379, 2316, 2083, Nak80, 2767 …etc. |
| Hot/ Cold Runner |
HUSKY, INCOE, YDDO, HASCO, DME, MoldMaster, Masterflow, Mastip, Taiwan made brand…etc. |
| Mould Life: |
5,000 to 1,000,000 Shots. (According to your working environment.) |
| Design & Program Softwares: |
CAD, CAM, CAE, Pro-E, UG, Soild works, Moldflow, CATIA….etc. |
| Equipments: |
High speed CNC, Standard CNC, EDM, Wire Cutting, WEDM, Grinder, Plastic Injection Molding Machine for trial out mold from 50-3000T available. |
Injection Molded Parts – Design Considerations
If you want to produce high-quality Injection molded parts, there are several factors to consider before the design process. These factors include the Surface finish, Material compatibility, and Tooling fabrication. This article will focus on some of these factors. Ultimately, you can save time and money by designing the parts in-house.
Design considerations
 When creating a new part, or updating an existing part, design considerations for injection molded parts are critical. The decisions you make in these early stages of development can have a profound effect on the final product, and they can also have substantial cost and timing implications. In this guide, we’ll explore key design considerations, including how to maximize the efficiency of the injection molding process. We’ll also touch on how to optimize gate placement and parting lines.
To ensure a successful injection molding process, part design must balance structural integrity and plastic fill volume. This means creating parts with relatively thin walls that have adequate support and avoid warping or sinking. To do this, injection molded parts often feature ribs or projections to strengthen the walls. However, too thin of a wall can result in excessive plastic pressure and air traps.
One of the most important design considerations for injection molded parts is the direction of the parting line. For many applications, a parting line is obvious, but for others it’s a little less obvious. The first step in designing an injection mold is to determine which direction it should open.
Another critical design consideration is the part’s ejection. If a part isn’t ejected properly, it will stick to the mold. A part that has too many undercuts or ribs will end up stuck on the mold’s side, making it difficult to eject it from the mold. A part that has a draft angle of at least five degrees is much easier to eject.
Another important design consideration for an injection molded part is the type of plastic used. Some plastics do not tolerate undercuts. However, some materials are able to tolerate undercuts of up to five percent. Undercuts are not ideal and can increase the complexity and cost of the injection mold.
Another design consideration for injection molded parts is the radius of edges. Sharp corners can create high molded-in stresses and can lead to failure points. A radius eliminates this stress by redistributing the stress more evenly throughout the part. This also facilitates flow of the material through the mold.
Surface finish
Injection molded parts are often finished with additional processing in order to improve their aesthetic quality. There are a variety of finishing processes, including machining and sanding, which give injected molded parts a particular look, feel, or texture. The surface finish of a plastic part affects both its aesthetics and its functionality. According to the Society of Plastics Industry, certain standards for surface finish are essential to the aesthetics and durability of plastic parts.
Surface finish of injection molded parts depends on the primary design goal. For instance, some designs may need a part to be aesthetically pleasing while others may want to enhance its functionality. Surface texture is often used by designers and engineers to achieve different aesthetic goals, such as improving the product’s perceived value. A textured surface may also help hide imperfections and improve the part’s non-slip qualities.
Surface finish is a critical aspect of plastic injection molding. It can affect material selection, tooling, and other process decisions. It is important to determine the desired surface finish early in the design phase. A skilled plastic injection molder can assist you in making this decision. In addition to determining the finish you need, a skilled molder can help you decide the best material for the job.
The PIA classification system defines four basic grades for surface finish. There are subcategories for each grade. Group A surface finish is smooth, and grade B and C finishes are textured. The former is the most common and economical finish and is most suitable for industrial parts. It can hide deformations and tooling marks, and is the least expensive finish type.
Surface finish of injection molded parts can vary greatly, and can be crucial to the performance and appearance of the part. Some companies prefer plastic parts with a glossy finish, while others prefer a textured surface for aesthetic reasons. While the former may be better for aesthetic purposes, rougher surfaces are often preferred for functional or mechanical parts.
Material compatibility
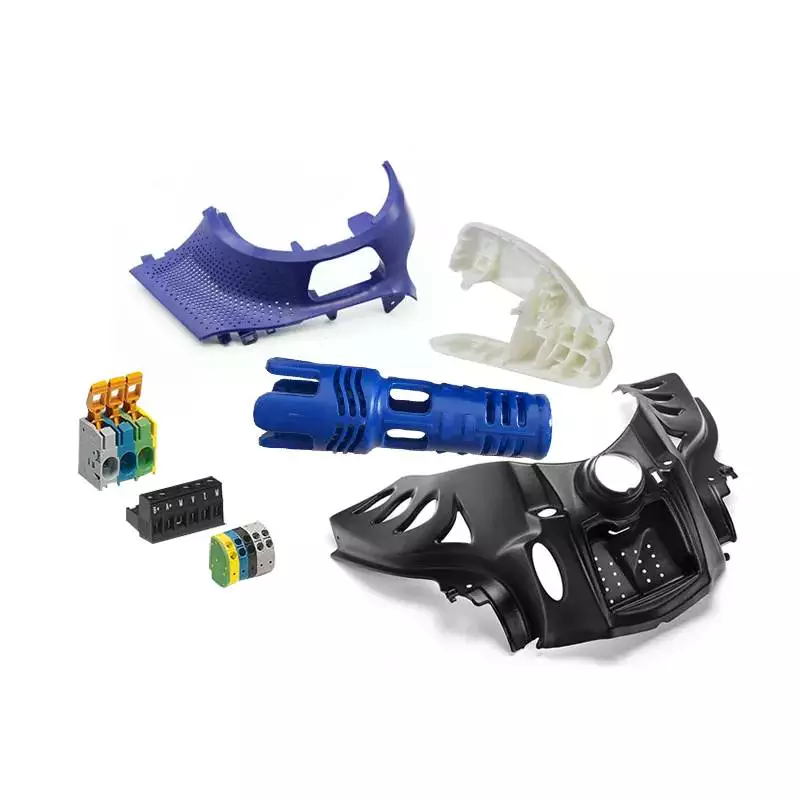 Material compatibility is important for the durability of your injection molded parts. You can use multiple materials in the same part by mixing resins. This is an ideal solution for parts that require adhesion, friction, or wear. Fast Radius can simplify the material selection process, optimize part design, and speed up production.
ABS is a thermoplastic polymer that can withstand a range of temperatures. Its low melting point means that it is easy to mold, and it has good chemical and moisture resistance. ABS also has good impact strength, and is highly durable. It is easy to recycle. Nylon is another versatile material for injection molding. It can be used for car tires, electrical components, and various apparel.
When choosing the material for your injection molded parts, keep in mind that the type of resin will determine their tolerance. Injection molding is compatible with a wide range of plastic resins. Some materials are more suitable than others for certain applications, and many plastics can be modified with stabilizers or additives to improve their properties. This flexibility allows the product development team to customize materials to achieve the performance characteristics they desire.
Polyamides are another great option for injection molding parts. Both natural and synthetic varieties of these plastics have excellent properties. However, they have some drawbacks. For instance, nylon injection molding is difficult and can result in inadequate filling. However, Nylon injection molding has many benefits, including high impact resistance and heat resistance.
Polybutylene terephthalate (PBT) is a high-molecular-weight polymer with excellent mechanical and chemical resistance. It is a good choice for components in the medical, automotive, and lighting industries. Its low water absorption and low flammability make it suitable for many applications.
Polyurethane (TPU) is another polymer option. It has excellent resistance to abrasion, chemicals, greases, and oils. It also has high temperature resistance, and is suitable for ozone environments. However, TPU is more expensive than TPE and requires drying before processing. Moreover, it has a short shelf life.
Tooling fabrication
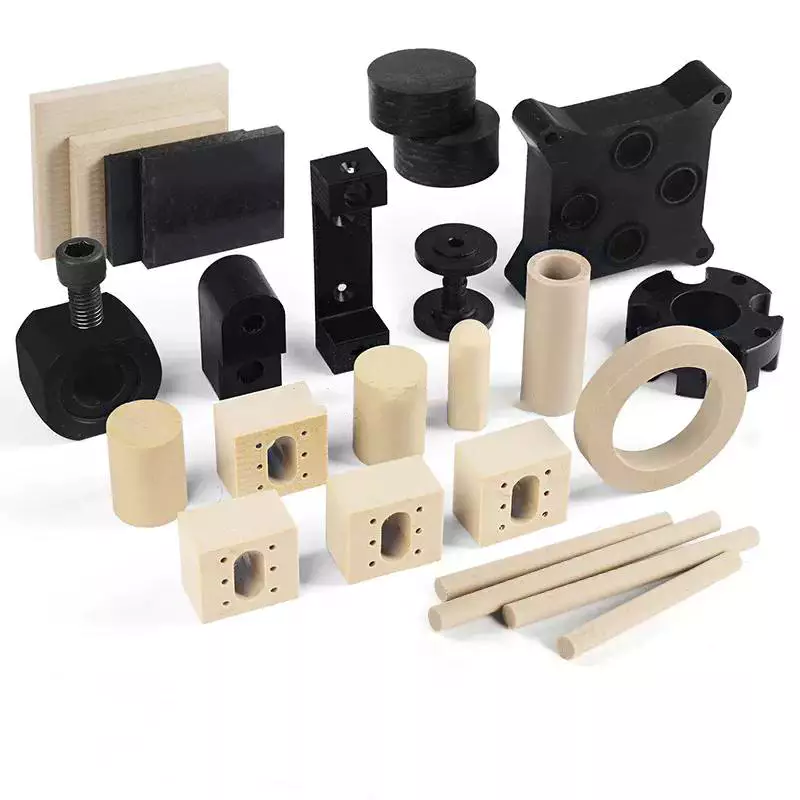 Tooling fabrication for injection-molded parts is an important component of the manufacturing process. The right design of the mold can reduce the cost and time required for a finished product. For instance, choosing the right type of core for the mold can reduce the amount of material used in the part, which is necessary to produce a high-quality product. It is also important to choose a design that is easy to mill into a mold.
Injection molding requires a mold with precise geometries. The mold tool must be constructed accurately and carefully to achieve the desired precision. It can be the biggest investment in the manufacturing process, but it is also critical to the success of a project. Large volume and high-precision parts often require more complex tooling, as they require the highest level of precision.
Tool steels typically used for injection moulding include H-13 and 420 stainless steel. Both of these materials are strong enough to produce parts of comparable hardness to wrought parts. These materials have low elongation values, so they are ideal for constructing injection moulding tools. Some of these steels also have excellent dimensional accuracy and are ideally suited for high-precision tool fabrication.
The process of plastic injection molding requires precise measuring and tooling fabrication. The mold must have the proper lead angle and space for the material to deform. Undercuts must be no larger than 5% of the diameter. Moreover, the injection molded part should be free of stripping or undercuts. Ideally, it should have a lead angle of 30o to 45o.
Various plastics can be used in the process of injection molding. The process can be used to produce cosmetic and end-use parts. Materials used in the molding process include silicone rubber and thermoplastics. If the part requires additional reinforcement, it can be reinforced with fibers, mineral particles, or flame retardant agents.
Increasingly advanced technologies have streamlined the process of tooling fabrication for injection moulded parts. The process has improved with the use of computer aided design, additive manufacturing, and CNC lathes. Approximately 15% of the cost of a finished injection molded part is spent on tooling fabrication.
editor by czh 2023-01-03
China Plastic Injection Molding Plastic Parts Molded Switch Housing roto mold vs injection mold
Merchandise Description
Product Description
Plastic injection molds and CZPT maker
one-Start from component style investigation
two-Mildew design drawing and DFM report offered so you can see how is the mold likely to be just before mildew producing
3-If merchandise is complex,moldflow report will be current as nicely
four-In house mould generating store guarantee you mould high quality beneath properly manage.
5-Normally it takes fifteen-25 operating times to make mold,exact time is dependent on part design and style
| Merchandise |
Plastic Parts |
Plastic substance |
Stomach muscles,PP,Nylon,Pc or any other materials as you require |
| Kind of enterprise |
Specialist company of injection molds and injection molding components |
Provider
|
OEM,Design and style based mostly on your idea or Make mold and create based mostly on your drawing |
| Style software program |
Solidworks, Professional-E, UG, CAD, Rhino and so forth. |
Drawing structure |
Stage, Igs, PDF, CAD and many others. |
Produce Dimension
|
From modest to big, based mostly on your drawing or sample |
Item fat
|
1g-10kgs |
| MOQ |
100PCS |
Manufacturing potential |
10,000pcs/working day |
| Assembly & Check |
Specialist assembly factory with 6 assembly traces |
Bundle
|
Standard carton, pallet or tailored deal |
| Payment details |
T/T, L/C, D/A, D/P, Western Union, MoneyGram, Veem, Paypal and so on |
Delivery time |
For mildew & samples: 3-4 months.
For mass manufacturing: 15 workdays |
| Shipping way |
By Courier DHL, Fedex, TNT, UPS, EMS, By Sea or By Air |
Prototype |
3D printing, CNC, Laser slicing etc |
Detailed Photos
How to Commence
CEMAL Enginnering , expert plastic mould company in China, we target on layout and production plastic molds for
the Automotive, Home Appliances and other sectors.
Excited and prepared to assist support your project from the early phases of part advancement and device style to fabrication and elements generation through expert engineering, producing, and project administration, we are assured that our support amount is next to none.
When you select CEMAL- no matter whether it’s for a single part, a tiny run or a multi-calendar year deal – you may get the identical focus to depth, the exact same problem-solving strategy, the identical high quality resolution. Which is the CEMAL guarantee.
Making our customers enjoyable, Keeping our consumer effective is the goal of CEMAL.
Why Select CEMAL
Are you plHangZhou to get a provide of personalized injection molds and possibly do not have an thought of which Company is very likely to offer you powerful merchandise? If yes, then this post will be a ideal CZPT for you as it attempts to spotlight a variety of motives as to why you need to decide on Loxin mould as your provider in injection molds. There are countless numbers of injection mold manufactures in China and consequently, identifying the best business to spouse with can quite be tough. Not all factories supply real merchandise or even supply the numerous services at affordable charges and there is thus the want to be cautious on the organization that you settle for. CEMAL mildew has been in existence for far more than ten years now and has proved to be the leading producer of the customized injection mold via the exemplary providers to the a variety of clients. It would hence be a clever option to take into account us as your companion in offer of mildew associated goods. Below are some of the reasons as to why you ought to consider our organization
All items are availed at cost-effective costs
At CEMAL mold, all production procedure is completed inside the business and nothing at all is purchased from other businesses and therefore guaranteeing that all merchandise are traded at the manufacturing facility value to the a variety of consumers. We do not offer our items through any center people but fairly directly to our customers. Brokers generally demand higher rates on the items in order to get their profits and for that reason that is why we avail all items directly to the users to steer clear of this sort of charges and that’s why avail the items at cost-effective charges to our customers.
Extremely knowledgeable in manufacturing of mildew
As mentioned before on, CEMAL mold has been in operation for much more than 10 several years and consequently has successful understanding in manufacturing of molds and the relevant services to out esteemed clients. We have transacted with a variety of clients even in the European countries and have often given a positive feedback on our companies. If you still will not think in us then you can refer from your place on the sort of providers provided. We can even supply contacts of the different consumers served if they enable us to do so.
Top quality services are provided
Our engineers are highly expert and you can be positive that they offer you high quality companies that fulfill our customer’s satisfaction. Our major aim is to make sure that all clients are entirely satisfied in the mould injection solutions provided and the business is often all set to even make any alterations to meet the customer requires. Our managers are helpful and talk right to you if you need to have a source of our products without involving any intermediaries. This is in distinction to other manufactures who retain the services of product sales girls to advertise the items as they shell out them on a commission foundation. This phone calls for much more costs as the amount is later on transferred to the cost of the products
FAQ
one. Are you a investing firm or a manufacturer?
We are a maker as you can see our workshop as earlier mentioned.
two. What kind of trade terms can you do?
EX-Performs,FOB,CIF,DDP DDU
3. What is your phrases of payment?
50% Mold value deposit,equilibrium mould expense +50% production price paid out when samples confimed,Stability production price paid towards copy of B/L. We settle for T/T
4. Do you assistance OEM ?
Indeed, we can generate by specialized drawings or samples.
five. How about your shipping and delivery time?
Usually, it get 20-thirty operating days ( fifteen-20days make mould, 5-ten days for mass generation).
US $1.99-9.99
/ Piece
|
|
500 Pieces
(Min. Order)
|
###
| After-sales Service: |
2 Years |
| Warranty: |
2 Years |
| Type: |
Plastic Mould Parts |
| Material: |
Plastic, ABS,PP,PC,PA,PMMA,PS,POM etc. |
| Application: |
Electronic, Hardware, Machinery, Daily Use, Furniture, Household Applicances, Car |
| Certification: |
ISO9001, SGS |
###
###
###
| Item |
Plastic Parts |
Plastic material |
ABS,PP,Nylon,PC or any other material as you need |
| Type of enterprise |
Professional manufacturer of injection molds and injection molding parts |
บริการ
|
OEM,Design based on your idea or Make mold and produce based on your drawing |
| Design software |
Solidworks, Pro-E, UG, CAD, Rhino etc. |
Drawing format |
Step, Igs, PDF, CAD etc. |
Produce Size
|
From small to big, based on your drawing or sample |
Product weight
|
1g-10kgs |
| MOQ |
100PCS |
Production ability |
10,000pcs/day |
| Assembly & Test |
Professional assembly factory with 6 assembly lines |
Package
|
Standard carton, pallet or customized package |
| Payment details |
T/T, L/C, D/A, D/P, Western Union, MoneyGram, Veem, Paypal etc |
Delivery time |
For mold & samples: 3-4 weeks.
For mass production: 15 workdays |
| Shipping way |
By Courier DHL, Fedex, TNT, UPS, EMS, By Sea or By Air |
Prototype |
3D printing, CNC, Laser cutting etc |
US $1.99-9.99
/ Piece
|
|
500 Pieces
(Min. Order)
|
###
| After-sales Service: |
2 Years |
| Warranty: |
2 Years |
| Type: |
Plastic Mould Parts |
| Material: |
Plastic, ABS,PP,PC,PA,PMMA,PS,POM etc. |
| Application: |
Electronic, Hardware, Machinery, Daily Use, Furniture, Household Applicances, Car |
| Certification: |
ISO9001, SGS |
###
###
###
| Item |
Plastic Parts |
Plastic material |
ABS,PP,Nylon,PC or any other material as you need |
| Type of enterprise |
Professional manufacturer of injection molds and injection molding parts |
บริการ
|
OEM,Design based on your idea or Make mold and produce based on your drawing |
| Design software |
Solidworks, Pro-E, UG, CAD, Rhino etc. |
Drawing format |
Step, Igs, PDF, CAD etc. |
Produce Size
|
From small to big, based on your drawing or sample |
Product weight
|
1g-10kgs |
| MOQ |
100PCS |
Production ability |
10,000pcs/day |
| Assembly & Test |
Professional assembly factory with 6 assembly lines |
Package
|
Standard carton, pallet or customized package |
| Payment details |
T/T, L/C, D/A, D/P, Western Union, MoneyGram, Veem, Paypal etc |
Delivery time |
For mold & samples: 3-4 weeks.
For mass production: 15 workdays |
| Shipping way |
By Courier DHL, Fedex, TNT, UPS, EMS, By Sea or By Air |
Prototype |
3D printing, CNC, Laser cutting etc |
Designing Injection Molded Parts
Designing injection molded parts involves careful consideration of various parameters, including the wall thickness and draft angle. These factors are essential for a strong, durable part. Improper wall thickness can lead to sinking and warping defects. To avoid these issues, ensure that the walls of your injection-molded parts have a uniform thickness that does not vary too much from the rest of the part.
Designing out sharp corners in injection molded parts
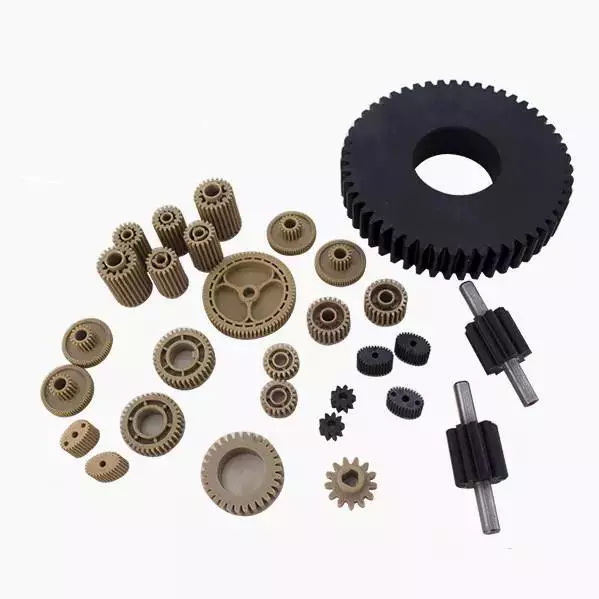 When designing an injection molded part, it’s important to consider the corner radius. Sharp corners will create more stress, and this will lead to weak spots and cracks. Creating a radius around the corner helps distribute stress evenly and allows easier material flow and part ejection. Additionally, sharp corners in a mold can collect contaminants and create defects, including surface delamination.
Sharp corners in injection molded parts are a common source of stress and can cause the part to become damaged during the manufacturing process. In addition to trapping air, sharp corners may also lead to localized high temperatures that degrade the part. To reduce these risks, consider adding radii to all sharp corners.
Another important design factor to consider is wall thickness. Parts that have a smooth transition between sections should be designed with a minimum of five millimeters of wall thickness. Anything thicker will increase production cycle time and may also negatively impact mechanical properties. The use of fillets and chamfers can also help avoid these problems.
Designing out sharp corners in injection molded components can prevent costly problems from occurring during the manufacturing process. While the process is simple and straightforward, it needs to be done correctly to ensure quality. By following best practices, designers can ensure their parts won’t develop any problems or sink, warp, or voids. A poor design can also cause damage to the mold, which can cost thousands of dollars and hundreds of hours to redesign.
When designing injection molded parts, designers should consider the following guidelines. Incorporate internal and external radiuses. The internal radius (also called a fillet radius) is designed into the mold for improved quality and strength during the molding process. This radius is typically located on the inside corners or the bottom of a compartment. It can also be used for connecting walls and ribs. An external radius, on the other hand, is known as a round radius.
A right-angled part with sharp corners has a tendency to be loaded by pushing the vertical wall to the left. This creates a high-level of molded-in stress in the part. The resulting part may be weaker than expected because of the increased stress on the corner.
Importance of uniform wall thickness
Uniform wall thickness is a critical factor when designing injection-molded parts. This ensures that molten polymers can flow efficiently throughout the part. Additionally, it facilitates ideal processing. Varying wall thickness can cause problems during molding, such as air trapping, unbalanced filling, and weld lines. To ensure that your injection-molded parts are uniform, consult a plastic injection molding company that specializes in uniform wall thickness.
Injection-molded parts are more durable when the walls are uniform. A thin wall reduces the volume of material used in the part. However, thin walls can break during ejection. In addition, thin walls increase the possibility of voids. To prevent such problems, use larger machines that can produce parts with uniform wall thickness. This way, parts are easier to handle and ship.
Another important factor is the presence of gussets. These are support structures that stick out from a part’s surface. Gussets are useful for preventing warping, because they provide rigidity to thin unsupported sections. For this reason, gussets are essential when designing an injection-molded part.
Uniform wall thickness is especially critical in parts that have bends or rims. A uniform thickness helps maintain the mechanical strength and appearance of a part. However, this can be tricky as you may need to balance optical properties with mechanical ones. At Providence, we have the experience to help you navigate these challenges and produce quality parts.
Proper wall thickness is important for many reasons. It can affect both cost and production speed. The minimum wall thickness for injection molded parts depends on the part size, structural requirements, and flow behavior of the resin. Typically, injection molded parts have walls that are 2mm to 4mm thick. However, thin wall injection molding produces parts with walls as thin as 0.5mm. If you’re having trouble choosing the right wall thickness, consult an experienced injection molding company that can help you determine the appropriate wall thickness for your part.
Uneven wall thickness causes problems during injection molding. The uneven wall thickness may make the material flow through the part too quickly, or it may cause it to cool too slowly. This can lead to warping, twisting, or cracks. Even worse, uneven wall thickness can cause parts to become permanently damaged when they are ejected from the mold.
Importance of draft angle
 Draft angles are an important part of design for injection molded parts. These angles are necessary because friction occurs on surfaces that come into contact with the mold during the molding process. A part with a simple geometry would only require a single degree of draft, but larger parts would need at least two degrees.
Almost all parts requiring injection molding will require some amount of draft. The better the draft, the less likely the parts will have a poor finish and may bend or break. Furthermore, parts with inadequate draft will take longer to cool, extending cycle times. Moreover, if the parts are too thick or have too little draft, they may become warped.
Having a draft angle in injection molding is very important, especially if the mold has sharp corners. Without it, parts will come out scratched and will shorten the life of the mold. In some cases, parts may even not be able to eject from the mold at all. To prevent this, air needs to be allowed to get between the plastic and metal. This allows air to escape and prevents warping during ejection.
The importance of draft angle is often overlooked in the design process. Adding this angle to the mold can help prevent problems with mold release and reduce production costs. A draft angle will also allow parts to release from the mold more easily and will lead to better cosmetic finishes and fewer rejected parts. Additionally, it will reduce the need for costly elaborate ejection setups.
Draft angle should be added to the design as early as possible. It’s crucial for the success of the injection molding process, so it is best to incorporate it early in the design process. Even 3D printed parts can benefit from this detail. The size of the draft angle is also important, especially for core surfaces.
A draft angle can be large or small. The larger the draft angle, the easier it is to release the mold after the mold is completed. However, if the draft angle is too small, it can lead to scrapes on the edges or large ejector pin marks. Draft angles that are too small can lead to cracks and increase mold expenses.
Cost
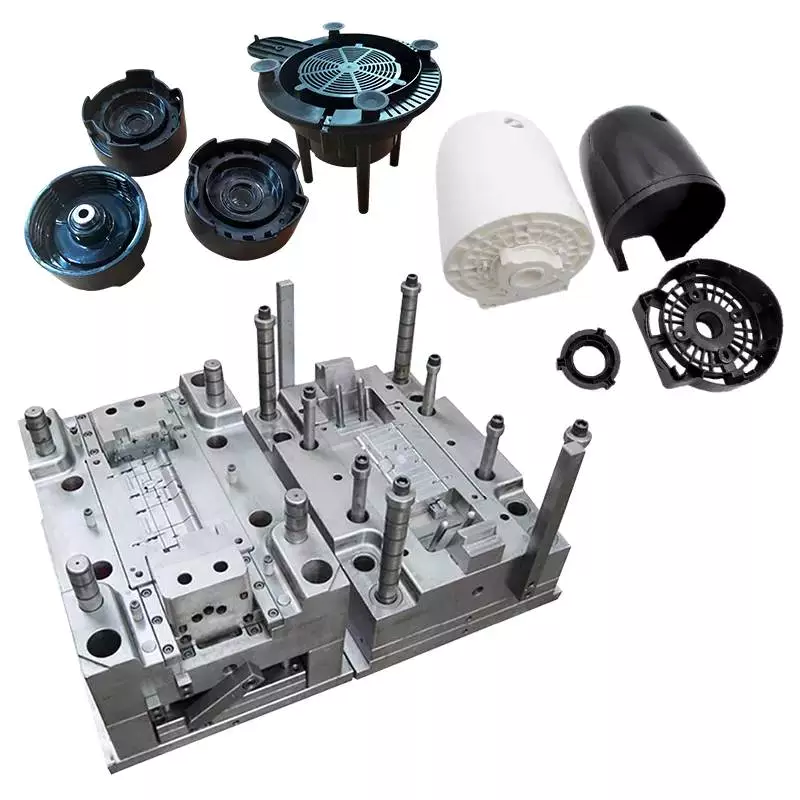 There are many factors that contribute to the cost of injection-molded parts, including the material used for the mold and the complexity of the design. For example, larger parts will require a larger injection mold, which will cost more to manufacture. Additionally, more complex parts may require a mold with special features. Mold makers can advise you on how to design your part in order to reduce the overall cost of an injection-molded part.
One of the biggest costs related to the production of injection molded parts is the cost of the tooling. Tooling costs can reach $1,000 or more, depending on the design, materials, and finishing options. Tooling costs are less if the part quantity is small and repeatable. Higher part volumes may require a new mold and tooling.
Injection-molded parts’ cost depends on the material used and the price of procuring the material. The type of material also influences how long the part will last. Plastics that contain high percentages of glass fibers are abrasive and can damage an injection mold. Therefore, they are more expensive but may not be necessary for certain applications. Additionally, the material’s thermal properties may also affect the cycle time.
Mold size is another factor that impacts the cost. Larger molds require more CNC machinery and building space than smaller molds. Additionally, the complexity of the part will also impact the cost. Injection molds with sharp corners and complex ribs will cost more than small injection molds without intricate designs.
Injection molding is a complex process that requires a variety of moving parts. During the process, a critical piece of equipment is the injection die. This machine is a large part of the process, and comes in different sizes and shapes. Its purpose is to accept the hot plastic and machine it to extremely precise tolerances.
If your project requires a complex product with a high degree of complexity, injection molding is an excellent choice. It is ideal for initial product development, crowdfunding campaigns, and on-demand production. Mold modifications can also lower the cost of injection molding.
editor by czh 2023-01-02
China Professional Custom Molded Plastic Parts Plastic Products Custom Plastic Injection Molding Service injection moulding for parts
Product Description
Produt Description
| Merchandise Identify |
Specialist Personalized Molded Plastic Parts Plastic Items Custom made Plastic Injection Molding Services |
| Content |
Abs/PE6/PE66/PVC/Laptop/PP/POM and many others |
| Functionality |
UV resistance, flame retardant, minimal temperature resistance, versatile/rigid and so forth |
| Software |
Industial, electronics etc |
| Mold Life |
100,000-500,000 photographs |
| Mildew Cavity |
Single cavity, multi cavity, based on customer’s ask for |
| Mildew Runner |
Scorching runner/ Chilly runner |
| Item Area Therapy |
Painting/ Sprucing/ Laser Carving/ Monitor Printing/ UV Printing/ Mirror Finishing/ Electroplated/ Oxidation/ Sand Blasting/ Passivating |
| Injection Molding Capacity |
one-5000g |
| MOQ |
Negotiable |
| Packing |
Common export carton packing, or according to customer’s request |
| Parameters |
Inch, centimeter, millimeter etc |
| OEM/ODM |
Heat welcome to make contact with us |
| Benefits |
Aggressive cost & Fast Shipping and delivery & Excellent high quality |
| Payment Phrases |
For mold: 50% advanceT/T payment, stability will be following you validate our samples For creation: 30%T/T, harmony will be following acquired our B/L copy |
Products Show
Comprehensive Items
PLEASE NOTE:
These products belong to our consumers. We just display them to show our potential, not in sale!
Packing
The way of packing depends on customer’s need.
Business Profile
Our company was recognized in 2003. We are oem services manufacturer and trader specialized in analysis.We are located in Xihu (West Lake) Dis. County, ZHangZhoug Province, with convenient transportation entry. Our yearly income benefit is in excess of USD 800,000.
With more than 10 years’ improvement, we have proven solid organization interactions with customers from Western Europe, Northern Europe, South The usa and North America.
We can regularly supply large high quality merchandise, affordable prices and the best providers for our customers. We produce and generate several types of plastic products.such as vehicle components, machinery fitting, house equipment, digital items, electrical appliance, computer systems, miniature switches, architecture and so on. We can produce Injection Molding merchandise,extrusion molding products and blow molding goods,we produce according to clients’ sample or drawing.
We can use a lot of components to create , this sort of as Abdominal muscles, PP, PE, PS, PVC, Computer, PBT, POM, PET, LDPE, TPE and so on.
If you are intrigued in any of our goods or would like to go over a custom made order, make sure you feel free of charge to make contact with us. We are searching ahead to forming productive enterprise relationships with new clientele in the in close proximity to future.
Our Benefits
Engineering abilities:
- Entirely use high performance raw components for manufacturing
- Assembled Plastic Components
- Metallic part pressed-in or Inserts Plastic components
- Specialty Surface area Finishes
- Lapping
- 3D printing for customer style screening
- Customized Packaging
- Several extra elements are free for consumer
- Has a metal parts workshop to provide metallic parts.
Spouse:
Our merchandise have been bought to renowned businesses in China, European and export numerous nations around the world, such as the Usa, Canada, Germany,the Netherlands,India,Saudi Arabia and so on.
We are warm welcome and we will just take care for the each inquiry .we always aimed to trace the client 1st, high quality 1st!We will spend wonderful focus reply every single inquiry.
We are looking ahead to forming successful company relationships with new clients in the close to future.
Please feel totally free to contact us,We imagine we will be your very good organization companion!
FAQ
one. Who are we?
We are based mostly in ZHangZhoug, China, start from 2007,promote to Southern Europe(20.00%),Domestic Market place(twenty.00%),North The united states(fifteen.00%),Western Europe(15.00%),Japanese Asia(10.00%),Oceania(10.00%),Northern Europe(5.00%),Japanese Europe(5.00%),South Asia(.00%),South The us(.00%),Central The united states(.00%),Africa(.00%),Mid East(.00%),Southeast Asia(.00%). There are whole about eleven-fifty men and women in our business office.
two. How can we promise high quality?
Often a pre-manufacturing sample just before mass manufacturing
Constantly ultimate Inspection ahead of shipment
three.What can you get from us?
Tailored Plastic Injection Molding Elements, Tailored Plastic Extrusion Profiles
4. Why ought to you buy from us not from other suppliers?
we have a lot more than ten many years experience for personalized injection molding support &plastic extrusion profiles as customer’s design or sample
5. What is actually your common lead time for mold and mass creation?
Normally 20-twenty five times for molding ,mass creation depending on get qty.
six.If the things we buy from your firm are not of perfected good quality/defective, what can we do?
Pls speak to with us freely in a 7 days following your got the goods.Kindly send out us pictures of all the negative items or any proof. Soon after affirmation, we can alternative/ refund/ deduct the fee from next get.
| Material: |
ABS |
| Application: |
Electronics, Automotive |
| Service: |
OEM |
| Color: |
Custom Color |
| Drawing Format: |
Step |
| Process: |
Injection Mould Plastic Part |
###
###
###
| Product Name |
Professional Custom Molded Plastic Parts Plastic Products Custom Plastic Injection Molding Service |
| วัสดุ |
ABS/PE6/PE66/PVC/PC/PP/POM etc |
| Performance |
UV resistance, flame retardant, low temperature resistance, flexible/rigid etc |
| แอปพลิเคชัน |
Industial, electronics etc |
| Mold Life |
100,000-500,000 shots |
| Mold Cavity |
Single cavity, multi cavity, based on customer’s request |
| Mold Runner |
Hot runner/ Cold runner |
| Product Surface Treatment |
Painting/ Polishing/ Laser Carving/ Screen Printing/ UV Printing/ Mirror Finishing/ Electroplated/ Oxidation/ Sand Blasting/ Passivating |
| Injection Molding Capability |
1-5000g |
| MOQ |
Negotiable |
| Packing |
Standard export carton packing, or according to customer’s request |
| Parameters |
Inch, centimeter, millimeter etc |
| OEM/ODM |
Warm welcome to contact us |
| Advantages |
Competitive price & Fast Delivery & Good quality |
| Payment Terms |
For mold: 50% advanceT/T payment, balance will be after you confirm our samples; For production: 30%T/T, balance will be after received our B/L copy |
| Material: |
ABS |
| Application: |
Electronics, Automotive |
| Service: |
OEM |
| Color: |
Custom Color |
| Drawing Format: |
Step |
| Process: |
Injection Mould Plastic Part |
###
###
###
| Product Name |
Professional Custom Molded Plastic Parts Plastic Products Custom Plastic Injection Molding Service |
| วัสดุ |
ABS/PE6/PE66/PVC/PC/PP/POM etc |
| Performance |
UV resistance, flame retardant, low temperature resistance, flexible/rigid etc |
| แอปพลิเคชัน |
Industial, electronics etc |
| Mold Life |
100,000-500,000 shots |
| Mold Cavity |
Single cavity, multi cavity, based on customer’s request |
| Mold Runner |
Hot runner/ Cold runner |
| Product Surface Treatment |
Painting/ Polishing/ Laser Carving/ Screen Printing/ UV Printing/ Mirror Finishing/ Electroplated/ Oxidation/ Sand Blasting/ Passivating |
| Injection Molding Capability |
1-5000g |
| MOQ |
Negotiable |
| Packing |
Standard export carton packing, or according to customer’s request |
| Parameters |
Inch, centimeter, millimeter etc |
| OEM/ODM |
Warm welcome to contact us |
| Advantages |
Competitive price & Fast Delivery & Good quality |
| Payment Terms |
For mold: 50% advanceT/T payment, balance will be after you confirm our samples; For production: 30%T/T, balance will be after received our B/L copy |
Importance of Wall Thickness in Injection Molded Parts
When designing injection molded parts, it is important to keep the wall thickness uniform. Uneven wall thickness can lead to warping and sinking. To minimize these problems, injection molded parts should have a wall thickness of 40 to 60 percent of the adjacent wall. The thickness of the wall should also fit within the range recommended for the resin that is being used. If the wall thickness is too thick, it should be cored out. Unnecessary wall thickness alters the dimensions of the part, reduces its strength, and may require post-process machining.
Designing out sharp corners on injection molded parts
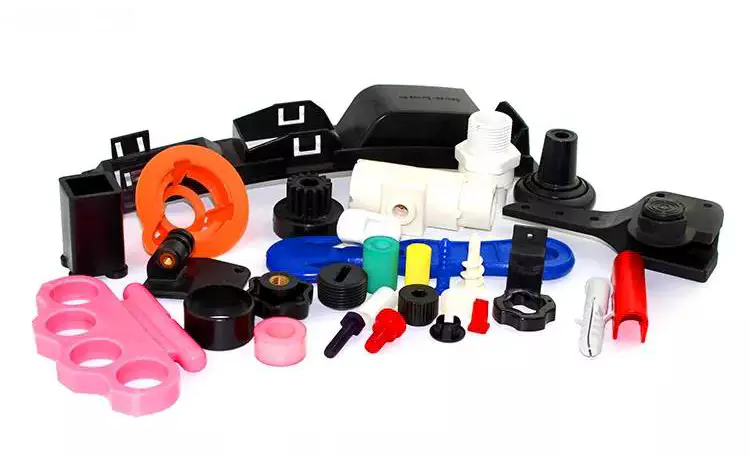 Designing out sharp corners on injection molded components can be a challenging process. There are several factors to consider that impact how much corner radius you need to design out. A general rule is to use a radius that is about 0.5 times the thickness of the adjacent wall. This will prevent sharp corners from occurring on a part that is manufactured from injection molding.
Sharp corners can obstruct the flow of plastic melt into the mold and create flaws on parts. They can also cause stress concentration, which can compromise the strength of the part. To avoid this, sharp corners should be designed out. Adding radii to the corners is also an effective way to avoid sharp angles.
Another common problem is the presence of overhangs. Injection molding parts with overhangs tend to have side-action cores, which enter from the top or bottom. As a result, the cost of making these parts goes up quickly. Moreover, the process of solidification and cooling takes up more than half of the injection molding cycle. This makes it more cost-effective to design parts with minimal overhangs.
Undercuts on injection molded parts should be designed with a greater radius, preferably one or two times the part’s wall thickness. The inside radius of corners should be at least 0.5 times the wall thickness and the outside radius should be 1.5 times the wall thickness. This will help maintain a consistent wall thickness throughout the part. Avoiding undercuts is also important for easy ejection from the mold. If undercuts are present, they can cause a part to stick inside the mold after it has cooled.
Keeping wall thickness uniform is another important issue when designing plastic parts. Inconsistent wall thickness will increase the chance of warping and other defects.
Adding inserts to injection molded parts
Adding inserts to injection molded parts can be a cost-effective way to enhance the functionality of your products. Inserts are usually manufactured from a wide range of materials, including stainless steel, brass, aluminum, bronze, copper, Monel, nickel/nickel alloy, and more. Selecting the right material for your parts depends on the application. Choosing the correct material can help prevent defects and keep production cycles short. The insert material should be durable and resist deformation during the injection molding process. It must also be thin enough to provide the desired grip and have a proper mold depth.
The benefits of adding inserts to injection molded parts include the ability to design parts with unique shapes. These parts can be aesthetically pleasing, while still remaining durable and resistant to wear and tear. In addition, insert molding allows products to have a good external finish. In addition to being cost-effective, insert molding is considered a more efficient manufacturing method than other conventional methods.
Adding inserts to injection molded parts is an excellent way to enhance the strength and performance of your products. There are many different types of inserts, including threaded nuts, bushings, pins, and blades. Some types are even available with knurled outer surfaces that help them adhere to plastic.
In addition to being cost-effective, insert molding is environmentally friendly and compatible with many types of materials. Typical inserts are made of metal or plastic. Depending on the application, stiffening inserts may also be made from wood.
Importance of uniform wall thickness
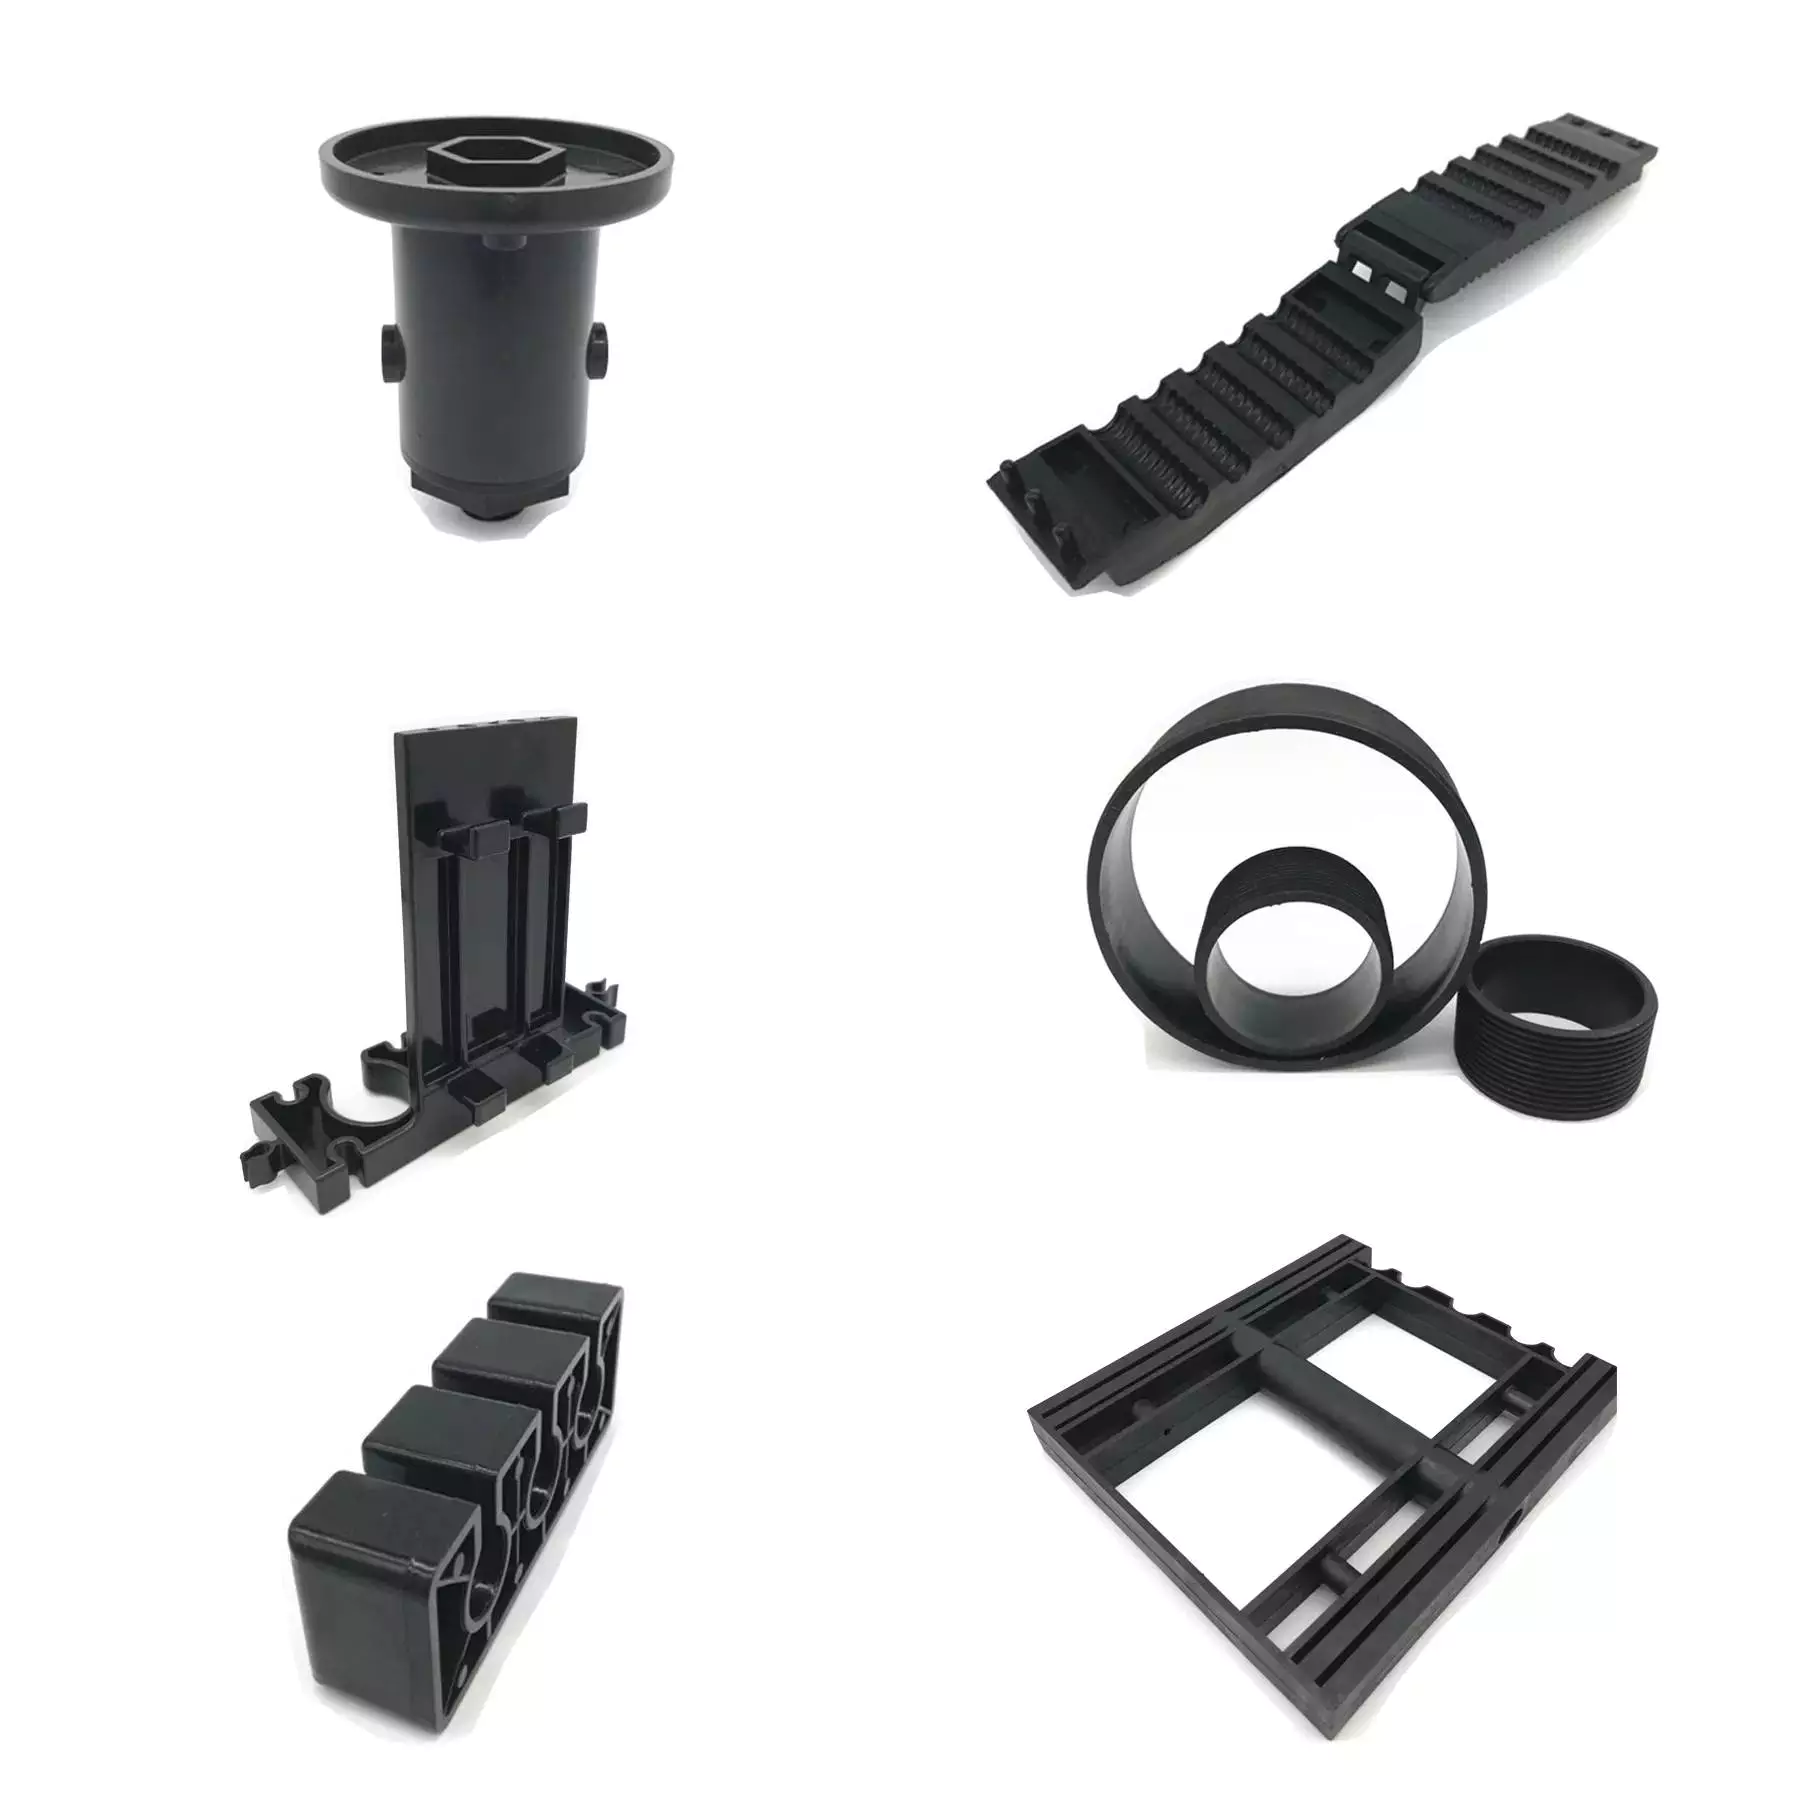 The uniformity of wall thickness is an essential factor in the plastic injection molding process. It not only provides the best processing results, but also ensures that the molded part is consistently balanced. This uniformity is especially important for plastics, since they are poor heat conductors. Moreover, if the wall thickness of an injection molded part varies, air will trap and the part will exhibit a poorly balanced filling pattern.
Uniform wall thickness also helps reduce shrinkage. Different materials have different shrinkage rates. For instance, thick parts take longer time to cool than thin ones. As the part’s thickness increases, cooling time doubles. This relationship is due to the one-dimensional heat conduction equation, which shows that heat flows from the center of the part toward the cooling channel. However, this relationship does not hold for all types of plastics.
The general rule for maintaining uniform wall thickness in injection molded parts is that walls should be no thicker than 3mm. In some cases, thicker walls can be used, but they will significantly increase production time and detract from the part’s aesthetic appeal and functionality. Furthermore, the thickness of adjacent walls should be no thicker than 40-60% of each other.
The uniformity of wall thickness is critical to the overall quality and efficiency of the injection molding process. An uneven wall thickness can cause twisting, warping, cracking, and even collapse. A uniform wall thickness also reduces residual stress and shrinkage. Injection molded parts are more stable when the wall thickness is uniform.
An injection molded part with thick walls can be problematic, especially when the molded parts are shaped like a cube. A non-uniform wall thickness can result in problems and costly retooling. Fortunately, there are solutions to this problem. The first step is to understand the problem areas and take action.
Using 3D printing to fabricate molds
 The use of 3D printed molds allows manufacturers to manufacture a wide range of injection molded parts. However, 3D-printed molds are not as strong as those made from metallic materials. This means that they do not withstand high temperatures, which can degrade them. As such, they are not suitable for projects that require smooth finishing. In order to reduce this risk, 3D-printed molds can be treated with ceramic coatings.
Using 3D printing to fabricate injection molds can help reduce costs and lead times, allowing manufacturers to bring their products to market faster. This process also has the advantage of being highly efficient, as molds made using 3D printing can be designed to last for many years.
The first step in fabricating an injection mold is to design a design. This design can be complex or simple, depending on the part. The design of the mold can be intricate. A simple example of a mold would be a red cup, with an interior and exterior. The interior portion would have a large cone of material protruding from the other side.
Injection molding is an effective way to produce thousands of parts. However, many engineering companies do not have access to expensive 3D printers. To solve this problem, companies should consider using outside suppliers. In addition to speeding up the manufacturing process, 3D printing can reduce the cost of sample parts.
Plastic injection molding still remains the most popular method for high volume production. However, this process requires a large up-front capital investment and takes a while to adapt. Its advantages include the ability to use multiple molds at once, minimal material wastage, and precision dosing. With an increasing number of materials available, 3D printing can be a smart option for companies looking to manufacture a variety of plastic parts.
editor by czh 2023-01-01
China Injection Molding Parts Suppliers Custom Plastic Electroplated Injection Molded wholesaler
Solution Description
Merchandise PARAMETERS
| Merchandise Identify |
injection molding elements suppliers customized plastic electroplated injection molded |
|
Mould Core/Cavity
|
DIN2312,2738,2344,718,S136,8407,NAK80,SKD61,P20, P20HH, H13, 420ss etc.
|
|
Hardness of steel
|
33-38HRC prehard, 46~56 HRC hardened
|
|
Mould Normal
|
HASCO,DME,MEUSBURGER,JIS,CHINA LKM Regular
|
|
Mould Base
|
LKM&Hasco&DME standard (A,B plate 1730,2311,2312,1050,P20 )
|
|
Cavity
|
Single/Family members/Multi
|
|
Runner
|
Scorching/Chilly Runner
|
|
Mould Size
|
a hundred and fifty*150mm Min, 3000*2500mm Max
|
|
Surface of Mould
|
EDM VDI/ Higher Polish&Texture
|
|
Plastic substance
|
PP, Computer, PS, PE, PET, POM, PA, PU, PVC, Stomach muscles, HIPS, PMMA, Nylon, and with GF, and so forth.
|
|
Mould Existence
|
Prototype one thousand-25,000 preproduction 50,000-10,0000 Large generation 300,000-1,000,000 photographs based mostly on Quantity requirements
|
|
Specification
|
Is dependent on the customer’s needs.
|
|
Trade terms
|
FOB HangZhou, EXW, CIF
|
|
Export to
|
Europe nations,United states,Mexico,Australia ,Middle-east ,Asia etc
|
|
Mildew sizzling runner
|
DME, HASCO, YUDO, Mold-Masters, HRS, Synventive, etc, or per buyer need
|
|
Mould gate type
|
stage gate, facet gate, sub gate, tunnel gate, banana gate, immediate gate, tab gate, sizzling runner valve gate, hot runner to cold runner, etc.
|
|
Direct time 1st Trial
|
20-45Days based mostly on distinct molds
|
|
Exterior package
|
Standard picket instances or as your need
|
|
Interior package
|
Extend water-resistant film & Every Mould painted, anti-rust oil.3. Spare elements together with the mildew shipment. 4. Vaccum package
|
Customized Solution
MANUFACTURING Method
ABOUT US
Certification
Shipping and delivery & PAYMENT
FAQ
| Q1: What is your company’s principal solution? |
| A: Our business is specialised in injection molding moulds and injection plastic items. We can customize all varieties of injection plastic items in accordance to your needs or 3D drawing. |
| |
| Q2: How can I get the samples to examine the good quality? |
| A: 1) You can occur to have the CZPT examination right. 2) We could send out samples & CZPT operating video clip to you. |
| |
| Q3: Can you make multi-cavity molds? |
| A: Of course, we are capable of creating molds in 16, 24, 48, and sixty four cavities. |
| |
| This autumn: What certificates are you qualified for? |
| A: We are qualified in ISO9001, and we have a method for TS16949. |
| |
| Q5: How do you make our enterprise a prolonged-term and very good romantic relationship? |
| A:1. We maintain very good top quality, on-time supply, and aggressive price to make certain our clients gain from the ideal high quality products 2. We benefit each client, no issue exactly where they come from, or how massive the buy they place. |
| |
| Q6: I have an notion for a new product, but don’t know if it can be created. Can you help? |
| A: Sure! We are usually pleased to function with possible customers to assess the specialized feasibility of your concept or design and we can suggest on components tooling and probably set-up costs. |
Welcome you for your inquiry and solution information. We will reply to you as before long as attainable.
aNUmmFACTURING TECHN
Merchandise PARAMEERS
PT PAAMENT
| Warranty: |
1 Year |
| Shaping Mode: |
Injection Mould |
| Surface Finish Process: |
Polishing |
| Mould Cavity: |
Multi Cavity |
| Plastic Material: |
ABS |
| Process Combination Type: |
Single-Process Mode |
###
###
###
| Item Name |
injection molding parts suppliers custom plastic electroplated injection molded |
|
Mould Core/Cavity
|
DIN2312,2738,2344,718,S136,8407,NAK80,SKD61,P20, P20HH, H13, 420ss etc.
|
|
Hardness of steel
|
33-38HRC prehard, 46~56 HRC hardened
|
|
Mould Standard
|
HASCO,DME,MEUSBURGER,JIS,CHINA LKM Standard
|
|
Mould Base
|
LKM&Hasco&DME standard (A,B plate 1730,2311,2312,1050,P20 )
|
|
Cavity
|
Single/Family/Multi
|
|
Runner
|
Hot/Cold Runner
|
|
Mould Size
|
150*150mm Min, 3000*2500mm Max
|
|
Surface of Mould
|
EDM VDI/ High Polish&Texture
|
|
Plastic material
|
PP, PC, PS, PE, PET, POM, PA, PU, PVC, ABS, HIPS, PMMA, Nylon, and with GF, etc.
|
|
Mould Life
|
Prototype 1000-25,000; preproduction 50,000-10,0000; High production 300,000-1,000,000 shots based on Volume requirements
|
|
Specification
|
Depends on the customer’s requirements.
|
|
Trade terms
|
FOB Shenzhen, EXW, CIF
|
|
Export to
|
Europe countries,USA,Mexico,Australia ,Middle-east ,Asia etc
|
|
Mold hot runner
|
DME, HASCO, YUDO, Mold-Masters, HRS, Synventive, etc, or per customer requirement
|
|
Mold gate type
|
point gate, side gate, sub gate, tunnel gate, banana gate, direct gate, tab gate, hot runner valve gate, hot runner to cold runner, etc.
|
|
Lead time 1st Trial
|
20-45Days based on different molds
|
|
Outside package
|
Standard wooden cases or as your requirement
|
|
Inner package
|
Stretch waterproof film & Each Mold painted, anti-rust oil.3. Spare parts together with the mold shipment. 4. Vaccum package
|
###
| Q1: What is your company’s main product? |
| A: Our company is specialized in injection molding moulds and injection plastic products. We can customize all kinds of injection plastic products according to your requirements or 3D drawing. |
| |
| Q2: How can I get the samples to check the quality? |
| A: 1) You can come to have the mould test directly. 2) We could send samples & mould running video to you. |
| |
| Q3: Can you make multi-cavity molds? |
| A: Yes, we are capable of making molds in 16, 24, 48, and 64 cavities. |
| |
| Q4: What certificates are you qualified for? |
| A: We are qualified in ISO9001, and we have a system for TS16949. |
| |
| Q5: How do you make our business a long-term and good relationship? |
| A:1. We keep good quality, on-time delivery, and competitive price to ensure our customers benefit from the best quality products 2. We value each customer, no matter where they come from, or how big the order they place. |
| |
| Q6: I have an idea for a new product, but don’t know if it can be manufactured. Can you help? |
| A: Yes! We are always happy to work with potential customers to evaluate the technical feasibility of your idea or design and we can advise on materials tooling and likely set-up costs. |
| Warranty: |
1 Year |
| Shaping Mode: |
Injection Mould |
| Surface Finish Process: |
Polishing |
| Mould Cavity: |
Multi Cavity |
| Plastic Material: |
ABS |
| Process Combination Type: |
Single-Process Mode |
###
###
###
| Item Name |
injection molding parts suppliers custom plastic electroplated injection molded |
|
Mould Core/Cavity
|
DIN2312,2738,2344,718,S136,8407,NAK80,SKD61,P20, P20HH, H13, 420ss etc.
|
|
Hardness of steel
|
33-38HRC prehard, 46~56 HRC hardened
|
|
Mould Standard
|
HASCO,DME,MEUSBURGER,JIS,CHINA LKM Standard
|
|
Mould Base
|
LKM&Hasco&DME standard (A,B plate 1730,2311,2312,1050,P20 )
|
|
Cavity
|
Single/Family/Multi
|
|
Runner
|
Hot/Cold Runner
|
|
Mould Size
|
150*150mm Min, 3000*2500mm Max
|
|
Surface of Mould
|
EDM VDI/ High Polish&Texture
|
|
Plastic material
|
PP, PC, PS, PE, PET, POM, PA, PU, PVC, ABS, HIPS, PMMA, Nylon, and with GF, etc.
|
|
Mould Life
|
Prototype 1000-25,000; preproduction 50,000-10,0000; High production 300,000-1,000,000 shots based on Volume requirements
|
|
Specification
|
Depends on the customer’s requirements.
|
|
Trade terms
|
FOB Shenzhen, EXW, CIF
|
|
Export to
|
Europe countries,USA,Mexico,Australia ,Middle-east ,Asia etc
|
|
Mold hot runner
|
DME, HASCO, YUDO, Mold-Masters, HRS, Synventive, etc, or per customer requirement
|
|
Mold gate type
|
point gate, side gate, sub gate, tunnel gate, banana gate, direct gate, tab gate, hot runner valve gate, hot runner to cold runner, etc.
|
|
Lead time 1st Trial
|
20-45Days based on different molds
|
|
Outside package
|
Standard wooden cases or as your requirement
|
|
Inner package
|
Stretch waterproof film & Each Mold painted, anti-rust oil.3. Spare parts together with the mold shipment. 4. Vaccum package
|
###
| Q1: What is your company’s main product? |
| A: Our company is specialized in injection molding moulds and injection plastic products. We can customize all kinds of injection plastic products according to your requirements or 3D drawing. |
| |
| Q2: How can I get the samples to check the quality? |
| A: 1) You can come to have the mould test directly. 2) We could send samples & mould running video to you. |
| |
| Q3: Can you make multi-cavity molds? |
| A: Yes, we are capable of making molds in 16, 24, 48, and 64 cavities. |
| |
| Q4: What certificates are you qualified for? |
| A: We are qualified in ISO9001, and we have a system for TS16949. |
| |
| Q5: How do you make our business a long-term and good relationship? |
| A:1. We keep good quality, on-time delivery, and competitive price to ensure our customers benefit from the best quality products 2. We value each customer, no matter where they come from, or how big the order they place. |
| |
| Q6: I have an idea for a new product, but don’t know if it can be manufactured. Can you help? |
| A: Yes! We are always happy to work with potential customers to evaluate the technical feasibility of your idea or design and we can advise on materials tooling and likely set-up costs. |
Factors to Consider When Converting a Design to Injection Molding
When considering injection molding for your design, there are several things you should consider. These factors include design, material selection, process, and reliability. In addition, you should consider the price of each part. The average cost per injection molded part is between $1 and $5. If you want to reduce your costs and improve your production cycle, look into converting your design to injection molding.
Design considerations for injection molded parts
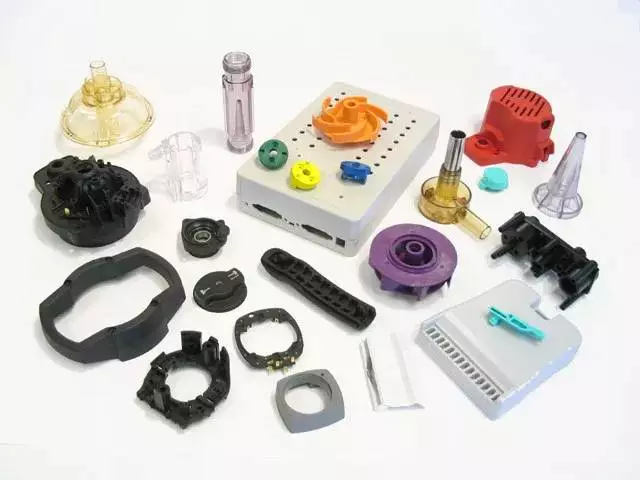 Injection molded parts must meet certain design considerations to ensure quality and precision. Design considerations include proper material choice, process control, and tool design. In addition, designers must consider the tolerance ranges for the parts to be produced. These tolerances will differ from molder to molder, and designers should discuss their specific needs with their molders before they begin production. Designers must also consider possible revisions to the mold, such as making the part more or less tighter.
When designing injection molded parts, the designer should consider the thickness of each wall. This will minimize stresses that may arise due to uneven wall thickness. Parts with uneven wall thickness can develop sink marks, voids, and molded-in stresses. This can result in longer production time and increased cost. Moreover, irregular wall thickness can restrict material flow. To minimize these problems, designers should make the transitions between the different thicknesses smooth.
Another important design consideration is the use of bosses in injection molded parts. Bosses are typically used as points of assembly and attachment in injection molded parts. Bosses are cylindrical projections with holes for threaded inserts and other fastening hardware. Injection molded parts with bosses are generally able to accommodate multiple threaded inserts without stripping. These inserts are also durable and enable several cycles of assembly.
The thickness of the walls is another important consideration when designing injection molded parts. The thickness of walls will determine many key characteristics of the part. Careful consideration of this feature will prevent expensive mold modifications and delays. The nominal wall thickness should be determined based on the functional requirements of the part. Likewise, the minimum wall thickness should be set based on acceptable stress. If the walls are too thin, air will collect between them and compromise the functional performance of the part.
Material selection
Selecting the right material for your injection molded parts is an important part of the process. While there are many options, there are also many factors to consider. For instance, what kind of end product are you producing? Whether it’s a consumer part for your home or a complex part for the aerospace industry, you’ll need the right material for the job.
There are literally hundreds or thousands of types of plastic materials available for injection molding. One of the most common types is ABS, a polymer that has a high degree of structural strength and low cost. Another popular choice is polycarbonate, which offers excellent heat resistance and transparency. Alternatively, you can opt for Ultem, a high performance plastic that’s commonly used in medical and aerospace applications.
The process of designing plastic products involves a combination of art and science. The goal of this process is to create a high-quality product that meets the expectations of consumers. By doing this, you’ll reduce production costs and increase profits. It’s not an easy process, but it’s well worth the effort.
Injection molding is an efficient and versatile method of manufacturing medical devices. It can be done in high volumes and with high flexibility. In addition to this, it also offers a broad range of materials. This is important when your parts need to be made of different materials with unique physical properties. For example, if you’re producing toys, you’ll want to use Acrylonitrile Butadiene Styrene (ABS). ABS is also a great option for medical applications because it can withstand the high temperatures and pressures of medical environments.
When choosing plastic injection molding materials, keep in mind the weight and stiffness of the material. Some applications require hard plastics, while others require softer materials. In addition, the material’s flexibility will determine how much you can bend it.
Process
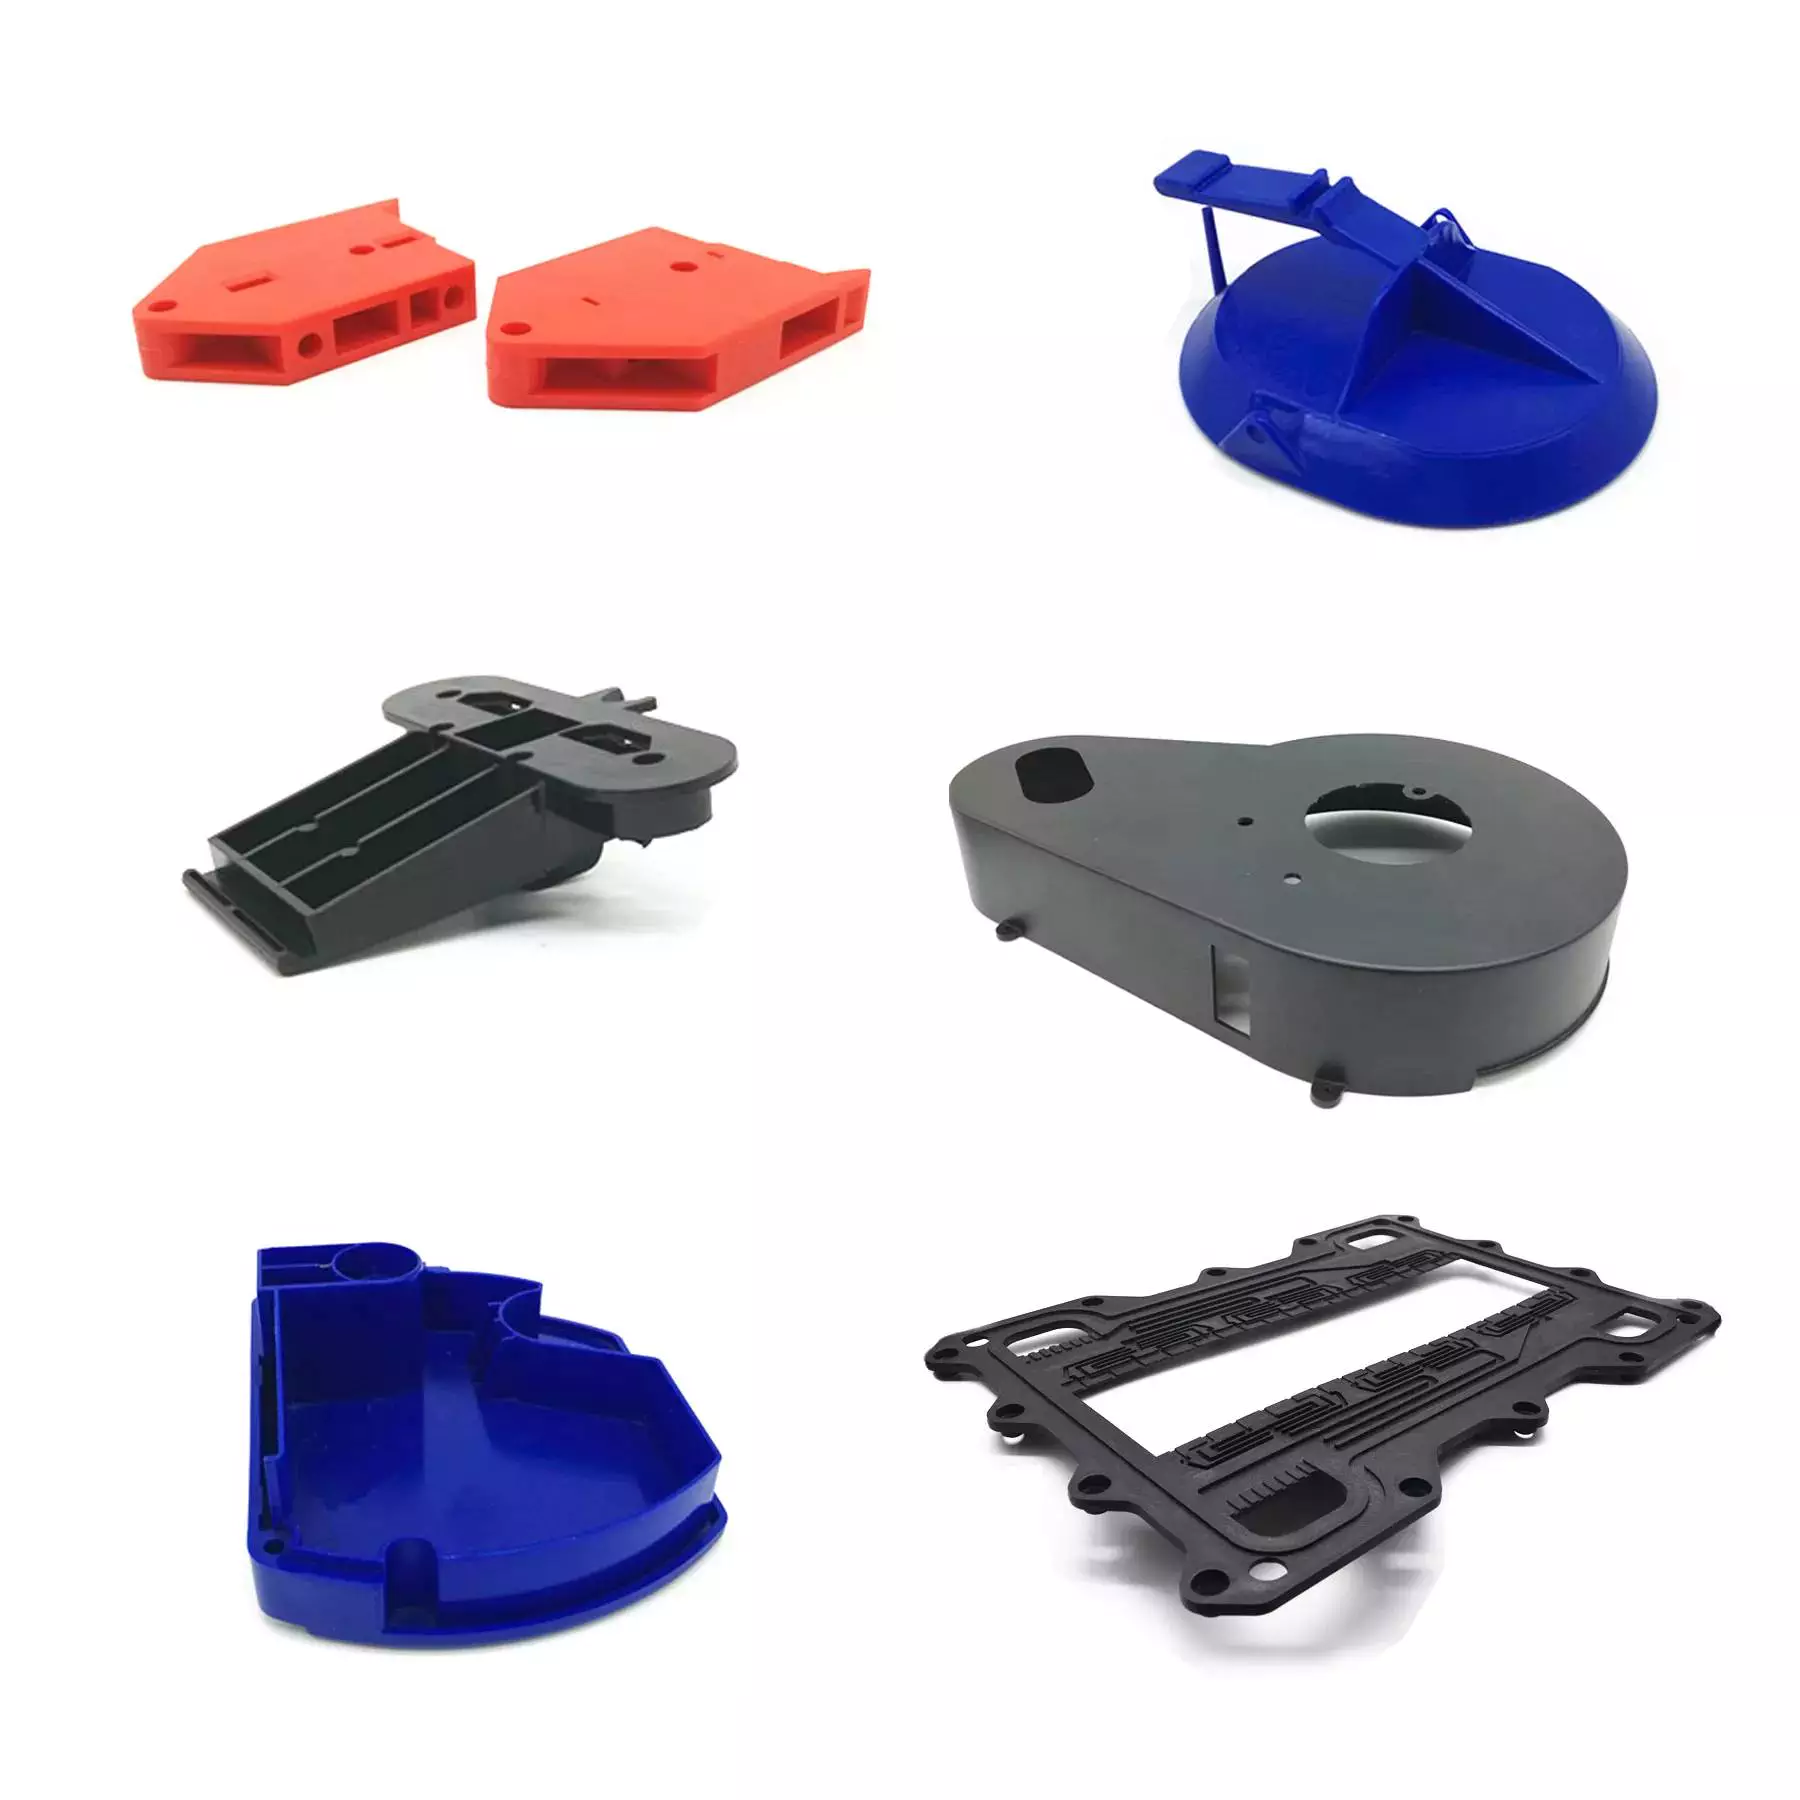 Injection molding is a process in which plastic parts are formed by pressing melt into a mold. The process takes place in two stages. During the first step, the material is injected and heated, while the second stage is when the mold is opened and the part ejected. The part is then finished and ready for use.
The material used in injection molding is made from a variety of polymers. Common polymers include nylon, elastomers, and thermoplastics. Since 1995, the number of materials used in injection molding has increased by 750 percent. Some materials are newly developed while others are alloys of previously-developed materials. The selection of material primarily depends on the strength and function required by the final part. Also, the cost of the material is a critical factor.
The design of custom components for the molding process should be carried out by a skilled industrial designer. There are a number of design guidelines for plastic parts, which should be followed carefully to achieve high quality and dimensional accuracy. Failure to follow these guidelines can lead to undesirable results. Therefore, it is crucial to specify specific requirements for the parts before the process begins.
The process is reliable and highly repeatable, making it ideal for large-scale production. Injection molding also allows for the creation of multi-cavity injection mold parts, which can create several parts in one cycle. Other advantages of the injection molding process include low labor costs, minimal scrap losses, and low post-mold finishing costs.
Before beginning the full production run, technicians perform a trial run. In this test, they insert a small shot weight in the mould. Then, they apply a small holding pressure and increase the holding time until the gate freezes. Then, they weigh the part to check if it is right.
Reliability
Injection-molded parts are subject to a variety of defects. One of the most common is unwanted deformation. This may happen when the temperature of the mold is too high or there is not enough plastic injected into the mold. Another problem is millidiopter range distortion. This distortion is invisible to the naked eye, and cannot be detected by manual inspection. Regardless of the cause, preventing unwanted deformations is critical for the long-term performance of the part.
The process of creating a custom mould for a plastic component requires great skill. Creating a mould that is perfectly suited to the product is important, because a good mould is crucial in avoiding potential defects. Traditionally, this process relied on the skill of a toolmaker and trial-and-error methods. This slows down the process and increases the cost of production.
Another factor contributing to injection molded parts’ reliability is the high level of repeatability. Injection molding is ideal for high volume production, because parts are easily re-molded. However, the process can be prone to failure if there is no quality control. While most injection-molded parts will last for a long time, parts that are prone to wear will eventually fail.
Besides high level of consistency and reliability, injection-molded parts are also eco-friendly. Unlike other manufacturing methods, the injection molding process produces little to no waste. Much of the plastic left behind in the process can be recycled, making it a green alternative. Another benefit of this manufacturing method is automation, which helps reduce production costs. Overall, injection molding is a highly reliable and consistent product.
Injection molding requires precise measurements and a 3-D model. It is also important to check for wall uniformity and draft angles. Properly-designed parts can avoid deformations. If the wall thickness is too low, support ribs can be used. Proper draft angles are important to ensure that the part can be removed easily from the mold.
Cost
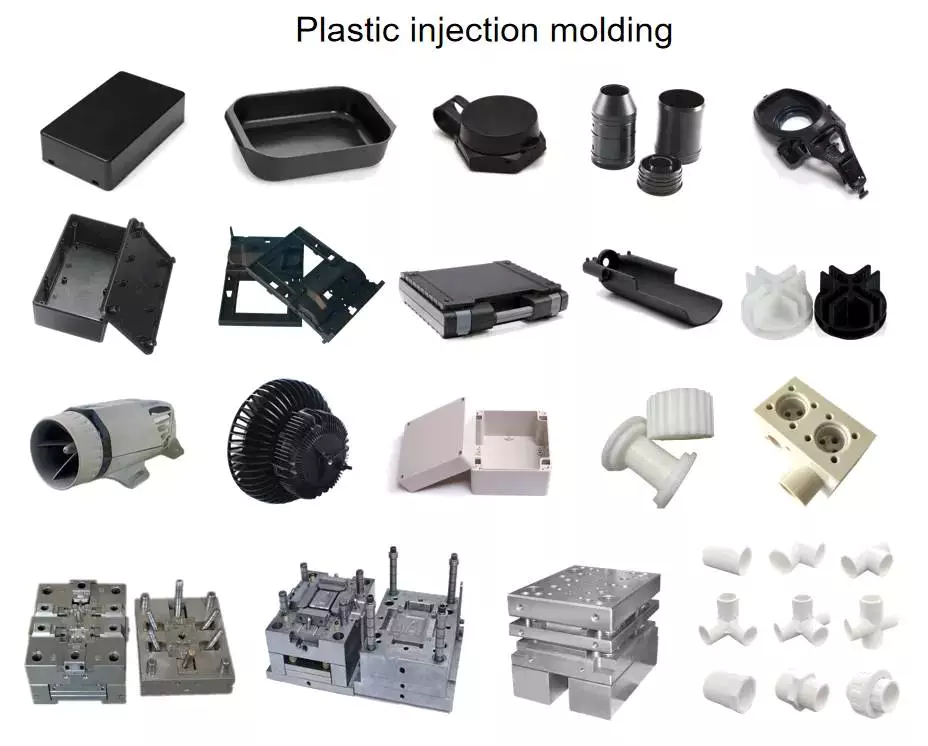 The cost of injection molded parts depends on many factors, including the complexity of the part and the mold design. Simpler designs, fewer CAD steps and simpler processes can help companies minimize costs. Another factor that affects the cost of injection molded parts is the geometry of the part. In general, complex geometries require more design work and tooling time. Additionally, thicker walls require more material than thin ones, which raises the cost of the part.
The amount of plastic used in the mold is also a key factor. Injection molding requires large quantities of material, so parts that are larger will require a larger mold. Larger parts are also more complex, so these require more detailed molds. A mold maker will be able to advise you on how to design your part to cut down on costs.
The next major factor affecting the cost of injection molded parts is the material of the mold. Most injection molds are made of steel, but the type and grade of steel used is important. Additionally, tight tolerances require molds with virtually wear-free interior cavities. Hence, higher-grade steel is required.
Another factor affecting the cost of injection molded parts is the price of mold tools. Depending on the size and complexity of the part, the cost of molding tools can vary from $10,000 to several hundred thousand dollars. Injection molding tooling is an integral part of the entire process and can add up to a significant portion of the overall cost of the part.
Draft angles are another factor that affects the cost of injection molded parts. A draft is an important design element as it allows for easy part separation and removal from the mold. Without a draft, it would be very difficult to remove a part after injection.
editor by czh 2022-12-31
China PC PP ABS PA66 Plastic Injection Mold Plastic Molded Products Plastic Mould Injection with Great quality
Item Description
Mold and precision molding processing are our core enterprise. When you select Jingsheng, you will get a
professional associate in the complete creation approach to carry your merchandise from notion to fact.
one. We give consumers with a single-cease providers for mildew/ plastic components/ hardware parts
die castings /cnc numerical management processing, which includes mould flow, component design and style, mould
design and style, mould producing and molding.
2. Our team has 20 years of business experience.
three. We have an superb quality inspection group to defend the high quality of merchandise.
HangZhou Jingsheng Electronic Technology Co., Ltd., started in 2012, is a production organization integrating
product advancement and design, mold manufacturing, injection molding, die-casting molding, stamping molding
and CNC processing.The firm covers an area of more than 6000 sq. meters, with a lot more than sixty R&D,
design, manufacturing and quality inspection personnel,and more than thirty advanced superior equipment.
The organization actively encourages and operates the ISO9001:2015 high quality administration method, pursuing the
theory of “becoming earnest and pragmatic, status 1st, quality very first”. Our objective is to allow consumers appreciate the
best top quality and services at the most reasonable value!
The injection Molding, metallic stamping, sheet metal processing, machining factories are ceritificated by
ISO 9001, IATF16949. Silicone Molding and Injection molding certificated by ISO13485
Q1: Can I get cost-free samples and how lengthy will it get?
A1: For the regular merchandise we have in stock, we can supply samples free of charge of demand, and the categorical price is borne
by the customer.
For custom-made goods, the sample price is decided in accordance to the merchandise specifications. It normally requires about 7 times
to deliver it.
Q2: Can you personalize parts in accordance to my samples or drawings?
A2:Sure,you can ship us drawings on the internet or by e-mail , or send out us samples. We will scan the features according to the drawings
or samples and attract 3D drawings for manufacturing.
Q3: What is the delivery time?
A3: twenty five-35 days soon after confirming the item drawing and acquiring the progress payment, the specific shipping and delivery time is dependent
on the merchandise and quantity you purchased
This autumn: What does your OEM provider include?
A4: We follow your specifications from layout idea to mass creation. You can provide us with 3D drawings, and then
our engineers and manufacturing staff consider the design and make recommendations on item modeling/ manufacturing
B. If you never have 3D drawings, you can give 2d drawings or sketches with complete-scale characteristic details. We can draft 3D
drawings for you at a realistic cost.
C. You can also customize the emblem on the item area packaging and cartons.
D. We also supply assembly services for OEM components
Q5: What is your payment expression?
A5: we accept paypal, credit history card, Westen Union remittance and other on the web payments. For typical orders, the payment tems
are thirty% deposit and full payment ahead of cargo.
Q6: Are you a manufactureror factory or a trading business?
A6: We are a producing manufacturing facility.Welcome to go to our manufacturing facility at any time.
US $0.38-1.6
/ Piece
|
|
1,000 Pieces
(Min. Order)
|
###
| Material: |
ABS+PC PP PC ABS PA HIPS PVC PE PS POM etc |
| Application: |
Household, Electronics, Automotive |
| Certification: |
TS16949, RoHS, ISO |
| Mold Material: |
S136 718h 738h Nak80 8407 DC53 SKD61 Fdac P20 |
| Mold Life Time: |
1 Million Times |
| Mould Cavity: |
Single Cavity, Multi-Cavity |
###
US $0.38-1.6
/ Piece
|
|
1,000 Pieces
(Min. Order)
|
###
| Material: |
ABS+PC PP PC ABS PA HIPS PVC PE PS POM etc |
| Application: |
Household, Electronics, Automotive |
| Certification: |
TS16949, RoHS, ISO |
| Mold Material: |
S136 718h 738h Nak80 8407 DC53 SKD61 Fdac P20 |
| Mold Life Time: |
1 Million Times |
| Mould Cavity: |
Single Cavity, Multi-Cavity |
###
Injection Molded Parts – Design Considerations
If you want to produce high-quality Injection molded parts, there are several factors to consider before the design process. These factors include the Surface finish, Material compatibility, and Tooling fabrication. This article will focus on some of these factors. Ultimately, you can save time and money by designing the parts in-house.
Design considerations
When creating a new part, or updating an existing part, design considerations for injection molded parts are critical. The decisions you make in these early stages of development can have a profound effect on the final product, and they can also have substantial cost and timing implications. In this guide, we’ll explore key design considerations, including how to maximize the efficiency of the injection molding process. We’ll also touch on how to optimize gate placement and parting lines.
To ensure a successful injection molding process, part design must balance structural integrity and plastic fill volume. This means creating parts with relatively thin walls that have adequate support and avoid warping or sinking. To do this, injection molded parts often feature ribs or projections to strengthen the walls. However, too thin of a wall can result in excessive plastic pressure and air traps.
One of the most important design considerations for injection molded parts is the direction of the parting line. For many applications, a parting line is obvious, but for others it’s a little less obvious. The first step in designing an injection mold is to determine which direction it should open.
Another critical design consideration is the part’s ejection. If a part isn’t ejected properly, it will stick to the mold. A part that has too many undercuts or ribs will end up stuck on the mold’s side, making it difficult to eject it from the mold. A part that has a draft angle of at least five degrees is much easier to eject.
Another important design consideration for an injection molded part is the type of plastic used. Some plastics do not tolerate undercuts. However, some materials are able to tolerate undercuts of up to five percent. Undercuts are not ideal and can increase the complexity and cost of the injection mold.
Another design consideration for injection molded parts is the radius of edges. Sharp corners can create high molded-in stresses and can lead to failure points. A radius eliminates this stress by redistributing the stress more evenly throughout the part. This also facilitates flow of the material through the mold.
Surface finish
Injection molded parts are often finished with additional processing in order to improve their aesthetic quality. There are a variety of finishing processes, including machining and sanding, which give injected molded parts a particular look, feel, or texture. The surface finish of a plastic part affects both its aesthetics and its functionality. According to the Society of Plastics Industry, certain standards for surface finish are essential to the aesthetics and durability of plastic parts.
Surface finish of injection molded parts depends on the primary design goal. For instance, some designs may need a part to be aesthetically pleasing while others may want to enhance its functionality. Surface texture is often used by designers and engineers to achieve different aesthetic goals, such as improving the product’s perceived value. A textured surface may also help hide imperfections and improve the part’s non-slip qualities.
Surface finish is a critical aspect of plastic injection molding. It can affect material selection, tooling, and other process decisions. It is important to determine the desired surface finish early in the design phase. A skilled plastic injection molder can assist you in making this decision. In addition to determining the finish you need, a skilled molder can help you decide the best material for the job.
The PIA classification system defines four basic grades for surface finish. There are subcategories for each grade. Group A surface finish is smooth, and grade B and C finishes are textured. The former is the most common and economical finish and is most suitable for industrial parts. It can hide deformations and tooling marks, and is the least expensive finish type.
Surface finish of injection molded parts can vary greatly, and can be crucial to the performance and appearance of the part. Some companies prefer plastic parts with a glossy finish, while others prefer a textured surface for aesthetic reasons. While the former may be better for aesthetic purposes, rougher surfaces are often preferred for functional or mechanical parts.
Material compatibility
Material compatibility is important for the durability of your injection molded parts. You can use multiple materials in the same part by mixing resins. This is an ideal solution for parts that require adhesion, friction, or wear. Fast Radius can simplify the material selection process, optimize part design, and speed up production.
ABS is a thermoplastic polymer that can withstand a range of temperatures. Its low melting point means that it is easy to mold, and it has good chemical and moisture resistance. ABS also has good impact strength, and is highly durable. It is easy to recycle. Nylon is another versatile material for injection molding. It can be used for car tires, electrical components, and various apparel.
When choosing the material for your injection molded parts, keep in mind that the type of resin will determine their tolerance. Injection molding is compatible with a wide range of plastic resins. Some materials are more suitable than others for certain applications, and many plastics can be modified with stabilizers or additives to improve their properties. This flexibility allows the product development team to customize materials to achieve the performance characteristics they desire.
Polyamides are another great option for injection molding parts. Both natural and synthetic varieties of these plastics have excellent properties. However, they have some drawbacks. For instance, nylon injection molding is difficult and can result in inadequate filling. However, Nylon injection molding has many benefits, including high impact resistance and heat resistance.
Polybutylene terephthalate (PBT) is a high-molecular-weight polymer with excellent mechanical and chemical resistance. It is a good choice for components in the medical, automotive, and lighting industries. Its low water absorption and low flammability make it suitable for many applications.
Polyurethane (TPU) is another polymer option. It has excellent resistance to abrasion, chemicals, greases, and oils. It also has high temperature resistance, and is suitable for ozone environments. However, TPU is more expensive than TPE and requires drying before processing. Moreover, it has a short shelf life.
Tooling fabrication
Tooling fabrication for injection-molded parts is an important component of the manufacturing process. The right design of the mold can reduce the cost and time required for a finished product. For instance, choosing the right type of core for the mold can reduce the amount of material used in the part, which is necessary to produce a high-quality product. It is also important to choose a design that is easy to mill into a mold.
Injection molding requires a mold with precise geometries. The mold tool must be constructed accurately and carefully to achieve the desired precision. It can be the biggest investment in the manufacturing process, but it is also critical to the success of a project. Large volume and high-precision parts often require more complex tooling, as they require the highest level of precision.
Tool steels typically used for injection moulding include H-13 and 420 stainless steel. Both of these materials are strong enough to produce parts of comparable hardness to wrought parts. These materials have low elongation values, so they are ideal for constructing injection moulding tools. Some of these steels also have excellent dimensional accuracy and are ideally suited for high-precision tool fabrication.
The process of plastic injection molding requires precise measuring and tooling fabrication. The mold must have the proper lead angle and space for the material to deform. Undercuts must be no larger than 5% of the diameter. Moreover, the injection molded part should be free of stripping or undercuts. Ideally, it should have a lead angle of 30o to 45o.
Various plastics can be used in the process of injection molding. The process can be used to produce cosmetic and end-use parts. Materials used in the molding process include silicone rubber and thermoplastics. If the part requires additional reinforcement, it can be reinforced with fibers, mineral particles, or flame retardant agents.
Increasingly advanced technologies have streamlined the process of tooling fabrication for injection moulded parts. The process has improved with the use of computer aided design, additive manufacturing, and CNC lathes. Approximately 15% of the cost of a finished injection molded part is spent on tooling fabrication.
editor by czh 2022-12-30
China Fpic Designed and Made in China Injection Moulding Plastic Parts OEM Plastic Injection for Automobile wholesaler
Solution Description
High Top quality OEM Aluminum Brass Stainless Steel Sheet Metal Stamping Components Vehicle areas
In Forman,you can locate different exiting connectors and also we can provide you the tailored merchandise,not only the plastic injection companies but also the metallic stamping(sheet metal) companies.In accordance to your necessity,our staff will offer you the most aggressive resolution and offer you the greatest overall performance.
Product Description
| Solution Name |
Auto Parts |
| Raw Materials |
PA66,PA6T,PA9T,PBT,LCP+Brass , Custom-made |
| แอปพลิเคชัน |
Automotive Connector,Electrical Connector |
| Color |
White ,Black, Grey, Personalized |
| R&D Capacity |
fourteen menbers weathy encounter R&D crew ,Layout composition and Open up New moulds according to your requirement |
| Deal |
PE bag/ Tray /tape& Reel with lable in export common Carton |
| Our Potential |
Entire-Automobile Creation Line for plastic injection,metal stamping and assembly companies,also the CCD inspection, |
| Our Max. Stamping Machine Tons. |
200 Tons. |
| Our Max Injection Machine Tons |
300 Tons |
| Our Manufacturing Cycels |
21 functioning times for the new CZPT and in 7 doing work times for exiting model(Relies upon on the QTY) |
| Our Certificate |
ISO9001:2015ISO14001:2015IATF16949:2016 |
| Top quality Assurance |
one hundred% CCD inspection and QC location examine for each 2 several hours. |
OEM stamping spare Parts
Company Profile
HangZhou Forman Precision Market Co.,Ltd has been committing to electronic component manufacture since 1999 with strong R&D and Complete-Vehicle manufacturing capacity.Forman supply a assortment of USB connectors,Pin Header,FPC,Wafer,Automotive Components and customized services.
After 20 several years advancement that Forman has handed ISO9001,ISO14000 and TS 16949 and become the member o f USB Affiliate. And we are very pleased of our progress, because our merchandise are extensively employed in many worldwide manufacturers and our quality is authorized dependent on scientific TQM system.
FPIC insists on introducing advantaged facility to improve our capacity from creation and top quality assurance,its in get to incorporate customer value and improve our competitiveness. We warmly welcome your enquiry,Forman will be your most ideal and recognize partner.
Manufacturing facility workshop
Manufacturing Process
Exiting Items: Inquiry with your necessity/drawing – Provide you our most suitable merchandise / Modify the structure based mostly on our exiting model – Ship the free of charge sample – validate the sample – Area the order – Deposit – Start Production – Offer files before shipment – Arrange the remainder payment – Shipping and delivery
New Goods: Inquiry with your drawing / requirement – Supply you our most aggressive cost – validate the construction and CZPT order – CZPT deposit – Complete the sample and take a look at – Sample delivery – Sample validate – Set up the remainder CZPT price – Location buy – Provide related paperwork just before shipment – Arrange the remainder expense – Delivery
High quality Assurance
Certifications
Honor From Client
FAQ
Q: Are you trading organization or company?
A: We are factory, so we can supply aggressive price for you.
Q: What type of items can you offer?
A: Our organization (FPIC) can provide OEM/ODM spare parts. We are an knowledgeable OEM / ODM company, concentrating on tooling and mass production of Stamping elements, Injection-molded plastic components and Insert-molding parts .
Q: What is varieties of details you require for a estimate?
A: In purchase to quotation for you earlier, remember to provide us the details collectively with your inquiry.
one. 3D drawings (Phase, CAD, Sound Operates, PROE, DXF and PDF)
2. Content necessity (include get in touch with material and insulation materials.)
three. Floor treatment method
four. Quantity or Intake (for each get/ for every month/ yearly)
5. Any special needs or demands, this kind of as packing, labels, shipping and delivery, etc.
Q: What shall we do if we do not have drawings?
A: Remember to send out your sample to our factory, then we can copy or supply you better remedies. Remember to deliver us images or drafts with proportions (Thickness, Duration, Top, Width), CAD or 3D file will be produced for you if put buy.
Q: What tends to make you different from others?
A.1. Our know-how R&D group with 14 member who all have prosperous specialist information and expertise about connectors
two. Automated generation tools and matched good quality testing equipment.
Q: Is it attainable to know how are my products heading on without having checking out your organization?
A: We will offer you a in depth generation routine and send weekly studies with pictures or films which demonstrate the machining progress.
Q: Can I have a trial order or samples only for numerous items?
A: As the solution is tailored and want to be made, we will cost sample price, but if the sample is not a lot more costly, we
will refund the sample expense soon after you placed mass orders.
Thanks FOR YOUR Individual Reading AND KINDLY Contact US FOR Timely Companies.
US $0.01-0.8
/ Piece
|
|
1,000 Pieces
(Min. Order)
|
###
| Type: |
Car Power Inverter |
| Certification: |
ISO9001, RoHS, Reach |
| Our Services: |
Plastic Injection + Metal Stamping |
| Metal Material: |
Copper,Brass,Iron,Steel,etc. |
| Plastic Material: |
PBT,LCP,Nylon,etc. |
| Feature: |
Mould Manufacture,Plastic Injection,Steel Stamping |
###
###
###
| Product Name |
Auto Parts |
| Raw Material |
PA66,PA6T,PA9T,PBT,LCP+Brass , Customized |
| แอปพลิเคชัน |
Automotive Connector,Electrical Connector |
| Color |
White ,Black, Gray, Customized |
| R&D Ability |
14 menbers weathy experience R&D team ,Design structure and Open New moulds according to your requirement |
| Package |
PE bag/ Tray /tape& Reel with lable in export standard Carton |
| Our Capacity |
Full-Auto Production Line for plastic injection,metal stamping and assembly services,also the CCD inspection, |
| Our Max. Stamping Machine Tons. |
200 Tons. |
| Our Max Injection Machine Tons |
300 Tons |
| Our Production Cycels |
21 working days for the new mould and within 7 working days for exiting model(Depends on the QTY) |
| Our Certificate |
ISO9001:2015;ISO14001:2015;IATF16949:2016 |
| Quality Assurance |
100% CCD inspection and QC spot check per 2 hours. |
US $0.01-0.8
/ Piece
|
|
1,000 Pieces
(Min. Order)
|
###
| Type: |
Car Power Inverter |
| Certification: |
ISO9001, RoHS, Reach |
| Our Services: |
Plastic Injection + Metal Stamping |
| Metal Material: |
Copper,Brass,Iron,Steel,etc. |
| Plastic Material: |
PBT,LCP,Nylon,etc. |
| Feature: |
Mould Manufacture,Plastic Injection,Steel Stamping |
###
###
###
| Product Name |
Auto Parts |
| Raw Material |
PA66,PA6T,PA9T,PBT,LCP+Brass , Customized |
| แอปพลิเคชัน |
Automotive Connector,Electrical Connector |
| Color |
White ,Black, Gray, Customized |
| R&D Ability |
14 menbers weathy experience R&D team ,Design structure and Open New moulds according to your requirement |
| Package |
PE bag/ Tray /tape& Reel with lable in export standard Carton |
| Our Capacity |
Full-Auto Production Line for plastic injection,metal stamping and assembly services,also the CCD inspection, |
| Our Max. Stamping Machine Tons. |
200 Tons. |
| Our Max Injection Machine Tons |
300 Tons |
| Our Production Cycels |
21 working days for the new mould and within 7 working days for exiting model(Depends on the QTY) |
| Our Certificate |
ISO9001:2015;ISO14001:2015;IATF16949:2016 |
| Quality Assurance |
100% CCD inspection and QC spot check per 2 hours. |
What Is Injection Moulding?
Injection molding is a process of producing precision-molded parts by fusing raw plastics and guiding them into a mold. The main components of an injection mold are a hopper, barrel, and reciprocating screw. Before injection, the raw plastics are mixed with coloring pigments and reinforcing additives.
Characteristics of injection molded parts
 Injection molding is the process of manufacturing plastic parts. It uses thermoplastic, thermoset, or elastomers to manufacture components. The range of materials is enormous and includes tens of thousands of different polymers. They are blended with other materials and alloys to produce a wide range of properties. Designers select the appropriate materials for the job based on the properties and functions desired in the finished part. During the mold design process, mold materials must be carefully chosen, as different materials require different molding parameters.
Injection molding requires precise tolerances of the temperature and strain levels. The maximum strain level is about 0.15 percent. It is possible to adjust these parameters to meet the requirements of an injection molding project. The resulting products can be easily checked for quality by measuring the strain and temperature of the mold inserts in real time.
Injection molding is known for its laminar flow of the polymer. However, there is still a possibility for side-to-side thermal variations in the part forming cavity. This is illustrated in FIG. 4. The part has high and low sheared areas; the higher sheared areas flow on the bottom side of the part, while the lower sheared areas flow on the top side.
Injection molding is used to make many different types of plastic parts, from small parts to entire body panels of a car. These parts can be made from a variety of different materials, such as polypropylene for toys and ABS for consumer electronics. They can also be made from metal, such as aluminum or steel.
The melting temperature of plastic parts must be appropriate for the project’s specifications. The mold should be large enough to produce the parts desired. This will minimize the impact of uneven shrinkage on the product’s dimensional accuracy. In addition to the temperature, a mold must be designed with the material’s properties in mind.
Tooling fabrication
Injection molded parts are produced using molds. This process is a complex process that requires customization to ensure proper fit and function. The main component of a mold is the base, which holds the cavities, ejectors and cooling lines. The size and position of these components are crucial to the production of quality parts. Incorrectly sized vents can cause trapped air to enter the part during the molding process. This can lead to gas bubbles, burn marks, and poor part quality.
The material used for tooling fabrication is usually H-13 tool steel. This steel is suitable for injection molded parts as it has a low elongation value. The material used to fabricate tooling for injection molded parts typically has a high yield strength. The material used for injection moulding tooling is typically 420 stainless steel or H-13 tool steel. These materials are suitable for most injection molding processes and have comparable yield strength compared to wrought or MIM parts.
Another important part of tooling fabrication is the design of the mold. It is important to design the mold with a draft angle, as this will make ejection easier and reduce costs. A draft angle of 5o is recommended when designing a tall feature. Choosing a draft angle is essential to ensuring that the plastic part is free from air bubbles after injection molding.
Injection moulding tooling costs can account for as much as 15% of the cost of an injection moulded part. With innovation in mould materials and design, tooling fabrication can be more efficient and cost-effective.
Surface finishes on injection molded parts
Surface finishes on injection molded parts can have a variety of effects on the part’s appearance and performance. Different materials lend themselves to different kinds of surface finishes, with some plastics better suited for smooth, glossy finishes than others. The type of surface finish is also affected by several factors, including the speed of injection and the melt temperature. Faster injection speeds help improve the quality of plastic finishes by decreasing the visibility of weld lines and improving the overall appearance of the parts.
For a smooth plastic surface finish, some companies require a high level of roughness on the part. Others may prefer a more rough look, but both options can have their benefits. The type of surface finish chosen will depend on the part’s purpose and intended application. For example, a glossy plastic finish may be preferred for a cosmetic part, while a rougher finish may be better suited for a mechanical part that must be tough and cost-effective.
Surface finishes on injection molded parts are often customized to match the application. For example, some parts require a rough surface finish because they require a greater amount of friction. These parts may require a sandblasting process to achieve the desired texture. Other processes can also be used to control plastic texture.
The type of surface finish depends on the materials used, as well as the design and shape of the part. The type of material used, additives, and temperature also have an impact on the surface finish. It is also important to consider surface finishes early in the design process.
Importance of a secondary operation to improve accuracy
While most injection molded parts do not require secondary operations, some components do require this type of processing. The surface finish of a component will determine how well it functions and what other secondary operations are necessary. Depending on the part’s function, a smooth or textured surface may be appropriate. Additionally, some parts may require surface preparation before applying adhesives, so an accurate surface finish can make all the difference. In order to achieve the desired finish, the injection molder should have experience molding different materials. He or she should also have the knowledge of how to simulate the flow of a mold. Also, experienced molders know how to mix materials to achieve the desired color, avoiding the need for secondary painting processes.
Injection molding is a complex process that requires precision and accuracy. The optimal temperature of the melted plastic must be chosen, as well as the mold itself. The mold must also be designed for the correct flow of plastic. In addition, it must be made of the best thermoplastic material for the part’s design. Finally, the correct time must be allowed for the part to be solid before it is ejected. Many of these issues can be overcome with specialized tooling that is customized to the part’s design.
Injection molding offers the opportunity to make complex parts at low cost. It also allows manufacturers to make parts with complicated geometries and multiple functions.
editor by czh 2022-12-29
China OEM Precision Customized Production, High-Precision Mold Parts Customization, Various Types of Precision Bottle Cap Mold Parts Customization roto mold vs injection mold
Merchandise Description
OEM precision personalized manufacturing, higher-precision mildew elements customization, different types of precision bottle cap mold areas customization
SENLAN concentrate on mold components processing for ten years. With seasoned manufacturing and processing crew, full generation gear and testing gear, a range of components one particular-cease customization. It has accrued wealthy expert encounter in mold parts manufacturing,technologies, marketing and advertising and services, and has been regarded and supported by numerous clients at house and overseas. Products are primarily offered to Germany, the United States, Japan, Italy, Singapore, Thailand, Malaysia and other international locations and locations. High quality and service are confirmed. Strict management of item processing method, layers of high quality inspection, emphasis on every single method, do every single detail, integrity management, mutual reward.
Comprehensive Merchandise Description
| Mould: |
Plastic Injection Mould |
Content: |
1.2083,STAVAX |
| Tolerance: |
+/-.005 |
Surface Treatment: |
Polish |
| Normal: |
MISUMI/HASCO/DME/PUNCH |
Processing: |
CNC/EDM/W-EDM |
| Large Light: |
best quilty Bottle Cap Mould.Everyday Packaging Bottle Cap Mould. |
Solution Description
| Content |
STAVAX/1.2083
|
| Hardness |
forty eight-52HRC |
| Warmth treatment method |
Offered |
| Services |
Created-to-get |
| Area therapy |
/ |
| Closest tolerance |
+ – .002mm |
| Polishness |
Ra0.six |
| Axiality |
.005mm |
| Verticality |
.005mm |
Firm Profile
HangZhou Xihu (West Lake) Dis.g Mould Parts Co., Ltd is set up in 2008, is a expert producer of precision CZPT areas. Our factory, situated in the CZPT town–Chang’an. It is a expert business in study, growth and producing of precision CZPT components,we have more than ten years knowledge in this field,our sophisticated precision gear and scientific quality handle assures buyers pleasure.
Equipment & Equipments
- CNC machining middle CNC milling equipment ,CNC lathe equipment
- Sodick EDM,Sodick Wire-slicing
- OD Grinding,ID Grinding,Surface grinding device
Our Support
one. Customer’s ask for is our purpose and goal.
2. Fast samples supply service and make in accordance to your BOM.
three. Professional manufacturing crew, strictly top quality handle office, seasoned sales section.
four. 1-stop solution for our extended expression buyers .
five. Custom-made measurement and OEM/ODM support satisfactory.
6. 100% inspect ahead of provide , good quality warranty and long term following-services .
seven. Competitive cost ,Outstanding services , Quick shipping , Basic safety payment , Flexible trade conditions.
Why select us
- We as a producer are specialised in all types of precsion main pins cavity pins insert pins
- Excellent experience of 8 a long time to make Stamping die components,Injection die elements,Vehicle components, metal-doing work goods.
- Have superior creation equipments and seasoned operators.
- Great expertise of OEM and ODM for our customers.
- Provide greatest price tag, excellent good quality and quick shipping.
Major products
one.Main pin,cavity pin,insert pin and so forth
2.HSS punch ,Precision punch ,Unique-formed punch
3.Ejector pins,ejector sleeve,two-stage ejector pins and so on
four.Xihu (West Lake) Dis. pillars ,Xihu (West Lake) Dis. bushings ,Xihu (West Lake) Dis. put up established
five.Slide Main Models,Latch locks,finding Collection
Good quality Management
XIHU (WEST LAKE) DIS.G has rigorous top quality handle technique from the raw content incoming to completed merchandise outgoing. Our CZPT parts are assured high precision,large polished and prolonged service lifestyle.
Under are our main good quality inspection objects in the total production process:
Materials incoming: 100% inspection
Tough Finished:a hundred% inspetion
Warmth therapy: random inspection
Face grinding: a hundred% inspection
Middle-less cylindrical grinding: a hundred% inspection
OD/ID grinding: a hundred% inspection
EDM:one hundred% inspection
Wire-Chopping:one hundred% inspection
Packing: the ultimate 100% inspection ahead of the formal shipment
Packaging & Shipping and delivery
Package
Coated with anticorrosive oil, packed in carton box
Delivery
Delivery time is normally 7-15 operating times for sort of ejector pin, particular time is according to amount.
Shipping
We ship utilizing specific these kinds of as DHL, UPS, FEDEX and many others. or in accordance to customer’s prerequisite . It requires about 3-5 days to get there your entrance door, and evidence of shippments are supplied with a delivery or tracking number. And we ship by occean shippment for larger amount items, it will be financial for clients.
FAQ
Q:Are you trading firm or manufacturer?
A:We are manufacturing facility.
Q:How prolonged is your delivery time?
A: Normally it is ten-20 days if the items are not in stock, it is according to quantity.
Q:What is your quotation components?
A:Product common: model + measurement, or buyer Drawing.
Q:How can you ensure the quality?
A:We have QC division to manage the good quality from the begining of manufacturing till items end.
Q:If you make poor top quality merchandise,will you refund our fund?
A:As a issue of fact, we wont just take a opportunity to do inadequate high quality merchandise. Meanwhile, we manufacture items high quality products until finally your fulfillment.
Q. Do you check all your products before shipping and delivery?
A: Of course, we have one hundred% QC examination and QC report for mildew elements just before shipping and delivery.
Q. Can you produce according to the samples or drawings?
A: Sure, we can create components by your samples or technological drawings
Our enthusiastic and helpful customer services reps are all set to support with any queries or troubles. If you are interested in any goods or our firm, please come to feel cost-free to get in touch with us nowadays.
| After-sales Service: |
From Payment to Delivery, We Guarantee Your Tradi |
| Warranty: |
One Year |
| Type: |
Plastic Mould Parts |
| Material: |
1.2083/Stavax |
| Application: |
Electronic, Hardware, Machinery, Daily Use, Furniture, Household Applicances, Car |
| Certification: |
ISO9001 |
###
###
| Mould: |
Plastic Injection Mould |
Material: |
1.2083,STAVAX |
| Tolerance: |
+/-0.005 |
Surface Treatment: |
Polish |
| Standard: |
MISUMI/HASCO/DME/PUNCH |
Processing: |
CNC/EDM/W-EDM |
| High Light: |
best quilty Bottle Cap Mould.Daily Packaging Bottle Cap Mould. |
###
| วัสดุ |
STAVAX/1.2083
|
| Hardness |
48-52HRC |
| Heat treatment |
Available |
| บริการ |
Made-to-order |
| Surface treatment |
/ |
| Closest tolerance |
+ – 0.002mm |
| Polishness |
Ra0.6 |
| Axiality |
0.005mm |
| Verticality |
0.005mm |
| After-sales Service: |
From Payment to Delivery, We Guarantee Your Tradi |
| Warranty: |
One Year |
| Type: |
Plastic Mould Parts |
| Material: |
1.2083/Stavax |
| Application: |
Electronic, Hardware, Machinery, Daily Use, Furniture, Household Applicances, Car |
| Certification: |
ISO9001 |
###
###
| Mould: |
Plastic Injection Mould |
Material: |
1.2083,STAVAX |
| Tolerance: |
+/-0.005 |
Surface Treatment: |
Polish |
| Standard: |
MISUMI/HASCO/DME/PUNCH |
Processing: |
CNC/EDM/W-EDM |
| High Light: |
best quilty Bottle Cap Mould.Daily Packaging Bottle Cap Mould. |
###
| วัสดุ |
STAVAX/1.2083
|
| Hardness |
48-52HRC |
| Heat treatment |
Available |
| บริการ |
Made-to-order |
| Surface treatment |
/ |
| Closest tolerance |
+ – 0.002mm |
| Polishness |
Ra0.6 |
| Axiality |
0.005mm |
| Verticality |
0.005mm |
Designing Injection Molded Parts
Injection molded parts are a great way to produce fast, reliable parts without having to spend much time on post-processing. Whether you’re designing a small component or a large vehicle, you can expect your parts to be ready to use right away. Because of their high-speed production cycles, you can expect your parts to be delivered within 30 to 90 seconds.
Design considerations for injection molded parts
When developing a medical device, there are several design considerations to be made to create a quality injection molded part. Typically, product designers want to minimize the amount of material needed to fill the part while still maintaining the structural integrity of the product. To this end, injection molded parts often have ribs to stiffen the relatively thin walls. However, improper placement of ribs or projections can create molding problems.
Design considerations for injection molded parts include the overall shape and finish of the part. There are several ways to make the part look better. One way is to make the surface smoother and less pronounced. This will help the material flow evenly throughout the mold and minimize the risk of parting lines. Another way to reduce the risk of sink marks is to reduce the thickness of ribs relative to the nominal wall thickness of the part.
A common problem encountered when designing injection molded parts is sink marks. These can be difficult to avoid. A molder may not be willing to guarantee the product’s surface is sink-free, so designers must make sure that sink marks are minimized. To prevent these problems, the design of the parts should be as simple as possible.
Injection molded parts can also have complex geometries, and the design process is incredibly flexible. A good molder will be able to reproduce complex parts at low cost. To get the best possible results, designers should discuss the design and process with the molder. They should also discuss with the molder any critical tolerance specifications. The designer should also consider reworking the mold if necessary.
The wall thickness of a plastic injection molded part should be consistent. This is important because it influences the part’s functionality and performance. An uneven wall thickness can result in sink marks, voids, and other undesirable effects. It may also result in excessive plastic pressure or cause air traps.
Materials used in injection molded parts
When designing a product, materials used in injection molding are an important factor in the end result. These materials vary in strength, reusability, and cost. Understanding these differences is essential for ensuring the best product. In addition, understanding the characteristics of these materials can help you plan your budget and determine which ones are right for your application.
Choosing the wrong material can have serious consequences. In addition to premature component failure, the wrong choice can also increase your cost. To avoid such an occurrence, it’s a good idea to seek expert advice. Expert consultations can help you understand the factors that are important for your particular plastic molding project.
Fortron PPS: This thermoplastic resin offers excellent strength, toughness, and chemical resistance. It’s also stiff and durable, which makes it ideal for demanding industrial applications. Other common plastics include Nylon 6/6, which is strong and lightweight. Its high melting point makes it a great replacement for metal in certain environments. It also offers desirable chemical and electrical properties. PEEK is another common material used in injection molding.
ABS: Another engineering grade thermoplastic, ABS offers excellent heat resistance and chemical resistance. The disadvantage of ABS is its oil-based composition. As a result, ABS production creates noxious fumes. Nylon is another popular plastic for injection molding. Nylon is used in many different applications, from electrical applications to various kinds of apparel.
Injection moulding is a process where raw material is injected through a mold under high pressure. The mold then shapes the polymer into a desired shape. These moulds can have one or multiple cavities. This enables manufacturers to create different geometries of parts using a single mould. Most injection moulds are made from tool steel, but stainless steel and aluminium are also used for certain applications.
Characteristics of injection molded parts
 Injection molded parts exhibit a range of mechanical and physical properties. These properties affect the performance of the parts. For example, they can affect electrical conductivity. Also, the degree of filling in the parts can determine their mechanical properties. Some studies have even found that filling content can affect the dimensional accuracy of the parts.
To ensure the highest quality of the molded parts, it is important to inspect the machines and processes used to manufacture them. Proper maintenance can prevent mistakes and prolong the service life of the components. Moreover, it is essential to clean and lubricate the machine and its components. This will also reduce the possibility of mold errors.
The temperature and pressure characteristics of the injection mold can be characterized with the help of a simulation tool. For example, in a simulation environment, the injection pressure can be set as a profile and is equal to the pressure in the flow front. Moreover, the maximum injection pressure can be set as a value with minimum dependence on the flow rate. The temperature of the material used in the injection mold should be within a recommended range.
The temperature and pressure of the mold cavity must be monitored to ensure proper ejection. The temperature of the injection mold cavity is usually set at a temperature slightly above the ejection temperature. This can be manually or automatically. If the temperature is too high, the part will not be able to eject. The rapid temperature change can cause the part to warp. The same applies to the cooling time of the mold and cavity.
The thickness of the molded part should be uniform. If the injection mold does not conform to the required thickness, sink marks may be visible. A minimum of 2.5 mm between the outer and inner diameters is required for proper ejection.
Common problems encountered
There are several common problems encountered during the production of injection-molded parts. One of the most common of these is sink marks. These appear on the surface of the part and are a result of uneven cooling of the plastic within the mold. This problem can be caused by poor mold design, insufficient cooling time, and/or low injection pressure.
The first common problem occurs when the mold is not tightly clamped. This causes the molten plastic to be forced out of the mold. Other problems may occur due to the wrong clamping pressure or temperature. In these cases, the clamping force should be increased or the mold design should be revised to allow the plastic to flow properly through it. In addition, a poor quality mold may cause flash or burrs.
Another common problem is wavy patterning. These two defects can affect the appearance and functionality of the part. To avoid these problems, work with an experienced injection molding manufacturer who has experience in these types of parts. They will be able to troubleshoot and minimize any potential risks.
One of the most common problems encountered in injection molding is discoloration. A discolored part will be black or rust-colored. This problem is caused by an excess of air in the mold cavity, and can be avoided by reducing the injection speed. Ventilation systems can also be adjusted to minimize the chances of these problems.
Defective molds can cause a negative impact on the bottom line. By understanding the common problems encountered during injection molding, you can better avoid these problems and make your products as attractive as possible.
Fasteners used in injection molded parts
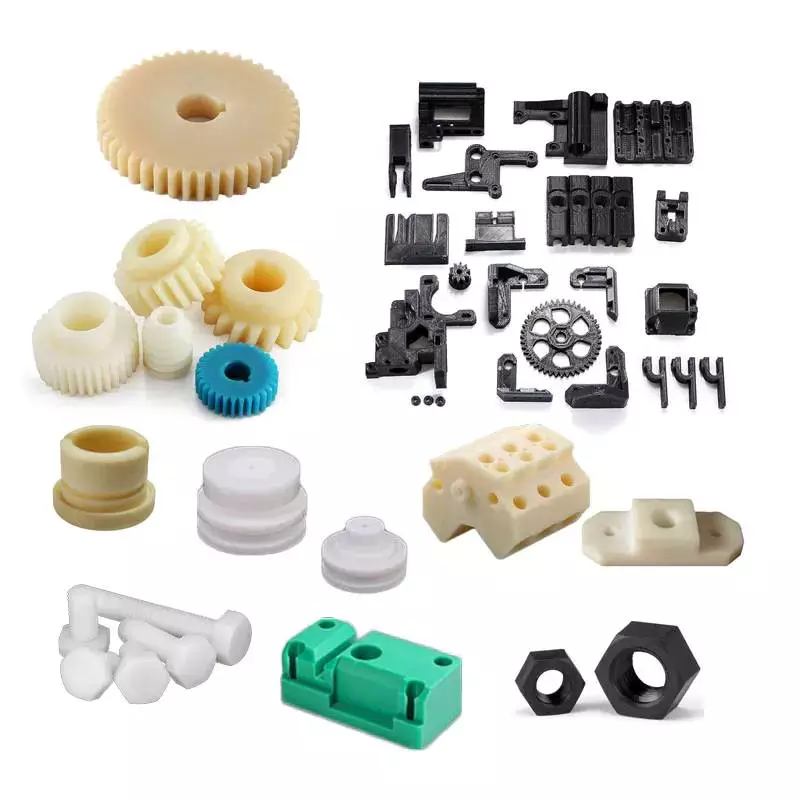 Injection molded parts often use fasteners for securing fastener elements in place. As shown in FIGS. 7 and 8 (two separate views), the fastener elements are integrated with the molded product, and they extend from one side. The fastener elements are designed to engage loop elements in the overlying layer. The palm-tree shaped fasteners are especially well-suited for this purpose, as their three-dimensional sides engage more loops than flat sides. These features result in a more secure closure.
When fasteners are used in injection molded parts, the plastic is injected into a mold, with the fastener integrated. In addition to self-tapping screws, other plastic fasteners can include moulded or pre-drilled pilot holes. This method avoids the need for a secondary assembly step and ensures an easy fit. These screws also have other advantages, including a smaller thread profile and lower radial stress, which prevents boss damage.
Another type of fastener commonly used in injection molded parts is a boss. This type of fastener is typically larger than the nut and the pilot hole. An undersized boss can lead to warpage during the injection molding process and cause a product to fail in the field.
Another type of fastener used in injection molded parts is a thread insert, which is usually a stainless steel A2 wire. There are different versions of this fastener for different materials, including carbon fiber reinforced plastic. And the fastener can be modified to adjust the size of the hole.
These fasteners are used in many different types of injection molded parts. Some parts are used to fix a variety of cosmetic issues, such as minor sinks. While these are not defects, they may not look perfect, and they can affect the overall appearance of a product. If you want to improve the appearance of an injection molded part, you can add fibers and glass fibers, as well as colorants.
editor by czh 2022-12-27
China Custom Injection Molding Plastic ABS HDPE PP PC PVC Parts injection molded plastic auto parts
Merchandise Description
Item Description
Plastic injection molding is an very flexible technique of making plastic areas and has multiple positive aspects in excess of other strategies of plastic molding. Not only is the approach simpler and much more reputable than other individuals strategies, but it is also incredibly efficient.
|
Produce name:
|
Personalized Plastic Injection Molding Elements Abs HDPE PP PVC plastic injection elements in china
|
|
Mold Shaping
|
Plastic CZPT ,plastic mould, plastic injection mildew, plastic injection mould
|
|
Colours
|
You give us PANTON# and we will match the shades
|
|
Mould Content
|
NAK80,S136,H13 ,718H,P20,and so on
|
|
Mold Cavities
|
Singe or multi as your prerequisite
|
|
Design Software
|
UG,PROE,CAD etc
|
|
Plastic Materials
|
PP, Pc, POM, PE, PU, PVC, Ab muscles, PMMA, etc
|
|
Mold Existence
|
three hundred,000-1,000,000 pictures
|
|
Shipping and delivery Time
|
fifteen-35 functioning times
|
|
Packaging
|
Picket Cases or as for each necessity
|
|
Transportation
|
By sea or by air as your prerequisite
|
|
Specification
|
As your need
|
|
OEM /ODM Buy
|
Indeed
|
In depth Photos
Our Benefits
1.Competitive cost.
2.Continuance support and support.
3.Diversified rich experienced competent workers.
four.Custom R&D software coordination.
five.Application experience.
6.Good quality,dependability and long merchandise lifestyle.
seven.Experienced,ideal and excellence,but straightforward style.
Totally free drawing design and style.
Our engineer have best technology for molding layout and cnc machining method.Definitely manufacture happy top quality areas as your ask for specifics.
3D printing prototype.
For intricate assemblies, we can print out the prototype and make confident that any proportions are right just before starting the mildew
Different material for your components
We suggest match materials for your parts, these kinds of as nylon, polyurethane, silicon,substantial polymer,PVC, Laptop,POM,PA.PP,PU,PTFE and son on.
Any particular elements we make
We are expert on non-standard components that make by variety any plastic, with large use resistance, insulation, warmth resistance and other overall performance, our engineer give you first help on your drawing.
Widely use components for all machine
If you require new device on creating device, health care device, milling device, marine device,even on the toy, please get in touch with us freely, that is our key on these .
Soon after Sales Service
Spare areas offering, like: spring, ejector pins…
Mould maintenance as a lot as possible
Some inserts or plate for value payment
Mould and plastic component design accessible
Prototype:CNC,SLC,SLS offered
Injection moulding obtainable
Software Regions
Home utility ware,auto parts,Computer electronics,Electronics factors,
Advertising and marketing samples,Health-related & dental items,Product stores, toys, interest,
New solution design & growth,Home furniture Design and style,Civil Engineering,Building,
Maritime Market,Yard Merchandise
Business Profile
HangZhou CZPT CZPT Materials Co., Ltd. is located in the Economic Growth Zone of HangZhou City, ZheJiang Province, it is 1 of the earliest organizations engaged in CZPT resources, engineering plastics, rubber and plastic items.
Company’s main products: POM, MC Nylon, Oil Nylon, HDPE, Abdominal muscles, PBT, PET, PVC, Pc, PU, PP, PTFE, PVDF, PEI, PSU, , PEEK, PAI, PI, PBI.Utra higher molecular weight polyethylene board (UHMW-PE), UPE rod, oily nylon items, PVC board, polyethylene nylon processing elements, put on-resistant materials and so on. Large-scale enterprises that generate numerous processes these kinds of as molding, injection molding, and pultrusion one particular.
Items are widely used in steel, mining, electrical power, port, paper, meals, chemical, textile and other industries.
Packaging & Delivery
Packing Information : Interior plastic bag,outside carton box,very last is the pallet,all are based on the customers’ requirments.
Supply Specifics : 10-thirty times following you confirm the samples.
FAQ
one. Q: Are you buying and selling company or maker ?
A: We are producer.
two. Q: How lengthy is your shipping and delivery time?
A: In accordance to the difficulty and quantity of merchandise processing,a realistic arrival time will be presented to you.
three. Q: Do you give samples ? is it cost-free or extra ?
A: Yes, we could provide the sample for totally free demand but do not shell out the value of freight.
4. Q: Can you do assembly and tailored bundle for us?
A: We have an assembly manufacturing unit and can assemble all kinds of plastic, steel and digital parts for you. For the completed
goods,we can custom-made the retail package deal and you can sell it straight right after acquiring them.
make contact with-data.html
| Material: |
ABS |
| Application: |
Medical, Household, Electronics, Automotive, Agricultural |
| Shaping Mode: |
Plastic Injection Mould |
| Design Service: |
According to The Customer Requirement |
| Color: |
Based on Customer Requirement |
| Drawing Format: |
Step., Igs., X_T, Dwg, Pdf, etc. |
###
###
###
|
Produce name:
|
Custom Plastic Injection Molding Parts ABS HDPE PP PVC plastic injection parts in china
|
|
Mold Shaping
|
Plastic mould ,plastic mold, plastic injection mold, plastic injection mould
|
|
Colors
|
You provide us PANTON# and we will match the colors
|
|
Mold Material
|
NAK80,S136,H13 ,718H,P20,and so on
|
|
Mold Cavities
|
Singe or multi as your requirement
|
|
Design Software
|
UG,PROE,CAD etc
|
|
Plastic Material
|
PP, PC, POM, PE, PU, PVC, ABS, PMMA, etc
|
|
Mold Life
|
300,000-1,000,000 shots
|
|
Delivery Time
|
15-35 working days
|
|
Packaging
|
Wooden Cases or as per requirement
|
|
Transportation
|
By sea or by air as your requirement
|
|
Specification
|
As your requirement
|
|
OEM /ODM Order
|
YES
|
| Material: |
ABS |
| Application: |
Medical, Household, Electronics, Automotive, Agricultural |
| Shaping Mode: |
Plastic Injection Mould |
| Design Service: |
According to The Customer Requirement |
| Color: |
Based on Customer Requirement |
| Drawing Format: |
Step., Igs., X_T, Dwg, Pdf, etc. |
###
###
###
|
Produce name:
|
Custom Plastic Injection Molding Parts ABS HDPE PP PVC plastic injection parts in china
|
|
Mold Shaping
|
Plastic mould ,plastic mold, plastic injection mold, plastic injection mould
|
|
Colors
|
You provide us PANTON# and we will match the colors
|
|
Mold Material
|
NAK80,S136,H13 ,718H,P20,and so on
|
|
Mold Cavities
|
Singe or multi as your requirement
|
|
Design Software
|
UG,PROE,CAD etc
|
|
Plastic Material
|
PP, PC, POM, PE, PU, PVC, ABS, PMMA, etc
|
|
Mold Life
|
300,000-1,000,000 shots
|
|
Delivery Time
|
15-35 working days
|
|
Packaging
|
Wooden Cases or as per requirement
|
|
Transportation
|
By sea or by air as your requirement
|
|
Specification
|
As your requirement
|
|
OEM /ODM Order
|
YES
|
Designing Injection Molded Parts
Injection molded parts are designed to work together to form a whole. While the small plastic toys like Legos aren’t typically fabricated for assembly, these products still require precision measurements. For this reason, the designs of injection molded parts should be perfected for manufacturing. The designs should also minimize error potential.
Design considerations for injection molded parts
When designing injection molded parts, it’s essential to consider the wall thickness of the part. Ideally, the wall thickness is uniform across the entire part. This allows the entire mold cavity to fill without restriction, and reduces the risk of defects. Parts that don’t have uniform wall thickness will have high stresses at the boundary between two sections, increasing the risk of cracks, warping, and twisting. To avoid such stresses, designers can consider tapering or rounding the edges of the part to eliminate stress concentration.
The wall thickness of the injection molded part is important because it affects many key characteristics. Therefore, it is critical to take proper care in choosing the wall thickness to avoid costly delays caused by mold problems or mold modification. The nominal wall thickness should be determined based on the function and stress requirements of the part. Similarly, the minimum wall thickness should be calculated based on acceptable stress. Too thin a wall can result in air traps and excessive plastic pressure.
Injection molded parts that have sharp corners are a common cause of defects. Sharp corners create stress concentrations, poor flow patterns, and increased injection mold wear. To minimize these problems, designers should keep inside corners and outside corners at half the wall thickness. This will help minimize stress and ensure the integrity of the part.
Another important design consideration for injection molded parts is the thickness of the ribs. They should be at least two-thirds of the outer wall. Thicker ribs may result in sink marks on the outer surface. Undercuts also complicate the mold design and increase the cost of the part.
Tolerance variation is also an important consideration. It depends on materials, process control, and tool design. Tolerance variation varies from molder to molder, and designers should discuss critical tolerance requirements with molders. If the part has to be manufactured to a particular tolerance, designers should consider options for mold revisions to minimize the tolerance variance. Additionally, designers may need to intentionally design extra clearance. To compensate for such variation, the molder may remove some steel or modify the design. In some cases, interference can be solved by welding.
Design considerations for injection molded parts should be discussed with material science professionals early in the design process. This is critical because changes to the mold design can be costly. Therefore, achieving the best possible result is critical. By following design guidelines, manufacturers can avoid common defects. A uniform wall thickness is also important because non-uniform thickness can lead to warping the part as it cools.
Another important factor for injection molded parts is the flowability of the material in the mold cavity. The resin should be able to flow easily around rounded corners. For example, a molded part with a curved undercut will not eject properly from the mold if there’s no space between the two sides. For this reason, designers should consider the flowability of the molded material before deciding on a design.
Adding a runner system to an injection molding machine
There are two main types of runner systems: hot runner systems and cold runner systems. In a hot runner system, a runner nozzle delivers the molten plastic into the mold cavity. A cold runner system does not require the use of a nozzle and acts as a conduit for the molten plastic.
The design of a hot runner mold should balance the activity of plastic solution and mold cavities. Ideally, a mold with two cavities is better balanced than one with three. However, it is important to remember that a three-cavity mold requires a manifold balance of human activities.
Plastic mold runner systems are crucial for ensuring consistent fill rates and pressure. Whether you are producing single or multiple-cavity plastic parts, a runner system will keep your processes consistent. When choosing a runner system, make sure you have the right one for your application.
Hot runner systems can reduce cycle times by as much as 10 to 30 percent. They help improve quality control and minimize material waste by keeping the plastic molten throughout the molding process. Moreover, they help save on plastic raw materials and energy. These features make them ideal for large production lines.
A hot runner system can also help prevent overfilling a cavity. Make sure that the volume of the hot runner is equal to the volume of the mold cavity. Otherwise, the plastic solution will be trapped inside the hot runner for too long and decompose.
Hot runner systems come in many varieties. One type of hot runner system is called the sprue hot runner system. This system uses a mechanical valve to open and close a nozzle. This type of hot runner is more effective and efficient than a general-purpose hot runner. However, it is also more expensive.
In a three-plate mold, the runner system is positioned between the core and cavity plates. When the mold is opened, the runner system automatically separates from the molded part. This eliminates the need for manual labor, but increases the cost of tooling.
The runner system is important for producing parts that are both thin and thick. The runner should be narrow but large so as not to create voids and improve the overall performance of the final product. Runner systems are also important for reducing the amount of energy needed to form and regrind the material.
A hot runner system is one way to improve the speed and accuracy of plastic molding. It helps avoid problems with waste by reducing the amount of plastic wasted. Furthermore, a hot runner system also prevents expensive repairs. By adding a runner system to an injection molding system, you will ensure better quality and precision, and avoid unnecessary downtime and costly repairs.
Hot runner systems are ideal for high-volume productions. However, they require a higher level of maintenance. In addition, hot runner systems are difficult to clean and often leave waste material. Hidden runners may also be inconvenient to remove, especially when changing materials or colors. They can also lead to sticking issues if they are made from thermally sensitive materials.
Using a thermally isolated cold injection unit
Thermostatic control of temperature in an injection molding process can make a significant impact on part quality. High mold temperatures should be regulated by using a temperature-controlled cooling unit. These devices are equipped with pumping systems and internal heaters. The temperature of the injected plastic determines the plastic’s flow characteristics and shrinkage. Temperature also influences the surface finish, dimensional stability, and physical properties of the finished product.
A thermally isolated cold injection unit allows mold operators to mold parts at lower temperatures than a conventional injection molding machine. The injection mold itself is composed of two steel halves. The two halves are connected by a mechanical hinge. During injection molding, a small amount of plastic is forced into the mold cavity. The injected plastic is then allowed to cool into a solid state. The molded part then falls out of the mold halves. The injected part then enters a bin to be collected.
The heat/cool injection molding process can improve the aesthetics of molded parts significantly. The effects of this technique are particularly apparent with amorphous resins, which do not form a skin during the injection phase. The molded parts have a higher gloss than with conventional molding techniques.
This process requires less clamping force than conventional injection molding and offers more design freedom. It also increases process capacity and materials savings. The process control for this process is more complex, with variables such as the amount of melt injection, water pressure, and water injection delay time.
The angle of repose is another criterion. A low angle indicates that the pellets are free-flowing, while an angle above 45deg indicates that the pellets are not free-flowing. This is important when processing nylon resins.
Plastic injection molding has made huge advances in recent decades. Today, most injection molds fall into one of two types: hot runner and cold runner. Each has its advantages and disadvantages. Understanding how they differ will help you decide which method is right for you.
Injection molding is a highly effective manufacturing process that gives manufacturers a competitive edge over their competition. Using this process produces high-quality plastic and metal parts with minimal waste and a low cycle time. The process is also extremely accurate and produces products with the perfect blend of flexibility and strength.
editor by czh 2022-12-26
China Custom Plastic Injection Molding Parts ABS/PP/PC/PVC/Nylon Part for Machine/ Furniture/Toy /Auto injection mold for parts
Item Description
|
Technical specs FOR FANG CZPT INJECTION MOULDS
|
|
Injection mildew standard
|
HASCO, DME, MISUMI, China lKM Common
|
|
You should give
|
Second, 3D, samples, or the measurement of the multi-angle photographs
|
|
Mould materials
|
forty five#, 50#, P20, 738, 738H, 718, 718H, NAK80, 2316, 2316A, S136, S136H and many others
|
|
Item material
|
Ab muscles, PA6, PA66, PP, Pc, TPU, POM, PBT, PVC, TPE, TPV, TPO, TPR, PE, HDPE and many others
|
|
Cavity
|
Single-cavity, Multi-cavity or by requested
|
|
Runner technique
|
Cold runner or Hot runner
|
|
Mould precision
|
±0.01mm
|
|
Mould Lifestyle
|
50-one hundred million photographs
|
|
แอปพลิเคชัน
|
CAD, Professional-E, UG, Rhinoceros and so forth
|
|
Style Time
|
one-3 times (typical conditions)
|
|
Main thechnology
|
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes and so forth
|
Business Profile
Our firm provides a wide assortment of merchandise to meet your needs. Considering that the establishment of our firm, we insist on the management plan of “top quality 1st, customer first and credit oriented”, and usually try our greatest to meet the potential requirements of our consumers. The pattern of financial globalization is creating with an unstoppable power, and our company is ready to cooperate sincerely with enterprises all in excess of the globe to achieve a CZPT circumstance.
HangZhou CZPT Plastic Merchandise Co., Ltd. is a manufacturer specializing in mildew making and injection molding, which was recognized in China in 2013.
Above the several years, we have been committed to delivering our customers with higher good quality various molds and molded elements and significantly less time.
We have our personal R&D office to give complex support. Currently, our company scope involves injection molds, blow molds, die casting molds, 3D printing, and our main items contain automotive areas, aerospace areas, digital areas, healthcare items, residence equipment areas, and many others
. We have the ability to consider your
items from conception to completion. Welcome to HangZhou CZPT Plastic Products Co.
Workshop
Custom Process
Personalized injection mold steps
one. Customers will give 3D drawings or sample inquiry, and we will estimate according to 3D drawings or samples.
2. Negotiations contain mildew value, mould high quality, mould substance, mildew cavity content, mildew dimensions, floor consequences, specialized requirements, mildew daily life, guarantee interval, item excess weight, item expense, delivery time, logistics mode, payment manner, and so on.
3. Confirm the purchase. Proforma invoice or business bill.
four. T/T deposit. 50% T/T in progress ,balance prior to cargo.
five. DFM (Design For Production), Make certain quality. CZPT style, CZPT drawing affirmation.
six. Mold processing. Comments the processing progress every single 7 days, we will display you the pictures of mildew processing.
seven. Sample affirmation. Categorical sample, confirm sample, mass generation.
8. Product packaging. Picket circumstance, carton or personalized created.
9. Supply. By Sea, By air, and so on. Pay the equilibrium.
Certifications
Our Rewards
Why Consumers Choose Us?
| We have been engaged in this discipline for 15 a long time, we’ve served buyers from the United States, the United Kingdom, Spain, Australia, Singapore, Russia and other countries. |
| Professional Certification |
| High quality management and technological innovation enhancement |
| •ISOIS09001:2000 |
| •SGS certification |
| •The complete top quality handle program. |
| Precision tough mildew |
| •3 CNC: Precision .005mm |
| •1 Three dimension:1Precision .001mm |
| •1 wire push gradually: Precision .002mm |
| •2 Mirror discharge: Precision .005mm |
| 100% Guaranteed Good quality |
| •100% analyzed(Not Just Batch Analyzed) |
| •SOP standard creation |
| •IQC(examined all in matical )-IPQC(examined 1st elements and prodcut)-FQC(tested finished elements)-OQC(Shipments) |
| •10 skilled good quality manage inspectors |
| Competitive price and support |
| •Delivery time: 2-3 Months after buy |
| •Provide new layout for customers’ requirements |
| •Provide DFM Report,Moldflow,Mould Design,MPR,QC Report, Injection parameter sheet,Screening movie. |
| •Free offered sample. |
| •10-20% less expensive than other competitors |
| •Return the whole CZPT cost if you order five hundred,000pcs merchandise. |
| •Life-lengthy assure period, which is much more time among this area. |
FAQ
China Company Precision Injection Mould Plastic Injection Mould / Steel CZPT Making Plastic Mold
1. Are you investing firm or manufacturing unit?
We are manufacturing facility with ten many years expertise.
2. How extended will get for the sample?
Generally the sample time will 3-5 functioning days. Specific time in accordance to the solution construction
3. Is it feasible to know the production situation without having going to your factory?
Thorough generation timetable will offer to you when the merchandise comfirmed. In addition, video clip will be despatched to you in the course of the generation approach.
four. What do i need to have to provide for your quoted?
Remember to deliver to us your drawing and thorough need. such as material, amount, floor therapy and so on. quotation will be ship to you inside 8 several hours
five. What’s your phrases of payment?
30% deposit in advance, 70% balance just before delivery. T/T, L/C, Escrow, Paypal and Western Union are offered.
Personalize your very own moulds in MOLDOR PLASTIC !
* In-house mould style and developing abilities to Increase work performance.
* Manufacturing unit cost can make your cost transparent.
* NDA arrangement can be signed to protect customers’ idea and layout.
* Professional sales team. Good conversation capabilities and right after-support.
* Skilled design crew, mold maker engineer. OEM/ODM service.
* Skilled QC and R&D groups to assure large top quality.
* In time reaction to letters and e-mail.
* On time supply.
US $0.3-0.5
/ Piece
|
|
1,000 Pieces
(Min. Order)
|
###
| Material: |
PVC PC ABS POM TPU TPR PP |
| Application: |
Medical, Household, Electronics, Automotive, Agricultural |
| Certification: |
RoHS, ISO |
| Die Material: |
45#, 50#, P20, 738, 738h, 718, 718h, Nak80, 2316, |
| Main Thechnology: |
Milling, Grinding, CNC, EDM, Wire Cutting, Carving |
| Mould Life: |
50-100 Million Shots |
###
###
SPECIFICATIONS FOR FANG RUI INJECTION MOULDS
|
|
|
HASCO, DME, MISUMI, China lKM Standard
|
|
|
2D, 3D, samples, or the size of the multi-angle pictures
|
|
|
45#, 50#, P20, 738, 738H, 718, 718H, NAK80, 2316, 2316A, S136, S136H etc
|
|
|
ABS, PA6, PA66, PP, PC, TPU, POM, PBT, PVC, TPE, TPV, TPO, TPR, PE, HDPE etc
|
|
|
Single-cavity, Multi-cavity or by requested
|
|
|
Cold runner or Hot runner
|
|
|
|
|
|
|
|
|
CAD, PRO-E, UG, Rhinoceros etc
|
|
|
1-3 days (normal circumstances)
|
|
|
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes etc
|
###
| We have been engaged in this field for 15 years, we’ve served customers from the United States, the United Kingdom, Spain, Australia, Singapore, Russia and other countries. |
| Professional Certification |
| Quality control and technology improvement |
| •ISOIS09001:2000 |
| •SGS certificate |
| •The complete quality control system. |
| Precision durable mold |
| •3 CNC: Precision 0.005mm |
| •1 Three dimension:1Precision 0.001mm |
| •1 wire drive slowly: Precision 0.002mm |
| •2 Mirror discharge: Precision 0.005mm |
| 100% Guaranteed Quality |
| •100% tested(Not Just Batch Tested) |
| •SOP standard production |
| •IQC(tested all in matical )-IPQC(tested first parts and prodcut)-FQC(tested finished parts)-OQC(Shipments) |
| •10 professional quality control inspectors |
| Competitive price and service |
| •Delivery time: 2-3 Weeks after order |
| •Provide new design for customers’ requirements |
| •Provide DFM Report,Moldflow,Mould Design,MPR,QC Report, Injection parameter sheet,Testing video. |
| •Free provided sample. |
| •10-20% cheaper than other competitors |
| •Return the entire mould cost if you order 500,000pcs product. |
| •Life-long guarantee period, which is much longer among this field. |
US $0.3-0.5
/ Piece
|
|
1,000 Pieces
(Min. Order)
|
###
| Material: |
PVC PC ABS POM TPU TPR PP |
| Application: |
Medical, Household, Electronics, Automotive, Agricultural |
| Certification: |
RoHS, ISO |
| Die Material: |
45#, 50#, P20, 738, 738h, 718, 718h, Nak80, 2316, |
| Main Thechnology: |
Milling, Grinding, CNC, EDM, Wire Cutting, Carving |
| Mould Life: |
50-100 Million Shots |
###
###
SPECIFICATIONS FOR FANG RUI INJECTION MOULDS
|
|
|
HASCO, DME, MISUMI, China lKM Standard
|
|
|
2D, 3D, samples, or the size of the multi-angle pictures
|
|
|
45#, 50#, P20, 738, 738H, 718, 718H, NAK80, 2316, 2316A, S136, S136H etc
|
|
|
ABS, PA6, PA66, PP, PC, TPU, POM, PBT, PVC, TPE, TPV, TPO, TPR, PE, HDPE etc
|
|
|
Single-cavity, Multi-cavity or by requested
|
|
|
Cold runner or Hot runner
|
|
|
|
|
|
|
|
|
CAD, PRO-E, UG, Rhinoceros etc
|
|
|
1-3 days (normal circumstances)
|
|
|
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes etc
|
###
| We have been engaged in this field for 15 years, we’ve served customers from the United States, the United Kingdom, Spain, Australia, Singapore, Russia and other countries. |
| Professional Certification |
| Quality control and technology improvement |
| •ISOIS09001:2000 |
| •SGS certificate |
| •The complete quality control system. |
| Precision durable mold |
| •3 CNC: Precision 0.005mm |
| •1 Three dimension:1Precision 0.001mm |
| •1 wire drive slowly: Precision 0.002mm |
| •2 Mirror discharge: Precision 0.005mm |
| 100% Guaranteed Quality |
| •100% tested(Not Just Batch Tested) |
| •SOP standard production |
| •IQC(tested all in matical )-IPQC(tested first parts and prodcut)-FQC(tested finished parts)-OQC(Shipments) |
| •10 professional quality control inspectors |
| Competitive price and service |
| •Delivery time: 2-3 Weeks after order |
| •Provide new design for customers’ requirements |
| •Provide DFM Report,Moldflow,Mould Design,MPR,QC Report, Injection parameter sheet,Testing video. |
| •Free provided sample. |
| •10-20% cheaper than other competitors |
| •Return the entire mould cost if you order 500,000pcs product. |
| •Life-long guarantee period, which is much longer among this field. |
Advantages of Injection Moulding
Whether you’re considering an injection molded part for your next project or need to replace an existing one, there are a few factors you should consider. These include design, surface finishes, tooling costs, and material compatibility. Understanding these factors can help you make the right decision. Read on to learn more about the advantages of injection molding and how to get started.
Design factors
One of the most critical design factors for injection molded parts is the wall thickness. The wall thickness affects many key characteristics of the part, from its surface finish to its structural integrity. Proper consideration of this factor can prevent costly delays due to mold issues or mold modifications. To avoid this problem, product designers must carefully consider the functional requirements of the part to determine the minimum and nominal wall thickness. In addition, they must also consider acceptable stress levels, since parts with excessively thin walls may require excessive plastic pressure and may create air traps.
Another factor to consider when designing a part is its ejection and release capabilities. If the part is released from the mold, the tools should be able to slide the plastic out. Injection molds usually have two sides, one of which is ejectable, and another that remains in the mold. In some cases, special features are required to prevent part release, such as a ramp or a gusset. These design features can increase the design flexibility, but they can also increase the cost of the mold.
When designing injection molded parts, the engineering team first determines the key design elements. These elements will make sure the injection process goes as smoothly as possible. This includes factors like wall thickness, rib design, boss design, corner transition, and weld line, among others. The engineering team will then perform a design for manufacturability analysis and, if all is well, can start building and testing the mold.
Material compatibility
Several factors can affect material compatibility of injection molded parts. When molding plastic parts, it is important to choose a material that is compatible with the part’s intended purpose. Many injection molding processes require that the two main plastic materials used are compatible with each other. This is the case in overmolding and two-shot injection molding.
The material you use to make an injection molded part will significantly impact the tolerance of the finished product. This is why material selection is as important as the design of the part. Many types of plastic resins can be used for injection molding. In addition, many of these resins can be modified or strengthened by adding additives, fillers, and stabilizers. This flexibility allows product teams to tailor the material to achieve desired performance characteristics.
One of the most common thermoplastics is polypropylene. It is extremely durable and has good impact strength and moisture resistance. This material is also recyclable and does not react with food.
Tooling costs
One of the largest costs for manufacturing injection molded parts is tooling. For an OEM, tooling costs can range from $15K per part for a simple part to $500K for a mold with complex geometry. Tooling costs vary based on the type of steel used and the production volume of the part.
To get a reasonable estimate, companies should have a final design, preliminary design, and sample part to hand when requesting quotes. The dimensions and complexity of the cavity in a mold are crucial in determining the tooling cost, as are the part tolerances. Part tolerances are based on the area covered by the part and its functions within the mold.
The type of mold you need can also impact your tooling costs. Injection molding machines can accommodate many different kinds of molds. Some molds are made from a single mold, while others require multiple molds. Some molds can be complicated, making them unmanufacturable, which in turn drives up the cost of tooling.
The costs for tooling for injection molding are not well known, but they do add up quickly. Many product development teams tend to consider the cost of the injection molding process in terms of direct materials, machine time, and labor, but that cost model often fails to take into account additional components.
Surface finishes
Surface finishes on injection molded parts are often used to mask defects, hide wear and tear, or enhance a product’s appearance. These finishes can also be useful when the product will come in contact with people’s hands. The surface texture you choose will depend on your desired functionality as well as the way you want to use the product. Generally, rougher textures provide better grip while masking minor molding imperfections. However, they can also make a product more difficult to release from the mold. This means that you may have to increase the draft angle of the mold. In order to get the best surface finish, the toolmaker and product designer must collaborate closely early in the design process.
There are several different surface finishes that can be used for injection molded parts. One type is known as the B-grade finish, and is compatible with a wide variety of injection molding plastics. Another type of finish is called a stone polishing process, and is ideal for parts that have no aesthetic value.
Overhangs
The injection moulding industry refers to overhangs on injection molded parts as “undercuts,” and these can lead to design instability. To minimize undercuts, the design must be parallel to the part’s surface. If an undercut is present, a zigzag parting line can be used.
The overhang is typically a few millimeters shorter than the surface of the mold. It is generally made from a lower-cost plastic material than the part’s surface area. The material used for the overhang should have sufficient strength to fulfill its function. An overhang will also help to prevent the piece from deforming or cracking.
Injection molding can create overhangs around the perimeter of a part. Overhangs are not always necessary; they can be added to parts as desired. Adding an overhang, however, will add substantial tooling costs. As a result, it is better to minimize the overall thickness of a design. However, in some cases an overhang can be useful to make the part look more attractive.
For parts with complex geometries, there are a few options for overhangs. Some manufacturers use side-action molds to form more complex shapes.
CNC machining
CNC machining of injection molded parts is a process that helps manufacturers achieve precise surfaces and shapes for their products. This process typically begins with the milling of the tooling, which is typically made of aluminum or steel. This tooling is then placed in a CNC mill. This machine carves the negative of the final plastic part, making it possible to achieve specific surface finishes. The process can be adapted to create a part with a complex structure or special features.
CNC machining allows the manufacturer to produce high-performance parts. This is possible because MIM parts do not experience induced stresses or internal pressure during the manufacturing process. Furthermore, the parts produced by MIM are more durable than CNC parts. Despite their advantages, CNC machining has its limitations, especially when it comes to design freedom and intricacy. This factor is largely dependent on the software used by the manufacturer or designer.
One drawback of CNC machining is its higher cost. Compared to injection molding, CNC machining is more expensive per part. The reason is that the initial mold cost is relatively high and is spread over a large number of parts. Once the injection molding process has been completed, the cost of the parts produced by this process becomes more competitive with those produced by machined parts. However, the cost gap increases with the volume of parts produced. This cost crossover generally occurs in quantities of at least 100 parts and can reach a maximum of 5000 parts.
Production volume
The production volume of injection molded parts varies depending on the material being used. Large volumes of parts are expensive to produce, while small quantities can be produced for low cost. Injection molding requires a precise mold, which is CNC-machined from tool steel or aluminum. The mold has a negative of the part that is injected, a runner system, and internal water cooling channels to aid in cooling the part. Recent advances in 3D printing materials have made it possible to produce molds for low-volume injection molding. Previously, this was not financially viable due to the high cost of traditional mold making.
A mold is used to produce plastic parts. The molding process is very fast, with each cycle taking anywhere from 30 seconds to 90 seconds. After a part is molded, it is removed from the mold and placed on a holding container or conveyor belt. Injection molded parts are generally ready for use right away and require minimal post-processing. Injection molded parts have a similar design to a photograph, since the geometry is directly transferred to the part’s surface texture.
When selecting a plastic mold, it is important to determine the volume that the part will be produced at. If the volume is low, softer plastics may be used. However, as the part is molded over, its performance characteristics may degrade. In low-volume production, it is important to consider the overall complexity of the part. This includes the part’s draft, wall thickness, and surface finish.
editor by czh 2022-12-25
China Die Casting Precision Custom Injection Molded Plastic Products injection molded plastic auto parts
Item Description
Specialist OEM/ODM Injection Mould/Stamping Mold Maker and Machining Component for Metallic Machinery Parts
| Mold Variety |
Plastic injection mould, overmolding, Interchangeable Mildew, insert molding, compression mold, stamping mildew, etc |
|
| Design software |
UG, ProE, Auto CAD, Solidworks, and so forth. |
| Main solutions |
Prototypes, Mold design, Mould generating, Mildew tesing,
lower quantity/substantial quantity plastic manufacturing |
|
| Certificate |
ISO 9001:2015 |
| Metal substance |
718H,P20,NAK80,S316H,SKD61, and many others. |
| Plastic production Raw substance |
PP,Pa6,PLA,AS,Ab muscles,PE,Personal computer,POM,PVC, PET,PS,TPE/TPR etc |
| Mildew base |
HASCO ,DME ,LKM,JLS regular |
| Mildew runner |
Cold runner, scorching runner |
| Mold hot runner |
DME, HASCO, YUDO,etc |
| Mould cold runner |
stage way, side way, adhere to way, direct gate way,etc. |
| Mold strandard elements |
DME, HASCO, etc. |
| mould daily life |
>300,000 photographs |
| Mold hot treatment |
quencher, nitridation, tempering,and so on. |
| Mildew cooling system |
water cooling or Beryllium bronze cooling, etc. |
| Mould surface area |
EDM, texture, high gloss sharpening |
| Hardness of the metal |
twenty~sixty HRC |
| Equipments |
High velocity CNC, standard CNC, EDM, Wire reducing, Grinder,
Lathe, Milling equipment, plastic injection device |
|
| Lead time |
twenty five~30 days |
| Thirty day period Creation |
50 sets/thirty day period |
| Mould Packing |
regular exporting Picket case |
Metal Equipment Parts:
Except mold generating, we also make equipment areas for House Appliances/ Vehicle/ Commpdity/ Residence Use/ Electronic/ Offical Products/ Health-related Apparatus ect.
Mould Screen:
Our tooling shop owns precision producing equipments and skillful employees. We design and style and make molds depending on your annual production demands.
To enhance the production capability, new sophisticated technology and equipment are released into our manufacturing unit. Now our mildew producing ability is compliant with the worldwide specifications of mould sector.
Manufacturing unit:
With more than 10 years knowledge in personalized tooling and injection molding, we have become a great mildew maker in manufacturing all kinds of plastic injection molds, stamping parts and machining elements.
50% of our molds are exported to far more than 30 nations around the world in Europe, North The us, South The usa, Mid-east and Australia. 50% in nearby industry.
With scientific mould layout, innovative technology, mindful production and humanized service, Inexperienced Vitality can attain and exceed customer’s expectation. We have knowledgeable mould makers. They are acquainted with HASCO, DME and so forth regular mildew components. They are properly trained to operate each method of mold production and strictly management the producing time for supply guarantee.
We personal modern day Japanese administration and innovative mould process gear. The equipment enables us to offer our buyers with unique remedy of limited machining precision and punctual shipping.
Cerification:
Shipment:
We typically shipping the moulds and equipment elements by sea/DHL/FedEx/TNT, according to the clients.
FAQ:
one. Q: What is the processing for the estimate?
A: We can estimate from your 3D formats like IGS, STP, PARASOLID and so on and 2nd drawings as effectively Quotation the value to clients after got the 2d or 3D drawings within 2 hours
two. Q: How is the next?
A: We will deliver the expense to you and get your confirmations for the quote
3. Q: What is the software program will you use for the continuing?
A: We make the 3D programm with Professional-Engineer, UGS, SOLIDWORKS, MASTERCAM etc
four. Q: What is the type of machines for producing?
A: Made from CNC Machining, Laser slicing, stamping, injection as nicely as the parts data files different
five. Q: Do you do the floor remedies you should?
A: Sure, positive. We do the surface area treatments, for instance: Chromated, powder coating, Anodizing, laser etching as effectively as painting
6. Q: What is the good quality Control just before transport?
A: We have QC department for the good quality management prior to shipping
US $1,000-3,000
/ Piece
|
|
1 Piece
(Min. Order)
|
###
| Shaping Mode: |
Injection Mould |
| Surface Finish Process: |
Anodizing |
| Mould Cavity: |
Custom Cavity |
| Plastic Material: |
HDPE |
| Process Combination Type: |
Single-Process Mode |
| Application: |
Car, Household Appliances, Furniture, Commodity, Electronic, Home Use, Hardware |
###
###
| Mold Type |
Plastic injection mold, overmolding, Interchangeable Mold, insert molding, compression mold, stamping mold, etc |
|
| Design software |
UG, ProE, Auto CAD, Solidworks, etc. |
| Main services |
Prototypes, Mold design, Mold making, Mold tesing,
low volume/high volume plastic production |
|
| Certificate |
ISO 9001:2015 |
| Steel material |
718H,P20,NAK80,S316H,SKD61, etc. |
| Plastic production Raw material |
PP,Pa6,PLA,AS,ABS,PE,PC,POM,PVC, PET,PS,TPE/TPR etc |
| Mold base |
HASCO ,DME ,LKM,JLS standard |
| Mold runner |
Cold runner, hot runner |
| Mold hot runner |
DME, HASCO, YUDO,etc |
| Mold cold runner |
point way, side way, follow way, direct gate way,etc. |
| Mold strandard parts |
DME, HASCO, etc. |
| mold life |
>300,000 shots |
| Mold hot treatment |
quencher, nitridation, tempering,etc. |
| Mold cooling system |
water cooling or Beryllium bronze cooling, etc. |
| Mold surface |
EDM, texture, high gloss polishing |
| Hardness of the steel |
20~60 HRC |
| Equipments |
High speed CNC, standard CNC, EDM, Wire cutting, Grinder,
Lathe, Milling machine, plastic injection machine |
|
| Lead time |
25~30 days |
| Month Production |
50 sets/month |
| Mold Packing |
standard exporting Wooden case |
US $1,000-3,000
/ Piece
|
|
1 Piece
(Min. Order)
|
###
| Shaping Mode: |
Injection Mould |
| Surface Finish Process: |
Anodizing |
| Mould Cavity: |
Custom Cavity |
| Plastic Material: |
HDPE |
| Process Combination Type: |
Single-Process Mode |
| Application: |
Car, Household Appliances, Furniture, Commodity, Electronic, Home Use, Hardware |
###
###
| Mold Type |
Plastic injection mold, overmolding, Interchangeable Mold, insert molding, compression mold, stamping mold, etc |
|
| Design software |
UG, ProE, Auto CAD, Solidworks, etc. |
| Main services |
Prototypes, Mold design, Mold making, Mold tesing,
low volume/high volume plastic production |
|
| Certificate |
ISO 9001:2015 |
| Steel material |
718H,P20,NAK80,S316H,SKD61, etc. |
| Plastic production Raw material |
PP,Pa6,PLA,AS,ABS,PE,PC,POM,PVC, PET,PS,TPE/TPR etc |
| Mold base |
HASCO ,DME ,LKM,JLS standard |
| Mold runner |
Cold runner, hot runner |
| Mold hot runner |
DME, HASCO, YUDO,etc |
| Mold cold runner |
point way, side way, follow way, direct gate way,etc. |
| Mold strandard parts |
DME, HASCO, etc. |
| mold life |
>300,000 shots |
| Mold hot treatment |
quencher, nitridation, tempering,etc. |
| Mold cooling system |
water cooling or Beryllium bronze cooling, etc. |
| Mold surface |
EDM, texture, high gloss polishing |
| Hardness of the steel |
20~60 HRC |
| Equipments |
High speed CNC, standard CNC, EDM, Wire cutting, Grinder,
Lathe, Milling machine, plastic injection machine |
|
| Lead time |
25~30 days |
| Month Production |
50 sets/month |
| Mold Packing |
standard exporting Wooden case |
Designing Injection Molded Parts
Injection molded parts are a great way to produce fast, reliable parts without having to spend much time on post-processing. Whether you’re designing a small component or a large vehicle, you can expect your parts to be ready to use right away. Because of their high-speed production cycles, you can expect your parts to be delivered within 30 to 90 seconds.
Design considerations for injection molded parts
When developing a medical device, there are several design considerations to be made to create a quality injection molded part. Typically, product designers want to minimize the amount of material needed to fill the part while still maintaining the structural integrity of the product. To this end, injection molded parts often have ribs to stiffen the relatively thin walls. However, improper placement of ribs or projections can create molding problems.
Design considerations for injection molded parts include the overall shape and finish of the part. There are several ways to make the part look better. One way is to make the surface smoother and less pronounced. This will help the material flow evenly throughout the mold and minimize the risk of parting lines. Another way to reduce the risk of sink marks is to reduce the thickness of ribs relative to the nominal wall thickness of the part.
A common problem encountered when designing injection molded parts is sink marks. These can be difficult to avoid. A molder may not be willing to guarantee the product’s surface is sink-free, so designers must make sure that sink marks are minimized. To prevent these problems, the design of the parts should be as simple as possible.
Injection molded parts can also have complex geometries, and the design process is incredibly flexible. A good molder will be able to reproduce complex parts at low cost. To get the best possible results, designers should discuss the design and process with the molder. They should also discuss with the molder any critical tolerance specifications. The designer should also consider reworking the mold if necessary.
The wall thickness of a plastic injection molded part should be consistent. This is important because it influences the part’s functionality and performance. An uneven wall thickness can result in sink marks, voids, and other undesirable effects. It may also result in excessive plastic pressure or cause air traps.
Materials used in injection molded parts
When designing a product, materials used in injection molding are an important factor in the end result. These materials vary in strength, reusability, and cost. Understanding these differences is essential for ensuring the best product. In addition, understanding the characteristics of these materials can help you plan your budget and determine which ones are right for your application.
Choosing the wrong material can have serious consequences. In addition to premature component failure, the wrong choice can also increase your cost. To avoid such an occurrence, it’s a good idea to seek expert advice. Expert consultations can help you understand the factors that are important for your particular plastic molding project.
Fortron PPS: This thermoplastic resin offers excellent strength, toughness, and chemical resistance. It’s also stiff and durable, which makes it ideal for demanding industrial applications. Other common plastics include Nylon 6/6, which is strong and lightweight. Its high melting point makes it a great replacement for metal in certain environments. It also offers desirable chemical and electrical properties. PEEK is another common material used in injection molding.
ABS: Another engineering grade thermoplastic, ABS offers excellent heat resistance and chemical resistance. The disadvantage of ABS is its oil-based composition. As a result, ABS production creates noxious fumes. Nylon is another popular plastic for injection molding. Nylon is used in many different applications, from electrical applications to various kinds of apparel.
Injection moulding is a process where raw material is injected through a mold under high pressure. The mold then shapes the polymer into a desired shape. These moulds can have one or multiple cavities. This enables manufacturers to create different geometries of parts using a single mould. Most injection moulds are made from tool steel, but stainless steel and aluminium are also used for certain applications.
Characteristics of injection molded parts
Injection molded parts exhibit a range of mechanical and physical properties. These properties affect the performance of the parts. For example, they can affect electrical conductivity. Also, the degree of filling in the parts can determine their mechanical properties. Some studies have even found that filling content can affect the dimensional accuracy of the parts.
To ensure the highest quality of the molded parts, it is important to inspect the machines and processes used to manufacture them. Proper maintenance can prevent mistakes and prolong the service life of the components. Moreover, it is essential to clean and lubricate the machine and its components. This will also reduce the possibility of mold errors.
The temperature and pressure characteristics of the injection mold can be characterized with the help of a simulation tool. For example, in a simulation environment, the injection pressure can be set as a profile and is equal to the pressure in the flow front. Moreover, the maximum injection pressure can be set as a value with minimum dependence on the flow rate. The temperature of the material used in the injection mold should be within a recommended range.
The temperature and pressure of the mold cavity must be monitored to ensure proper ejection. The temperature of the injection mold cavity is usually set at a temperature slightly above the ejection temperature. This can be manually or automatically. If the temperature is too high, the part will not be able to eject. The rapid temperature change can cause the part to warp. The same applies to the cooling time of the mold and cavity.
The thickness of the molded part should be uniform. If the injection mold does not conform to the required thickness, sink marks may be visible. A minimum of 2.5 mm between the outer and inner diameters is required for proper ejection.
Common problems encountered
There are several common problems encountered during the production of injection-molded parts. One of the most common of these is sink marks. These appear on the surface of the part and are a result of uneven cooling of the plastic within the mold. This problem can be caused by poor mold design, insufficient cooling time, and/or low injection pressure.
The first common problem occurs when the mold is not tightly clamped. This causes the molten plastic to be forced out of the mold. Other problems may occur due to the wrong clamping pressure or temperature. In these cases, the clamping force should be increased or the mold design should be revised to allow the plastic to flow properly through it. In addition, a poor quality mold may cause flash or burrs.
Another common problem is wavy patterning. These two defects can affect the appearance and functionality of the part. To avoid these problems, work with an experienced injection molding manufacturer who has experience in these types of parts. They will be able to troubleshoot and minimize any potential risks.
One of the most common problems encountered in injection molding is discoloration. A discolored part will be black or rust-colored. This problem is caused by an excess of air in the mold cavity, and can be avoided by reducing the injection speed. Ventilation systems can also be adjusted to minimize the chances of these problems.
Defective molds can cause a negative impact on the bottom line. By understanding the common problems encountered during injection molding, you can better avoid these problems and make your products as attractive as possible.
Fasteners used in injection molded parts
Injection molded parts often use fasteners for securing fastener elements in place. As shown in FIGS. 7 and 8 (two separate views), the fastener elements are integrated with the molded product, and they extend from one side. The fastener elements are designed to engage loop elements in the overlying layer. The palm-tree shaped fasteners are especially well-suited for this purpose, as their three-dimensional sides engage more loops than flat sides. These features result in a more secure closure.
When fasteners are used in injection molded parts, the plastic is injected into a mold, with the fastener integrated. In addition to self-tapping screws, other plastic fasteners can include moulded or pre-drilled pilot holes. This method avoids the need for a secondary assembly step and ensures an easy fit. These screws also have other advantages, including a smaller thread profile and lower radial stress, which prevents boss damage.
Another type of fastener commonly used in injection molded parts is a boss. This type of fastener is typically larger than the nut and the pilot hole. An undersized boss can lead to warpage during the injection molding process and cause a product to fail in the field.
Another type of fastener used in injection molded parts is a thread insert, which is usually a stainless steel A2 wire. There are different versions of this fastener for different materials, including carbon fiber reinforced plastic. And the fastener can be modified to adjust the size of the hole.
These fasteners are used in many different types of injection molded parts. Some parts are used to fix a variety of cosmetic issues, such as minor sinks. While these are not defects, they may not look perfect, and they can affect the overall appearance of a product. If you want to improve the appearance of an injection molded part, you can add fibers and glass fibers, as well as colorants.
editor by czh 2022-12-24