
产品描述
详细照片
我们的优势
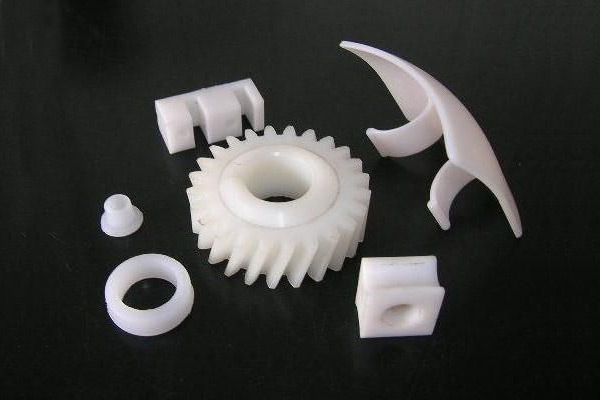
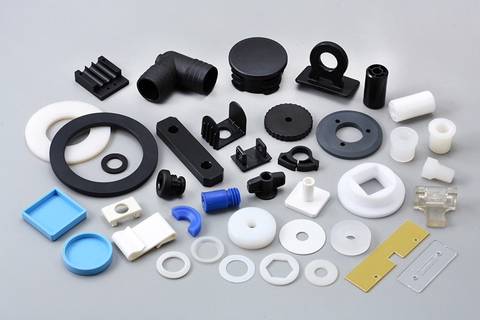
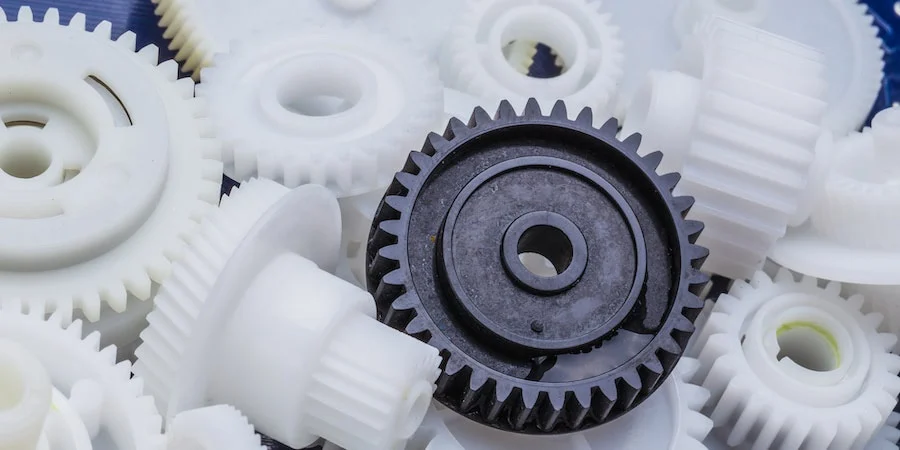
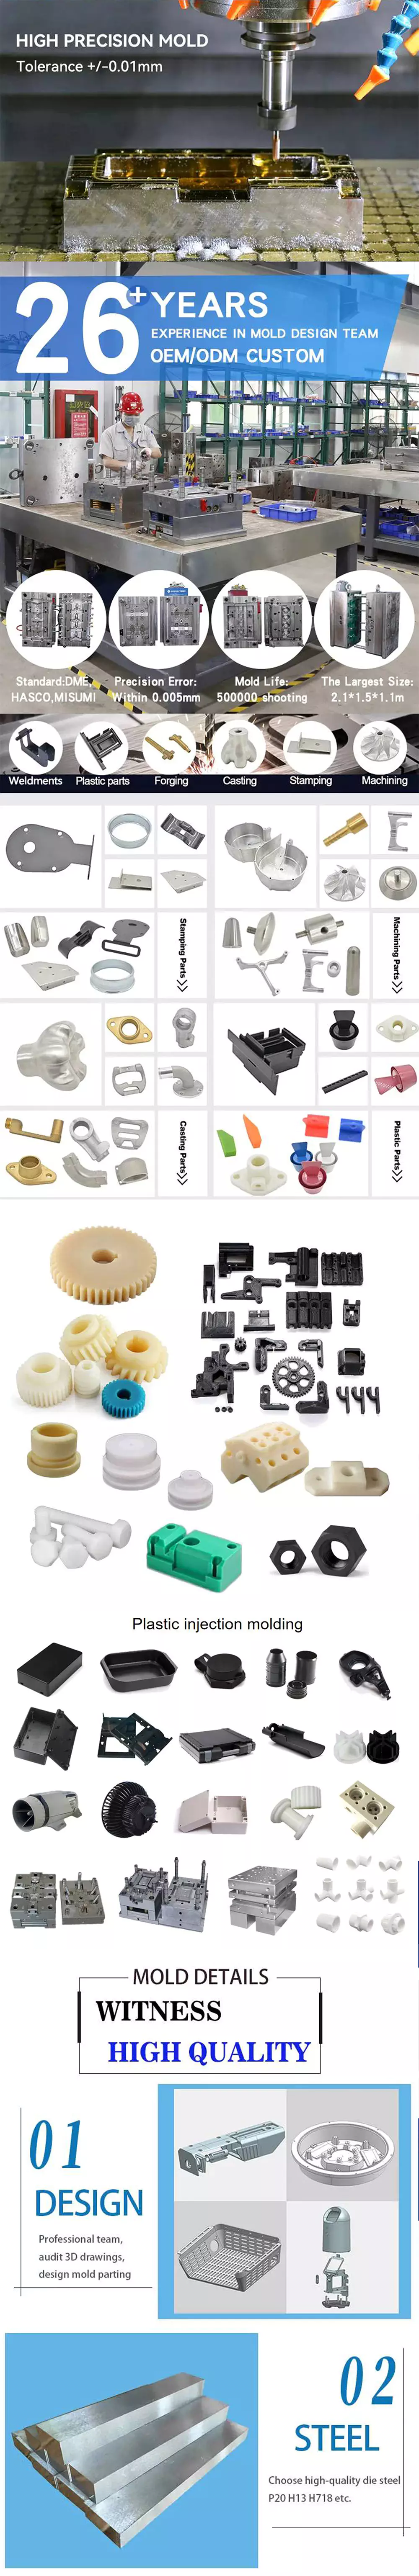
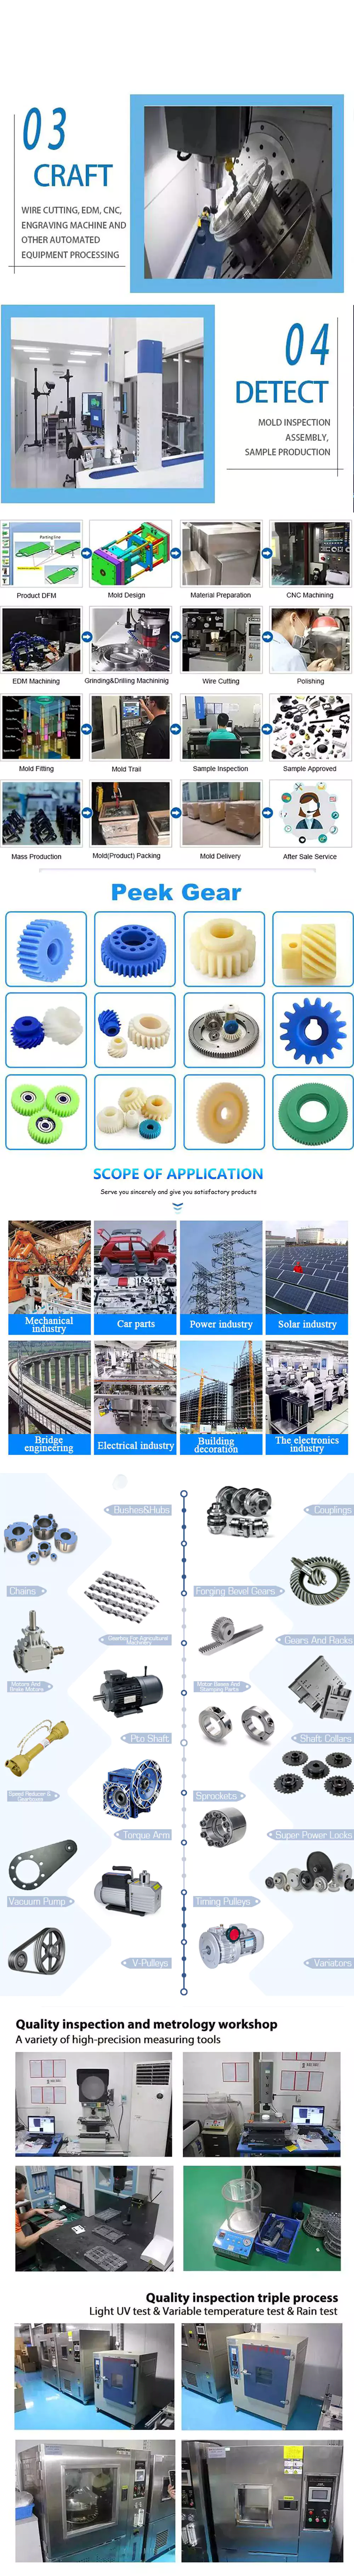
Our factory is specialized in the production of engineering plastic processing manufacturers, with rich experience and advanced equipment. All year round production injection molding, extrusion, rolling, casting CNC engineering CHINAMFG processing.The plastic products of our factory are carefully made of excellent raw materials, which are stable performance, long service life, reliable quality, good compression and impact resistance. Complete types of specifications and a variety of optional materials, which can turn your design into reality. Response speed, shipment speed, is your quality supplier. Contact us and Welcome to place order.
认证
| 产品描述 | |
|
Products: |
Plastic parts |
| 材料: | ABS, AS, PA, PE, PP PVC, PC, PE, Nylon, EPDM, POM, EPT^ |
| Surface Treat:
|
Paint, texture |
| 尺寸 | 定制 |
| 颜色 | Any color |
| 3D,CAD drawing | Accepted |
| 温度 | -40°C to+300°C |
| 硬度 | 30-95 shore A |
| Logo | OEM & ODM orders are welcomed |
| 宽容 | 0.05mm |
| 包裹 | Standard package or according to your request |
| 特征 | 1.CHINAMFG and Chemical resistance |
| 2. Anti-aging, good flexibility, good elasticity | |
| 3. Excellent oil resistance | |
| 应用 | Electronic field, industrial machine & equipment,house-hold appliance,tele-communication,automobile,medical equipment industry etc. |
| Delivery | 10 days-20 days |
| Note | 1.Models and Logos can be Customized according to your Requirement |
| 2.Designs and Specification are Accepted |
公司简介
After Sales Service
| 材料: | ABS、PP、HDPE、LDPE、尼龙、POM、PC、HIPS、TPR等 |
|---|---|
| 应用: | Electronics |
| 认证: | ISO |
| Process: | Plastic Injection |
| 霉菌寿命: | 500, 000-1, 000, 000 Shots |
| Transport Package: | Bags, Cartons, Pallets, Carton Box |
| 示例: |
US$ 1件
1 件(最低订购量) | |
|---|
| 定制化: |
可用的
|
|
|---|
材料选择对注塑件的性能和耐久性有何影响?
注塑件的材料选择对其性能和耐久性有着显著影响。材料的选择会影响诸多关键因素,包括机械性能、耐化学性、热稳定性、尺寸稳定性以及零件的整体功能。以下详细阐述了材料选择对注塑件性能和耐久性的影响:
机械性能:
材料的机械性能直接影响零件的强度、刚度、抗冲击性和疲劳寿命。不同的材料具有不同的拉伸强度、弯曲强度、弹性模量和断裂伸长率。选择具有合适机械性能的材料,可以确保注塑成型的零件能够承受外力、振动和运行应力而不发生失效或变形。
耐化学性:
在部件会接触腐蚀性物质的应用中,材料的耐化学性和耐溶剂性至关重要。某些材料,例如工程热塑性塑料,如ABS(丙烯腈-丁二烯-苯乙烯共聚物)或PEEK(聚醚醚酮),具有优异的耐化学性。选择具有合适耐化学性的材料,可确保注塑成型的部件在暴露于特定化学品或环境时保持其完整性和功能性。
热稳定性:
在涉及高温或热循环的应用中,材料的热稳定性至关重要。不同材料的熔点、玻璃化转变温度和热变形温度各不相同。选择具有合适热稳定性的材料,可确保注塑成型的零件能够承受预期的温度变化,而不会发生尺寸变化、翘曲或机械性能下降。
尺寸稳定性:
在对公差和尺寸精度要求极高的应用中,材料的尺寸稳定性至关重要。某些材料,例如工程热塑性塑料或填充聚合物,具有较低的热膨胀系数,从而最大限度地减少零件尺寸随温度变化而发生的变化。选择尺寸稳定性良好的材料有助于确保注塑成型的零件在较宽的工作温度范围内保持其形状、尺寸和关键尺寸。
部件功能:
材料的选择直接影响注塑件的功能和性能。不同的材料具有独特的性能,可以根据具体的应用需求进行定制。例如,聚碳酸酯 (PC) 或聚丙烯 (PP) 等材料具有优异的透明度,适用于需要光学透明度的应用;而聚酰胺 (PA) 或聚甲醛 (POM) 等材料则具有低摩擦系数和耐磨性,适用于运动或滑动部件。
周期时间和加工性能:
材料的选择也会影响注塑成型的周期时间和工艺性能。不同的材料具有不同的熔体粘度和流动特性,这会影响成型过程中的填充和冷却时间。流动性好的材料更容易填充复杂的模具几何形状,从而缩短周期时间并提高生产效率。因此,选择一种能够利用现有注塑设备和技术有效加工的材料至关重要。
成本考量:
材料的选择也会影响注塑件的总成本。不同的材料成本各异,选择最合适的材料需要考虑诸多因素,例如材料的可用性、模具要求、加工条件以及所需的性能特征。在预算范围内,平衡性能要求和成本考量对于选择能够满足性能和耐久性要求的最佳材料至关重要。
总体而言,材料选择对注塑件的性能、耐久性和功能性起着至关重要的作用。仔细考虑机械性能、耐化学性、热稳定性、尺寸稳定性、零件功能、生产周期、加工性能和成本因素,有助于确保所选材料满足特定的应用要求,并在零件的预期使用寿命内提供所需的性能和耐久性。
Can you describe the various post-molding processes, such as assembly or secondary operations, for injection molded parts?
Post-molding processes play a crucial role in the production of injection molded parts. These processes include assembly and secondary operations that are performed after the initial molding stage. Here’s a detailed explanation of the various post-molding processes for injection molded parts:
1. Assembly:
Assembly involves joining multiple injection molded parts together to create a finished product or sub-assembly. The assembly process can include various techniques such as mechanical fastening (screws, clips, or snaps), adhesive bonding, ultrasonic welding, heat staking, or solvent welding. Assembly ensures that the individual molded parts are securely combined to achieve the desired functionality and structural integrity of the final product.
2. Surface Finishing:
Surface finishing processes are performed to enhance the appearance, texture, and functionality of injection molded parts. Common surface finishing techniques include painting, printing (such as pad printing or screen printing), hot stamping, laser etching, or applying specialized coatings. These processes can add decorative features, branding elements, or improve the surface properties of the parts, such as scratch resistance or UV protection.
3. Machining or Trimming:
In some cases, injection molded parts may require additional machining or trimming to achieve the desired final dimensions or remove excess material. This can involve processes such as CNC milling, drilling, reaming, or turning. Machining or trimming is often necessary when tight tolerances, specific geometries, or critical functional features cannot be achieved solely through the injection molding process.
4. Welding or Joining:
Welding or joining processes are used to fuse or bond injection molded parts together. Common welding techniques for plastic parts include ultrasonic welding, hot plate welding, vibration welding, or laser welding. These processes create strong and reliable joints between the molded parts, ensuring structural integrity and functionality in the final product.
5. Insertion of Inserts:
Insertion involves placing metal or plastic inserts into the mold cavity before the injection molding process. These inserts can provide additional strength, reinforce threaded connections, or serve as mounting points for other components. Inserts can be placed manually or using automated equipment, and they become permanently embedded in the molded parts during the molding process.
6. Overmolding or Two-Shot Molding:
Overmolding or two-shot molding processes allow for the creation of injection molded parts with multiple layers or materials. In overmolding, a second material is molded over a pre-existing substrate, providing enhanced functionality, aesthetics, or grip. Two-shot molding involves injecting two different materials into different sections of the mold to create a single part with multiple colors or materials. These processes enable the integration of multiple materials or components into a single injection molded part.
7. Deflashing or Deburring:
Deflashing or deburring processes involve removing excess flash or burrs that may be present on the molded parts after the injection molding process. Flash refers to the excess material that extends beyond the parting line of the mold, while burrs are small protrusions or rough edges caused by the mold features. Deflashing or deburring ensures that the molded parts have smooth edges and surfaces, improving their appearance, functionality, and safety.
8. Inspection and Quality Control:
Inspection and quality control processes are performed to ensure that the injection molded parts meet the required specifications and quality standards. This can involve visual inspection, dimensional measurement, functional testing, or other specialized testing methods. Inspection and quality control processes help identify any defects, inconsistencies, or deviations that may require rework or rejection of the parts, ensuring that only high-quality parts are used in the final product or assembly.
9. Packaging and Labeling:
Once the post-molding processes are complete, the injection molded parts are typically packaged and labeled for storage, transportation, or distribution. Packaging can include individual part packaging, bulk packaging, or custom packaging based on specific requirements. Labeling may involve adding product identification, barcodes, or instructions for proper handling or usage.
These post-molding processes are vital in achieving the desired functionality, appearance, and quality of injection molded parts. They enable the integration of multiple components, surface finishing, dimensional accuracy, and assembly of the final products or sub-assemblies.
与其他制造方法相比,注塑成型零件在成本和效率方面有何不同?
与其他制造方法相比,注塑成型零件在成本和效率方面具有显著优势。注塑成型工艺效率高、成本效益好,尤其适用于大规模生产。以下详细比较了注塑成型零件与其他制造方法:
成本比较:
与其他制造方法相比,注塑成型具有成本效益,原因有以下几点:
1. 模具成本:
注塑成型需要前期投入资金用于模具制造,这笔费用可能较高。然而,模具一旦制作完成,即可重复使用,用于生产大量零件,从而降低单位成本。模具成本的摊销使得注塑成型在大批量生产中更具成本效益。
2. 材料利用率:
注塑成型在材料利用方面效率极高。该工艺能够精确控制注入模具的材料量,最大限度地减少浪费。此外,成型过程中产生的多余材料可以回收再利用,与那些会产生大量废料的成型方法相比,进一步降低了材料成本。
3. 人工成本:
注塑成型是一种高度自动化的工艺,与其他制造方法相比,所需人工极少。模具安装完毕、工艺参数设定完成后,注塑机即可连续运行,在极少人工干预的情况下生产零件。这种自动化降低了人工成本,提高了整体效率。
效率比较:
注塑成型零件在效率方面具有以下几个优势:
1. 快速生产周期:
注塑成型是一种快速制造工艺,能够在相对较短的周期内生产零件。周期时间取决于零件的复杂程度、材料特性和冷却时间等因素。然而,与其他方法(例如机械加工或铸造)相比,注塑成型可以在每个周期内同时生产多个零件,从而实现更高的生产率和更优的效率。
2. 高精度和一致性:
注塑成型能够生产高精度、高一致性的零件。注塑模具的设计旨在提供精确且可重复的尺寸控制。这种精度确保每个零件都符合所需规格,从而减少了后续加工或后处理的需求。持续生产高精度零件的能力提高了效率,并减少了返工或废品相关的时间和成本。
3. 可扩展性:
注塑成型具有高度可扩展性,因此既适用于小批量生产,也适用于大批量生产。模具一旦制作完成,注塑成型工艺即可轻松复制,从而高效生产出相同的零件。这种快速高效的生产规模化能力,使注塑成型成为满足不断变化的市场需求的理想选择。
4. 设计复杂度:
注塑成型技术能够生产具有复杂几何形状和精细细节的零件。模具设计可适应倒扣、薄壁和复杂形状,而这些对于其他制造方法来说可能具有挑战性或成本高昂。这种设计灵活性允许将多个组件集成到单个零件中,从而减少装配要求和潜在的故障点。高效生产复杂设计的能力提高了整体效率和功能性。
5. 材料多样性:
注塑成型工艺支持多种热塑性材料,可根据最终零件所需的性能灵活选择材料。选择不同的材料可以获得特定的特性,例如强度、柔韧性、耐热性、耐化学腐蚀性或透明度。这种材料的多样性使得零件性能的定制和优化成为可能。
总而言之,与其他许多制造方法相比,注塑成型零件具有成本效益高、效率高的优点。虽然初始模具成本较高,但由于能够以较低的单位成本生产大量零件,因此可以有效抵消这些成本。材料利用率高、自动化程度高、生产周期短、精度高、可扩展性强、能够应对复杂的设计以及材料适用性强,这些都提高了注塑成型的整体成本效益和效率。这些优势使得注塑成型成为众多行业高效经济地生产高质量零件的首选。
editor by CX 2023-11-23

























