
وصف المنتج
plastic molding
وصف المنتج
| Product Information | |||
| اسم المنتج | OEM CNC Machining Plastic Parts | ||
| Quotation | According to your drawing (material / Size / Required Technology / Etc.) | ||
| Drawing Formats | 2D(PDF/CAD) And 3D(STP/STEP) | ||
| Quotation | According To Your Drawing(Size / Material / Required Technology / Etc.) | ||
| مواد | ABS / PC+ABS / PC / PP / Nylon (PA6/66) / POM / PVC / PMMA / TPE / TPU / PC+GF / Etc. | ||
| Surface finish | Polishing Finish / Slik Print / Texture Finish / Rubber Painting / Glossy Finish / Painting / Slik-Screen / Pad Print / EMI Coating / Electronic Plating / Laser Marking / Etc. | ||
| Technology | Foaming / Ordinary Injection / Structual Foam Molding / Over-Molding / Gas Assisted Injection Molding | ||
| Production Process | Orders-Raw Materials- Production-Quality Inspection -Packaging-Shipment | ||
| التعبئة والتغليف | PE bag + paper card/paper skin + export-grade carton / crate / Pallet | ||
| Delivery | 1~4 weeks depends on order quantity | ||
111
Company Information
التعليمات
س1: Avaliable for customized design drawings?
A:Yes, DWG, DXF,DXW, IGES, STEP, PDF etc.Or you can send us samples for scHangZhou.
س2: Will my drawing be safe after you get it?
A:Yes, we can CHINAMFG the NDA before you send the drawing.Or you can send us samples for scHangZhou.
س3: Can we know the production process without visiting the factory?
A:We will offer detailed production schedule and send weekly reports with digital pictures and videos which show the production progress.
الربع الرابع:What craftsmanship do you have for processing accessories?
A:According to different products, different processes are used, such as machining, extrusion, injection molding, etc.
س5: What areyour processing equipment?
A:CNC machining center, CNC lathe, milling machine, engraving machine, injection molding machine,extruder, molding machine.
س6:Can injection products be surface treated? What are the surface treatments?
A:It’s okay. Surface treatment: spray paint, silk screen,electroplating, etc.
/* May 10, 2571 16:49:51 */!function(){function d(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
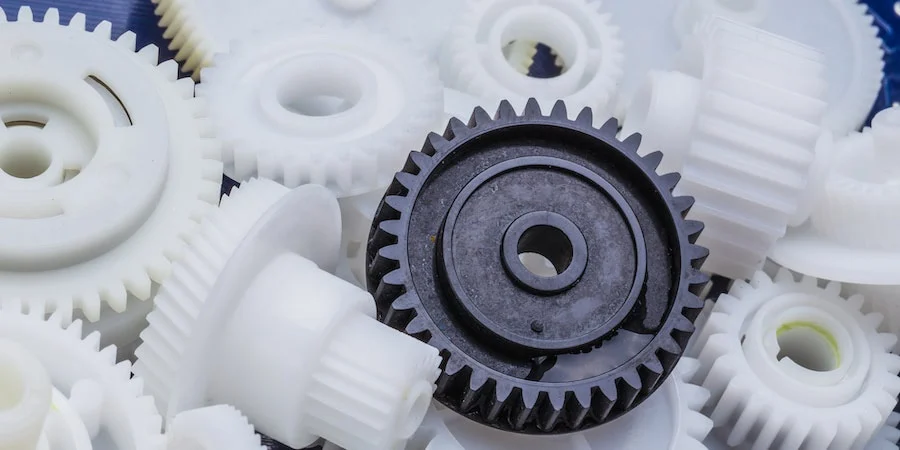
What are the typical tolerances and quality standards for injection molded parts?
When it comes to injection molded parts, the tolerances and quality standards can vary depending on several factors, including the specific application, industry requirements, and the capabilities of the injection molding process. Here are some general considerations regarding tolerances and quality standards:
Tolerances:
The tolerances for injection molded parts typically refer to the allowable deviation from the intended design dimensions. These tolerances are influenced by various factors, including the part geometry, material properties, mold design, and process capabilities. It’s important to note that achieving tighter tolerances often requires more precise tooling, tighter process control, and additional post-processing steps. Here are some common types of tolerances found in injection molding:
1. Dimensional Tolerances:
Dimensional tolerances define the acceptable range of variation for linear dimensions, such as length, width, height, and diameter. The specific tolerances depend on the part’s critical dimensions and functional requirements. Typical dimensional tolerances for injection molded parts can range from +/- 0.05 mm to +/- 0.5 mm or even tighter, depending on the complexity of the part and the process capabilities.
2. Geometric Tolerances:
Geometric tolerances specify the allowable variation in shape, form, and orientation of features on the part. These tolerances are often expressed using symbols and control the relationships between various geometric elements. Common geometric tolerances include flatness, straightness, circularity, concentricity, perpendicularity, and angularity. The specific geometric tolerances depend on the part’s design requirements and the manufacturing capabilities.
3. Surface Finish Tolerances:
Surface finish tolerances define the acceptable variation in the texture, roughness, and appearance of the part’s surfaces. The surface finish requirements are typically specified using roughness parameters, such as Ra (arithmetical average roughness) or Rz (maximum height of the roughness profile). The specific surface finish tolerances depend on the part’s aesthetic requirements, functional needs, and the material being used.
Quality Standards:
In addition to tolerances, injection molded parts are subject to various quality standards that ensure their performance, reliability, and consistency. These standards may be industry-specific or based on international standards organizations. Here are some commonly referenced quality standards for injection molded parts:
1. ISO 9001:
The ISO 9001 standard is a widely recognized quality management system that establishes criteria for the overall quality control and management of an organization. Injection molding companies often seek ISO 9001 certification to demonstrate their commitment to quality and adherence to standardized processes for design, production, and customer satisfaction.
2. ISO 13485:
ISO 13485 is a specific quality management system standard for medical devices. Injection molded parts used in the medical industry must adhere to this standard to ensure they meet the stringent quality requirements for safety, efficacy, and regulatory compliance.
3. Automotive Industry Standards:
The automotive industry has its own set of quality standards, such as ISO/TS 16949 (now IATF 16949), which focuses on the quality management system for automotive suppliers. These standards encompass requirements for product design, development, production, installation, and servicing, ensuring the quality and reliability of injection molded parts used in automobiles.
4. Industry-Specific Standards:
Various industries may have specific quality standards or guidelines that pertain to injection molded parts. For example, the aerospace industry may reference standards like AS9100, while the electronics industry may adhere to standards such as IPC-A-610 for acceptability of electronic assemblies.
It’s important to note that the specific tolerances and quality standards for injection molded parts can vary significantly depending on the application and industry requirements. Design engineers and manufacturers work together to define the appropriate tolerances and quality standards based on the functional requirements, cost considerations, and the capabilities of the injection molding process.
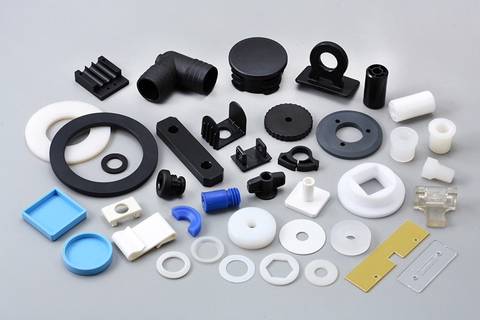
Can you describe the various post-molding processes, such as assembly or secondary operations, for injection molded parts?
Post-molding processes play a crucial role in the production of injection molded parts. These processes include assembly and secondary operations that are performed after the initial molding stage. Here’s a detailed explanation of the various post-molding processes for injection molded parts:
1. Assembly:
Assembly involves joining multiple injection molded parts together to create a finished product or sub-assembly. The assembly process can include various techniques such as mechanical fastening (screws, clips, or snaps), adhesive bonding, ultrasonic welding, heat staking, or solvent welding. Assembly ensures that the individual molded parts are securely combined to achieve the desired functionality and structural integrity of the final product.
2. Surface Finishing:
Surface finishing processes are performed to enhance the appearance, texture, and functionality of injection molded parts. Common surface finishing techniques include painting, printing (such as pad printing or screen printing), hot stamping, laser etching, or applying specialized coatings. These processes can add decorative features, branding elements, or improve the surface properties of the parts, such as scratch resistance or UV protection.
3. Machining or Trimming:
In some cases, injection molded parts may require additional machining or trimming to achieve the desired final dimensions or remove excess material. This can involve processes such as CNC milling, drilling, reaming, or turning. Machining or trimming is often necessary when tight tolerances, specific geometries, or critical functional features cannot be achieved solely through the injection molding process.
4. Welding or Joining:
Welding or joining processes are used to fuse or bond injection molded parts together. Common welding techniques for plastic parts include ultrasonic welding, hot plate welding, vibration welding, or laser welding. These processes create strong and reliable joints between the molded parts, ensuring structural integrity and functionality in the final product.
5. Insertion of Inserts:
Insertion involves placing metal or plastic inserts into the mold cavity before the injection molding process. These inserts can provide additional strength, reinforce threaded connections, or serve as mounting points for other components. Inserts can be placed manually or using automated equipment, and they become permanently embedded in the molded parts during the molding process.
6. Overmolding or Two-Shot Molding:
Overmolding or two-shot molding processes allow for the creation of injection molded parts with multiple layers or materials. In overmolding, a second material is molded over a pre-existing substrate, providing enhanced functionality, aesthetics, or grip. Two-shot molding involves injecting two different materials into different sections of the mold to create a single part with multiple colors or materials. These processes enable the integration of multiple materials or components into a single injection molded part.
7. Deflashing or Deburring:
Deflashing or deburring processes involve removing excess flash or burrs that may be present on the molded parts after the injection molding process. Flash refers to the excess material that extends beyond the parting line of the mold, while burrs are small protrusions or rough edges caused by the mold features. Deflashing or deburring ensures that the molded parts have smooth edges and surfaces, improving their appearance, functionality, and safety.
8. Inspection and Quality Control:
Inspection and quality control processes are performed to ensure that the injection molded parts meet the required specifications and quality standards. This can involve visual inspection, dimensional measurement, functional testing, or other specialized testing methods. Inspection and quality control processes help identify any defects, inconsistencies, or deviations that may require rework or rejection of the parts, ensuring that only high-quality parts are used in the final product or assembly.
9. Packaging and Labeling:
Once the post-molding processes are complete, the injection molded parts are typically packaged and labeled for storage, transportation, or distribution. Packaging can include individual part packaging, bulk packaging, or custom packaging based on specific requirements. Labeling may involve adding product identification, barcodes, or instructions for proper handling or usage.
These post-molding processes are vital in achieving the desired functionality, appearance, and quality of injection molded parts. They enable the integration of multiple components, surface finishing, dimensional accuracy, and assembly of the final products or sub-assemblies.
كيف تتم مقارنة الأجزاء المصنعة بالحقن مع طرق التصنيع الأخرى من حيث التكلفة والكفاءة؟
تتميز الأجزاء المصنعة بالحقن بمزايا واضحة مقارنةً بأساليب التصنيع الأخرى من حيث التكلفة والكفاءة. توفر عملية الحقن كفاءة عالية وفعالية من حيث التكلفة، خاصةً في الإنتاج على نطاق واسع. إليكم شرح مفصل لكيفية مقارنة الأجزاء المصنعة بالحقن بأساليب التصنيع الأخرى:
مقارنة التكاليف:
يمكن أن يكون قولبة الحقن فعالة من حيث التكلفة مقارنة بطرق التصنيع الأخرى لعدة أسباب:
1. تكاليف الأدوات:
تتطلب عملية التشكيل بالحقن استثمارًا أوليًا في صناعة القوالب، وهو ما قد يكون مكلفًا. مع ذلك، بمجرد تصنيع القوالب، يمكن استخدامها مرارًا وتكرارًا لإنتاج عدد كبير من القطع، مما يؤدي إلى انخفاض تكلفة الوحدة. كما أن انخفاض تكاليف الأدوات يجعل التشكيل بالحقن أكثر فعالية من حيث التكلفة لعمليات الإنتاج بكميات كبيرة.
2. كفاءة استخدام المواد:
تتميز عملية التشكيل بالحقن بكفاءة عالية في استخدام المواد. فهي تتيح التحكم الدقيق في كمية المواد المحقونة في القالب، مما يقلل الهدر إلى أدنى حد. إضافةً إلى ذلك، يمكن إعادة تدوير المواد الزائدة الناتجة عن عملية التشكيل وإعادة استخدامها، مما يقلل تكاليف المواد بشكل أكبر مقارنةً بالطرق التي تُنتج كميات أكبر من النفايات.
3. تكاليف العمالة:
يُعدّ قولبة الحقن عملية آلية للغاية، تتطلب الحد الأدنى من العمالة مقارنةً بأساليب التصنيع الأخرى. فبمجرد تجهيز القوالب وتحديد معايير العملية، يمكن لآلة قولبة الحقن العمل بشكل متواصل، منتجةً الأجزاء بأقل قدر من التدخل البشري. هذه الأتمتة تُقلل تكاليف العمالة وتزيد الكفاءة الإجمالية.
مقارنة الكفاءة:
توفر الأجزاء المصبوبة بالحقن العديد من المزايا من حيث الكفاءة:
1. دورة إنتاج سريعة:
يُعدّ قولبة الحقن عملية تصنيع سريعة، قادرة على إنتاج الأجزاء في دورة زمنية قصيرة نسبيًا. وتعتمد مدة الدورة على عوامل مثل تعقيد الجزء، وخصائص المادة، ووقت التبريد. ومع ذلك، بالمقارنة مع طرق أخرى كالتصنيع الآلي أو الصب، تُمكّن قولبة الحقن من إنتاج أجزاء متعددة في وقت واحد في كل دورة، مما يؤدي إلى معدلات إنتاج أعلى وكفاءة مُحسّنة.
2. دقة عالية واتساق:
تُمكّن عملية التشكيل بالحقن من إنتاج أجزاء بدقة عالية واتساق تام. صُممت القوالب المستخدمة في هذه العملية لتوفير تحكم دقيق ومتكرر في الأبعاد. تضمن هذه الدقة أن كل جزء يفي بالمواصفات المطلوبة، مما يقلل الحاجة إلى عمليات تشغيل أو معالجة لاحقة إضافية. كما أن القدرة على إنتاج أجزاء دقيقة باستمرار تُعزز الكفاءة وتُقلل الوقت والتكاليف المرتبطة بإعادة العمل أو الأجزاء المرفوضة.
3. قابلية التوسع:
تتميز عملية التشكيل بالحقن بقابليتها العالية للتوسع، مما يجعلها مناسبة للإنتاج بكميات صغيرة وكبيرة على حد سواء. وبمجرد تصنيع القوالب، يمكن تكرار عملية التشكيل بالحقن بسهولة، مما يسمح بإنتاج أجزاء متطابقة بكفاءة عالية. إن القدرة على توسيع نطاق الإنتاج بسرعة وكفاءة تجعل التشكيل بالحقن طريقة مفضلة لتلبية متطلبات السوق المتغيرة.
4. تعقيد التصميم:
تدعم عملية التشكيل بالحقن إنتاج أجزاء ذات أشكال هندسية معقدة وتفاصيل دقيقة. يمكن تصميم القوالب لتناسب التجاويف السفلية والجدران الرقيقة والأشكال المعقدة التي قد يصعب أو يكلف تصنيعها باستخدام طرق أخرى. تتيح هذه المرونة في التصميم دمج مكونات متعددة في جزء واحد، مما يقلل من متطلبات التجميع ونقاط الضعف المحتملة. كما أن القدرة على إنتاج تصاميم معقدة بكفاءة تعزز الكفاءة العامة والأداء الوظيفي.
5. تنوع المواد:
تدعم عملية التشكيل بالحقن مجموعة واسعة من المواد البلاستيكية الحرارية، مما يوفر مرونة في اختيار المواد بناءً على الخصائص المطلوبة للجزء النهائي. يمكن اختيار مواد مختلفة لتحقيق خصائص محددة مثل المتانة، والمرونة، ومقاومة الحرارة، ومقاومة المواد الكيميائية، أو الشفافية. تتيح هذه المرونة في اختيار المواد إمكانية تخصيص الجزء وتحسين أدائه بكفاءة عالية.
باختصار، تُعدّ الأجزاء المصنّعة بتقنية الحقن فعّالة من حيث التكلفة والكفاءة مقارنةً بالعديد من طرق التصنيع الأخرى. إذ تُعوّض تكاليف الأدوات الأولية بفضل القدرة على إنتاج كميات كبيرة من الأجزاء بتكلفة أقل للوحدة. وتساهم كفاءة استخدام المواد، وأتمتة العمل، وسرعة دورة الإنتاج، والدقة العالية، وقابلية التوسع، وتعقيد التصميم، وتنوّع المواد في فعالية وكفاءة عملية الحقن من حيث التكلفة. هذه المزايا تجعل من الحقن خيارًا مفضلًا للعديد من الصناعات التي تسعى إلى إنتاج أجزاء عالية الجودة بكفاءة واقتصادية.
<img src="https://img.hzpt.com/img/Injectionmoldedparts/Injectionmoldedparts-L1.webp" alt="China Professional Injection Molded Plastic Part in Customized Size for Manufacturing Requirements “><img src="https://img.hzpt.com/img/Injectionmoldedparts/Injectionmoldedparts-L2.webp" alt="China Professional Injection Molded Plastic Part in Customized Size for Manufacturing Requirements “>
editor by Dream 2024-10-25

























